
3-Axis CNC Machining Services
Precision 3-axis CNC machining for custom metal and plastic parts with accessible surfaces, pockets, slots, holes, and external profiles. Designed for tight tolerances, stable quality, and cost efficiency, this process is ideal for prototypes and low-to-medium volume production, delivering reliable results for functional components with straightforward geometries.
3-Axis CNC Milling Capabilities and Specifications
| Item | Specification |
|---|---|
| Machining Processes | Face milling, pocket milling, slot milling, profile milling, drilling, boring, reaming, tapping, chamfering, and engraving |
| Maximum Part Size | Up to 1200 × 700 × 500 mm |
| Part Types | Plates, brackets, housings, covers, fixture blocks, tooling components, panels, and machine bases |
| Materials | Aluminum, stainless steel, carbon steel, alloy steel, brass, copper, titanium, and engineering plastics |
| Tolerance | ±0.025 mm; down to ±0.01 mm for selected critical features after drawing and process |
| Machining Features | Flat surfaces, pockets, slots, holes, threads, steps, chamfers |
| Surface Roughness | Typically Ra 0.8–3.2 μm for as-machined surfaces |
| Inspection | First article inspection, dimensional checks, thread gauges, pin gauges, height gauges, and CMM inspection |
| Production Support | One-off prototypes, low-volume production, and repeat manufacturing |
| Supported Files | STEP, STP, IGES, X_T, SLDPRT, DWG, DXF, and PDF |
| Prototype Lead Time | Typically 3–7 business days |
| Production Lead Time | Typically 10–20 business days, depending on quantity, complexity, and finishing |

Custom Parts Best Suited for 3-Axis CNC Machining

Mounting Brackets

Fixture Blocks

CNC Machined Enclosures
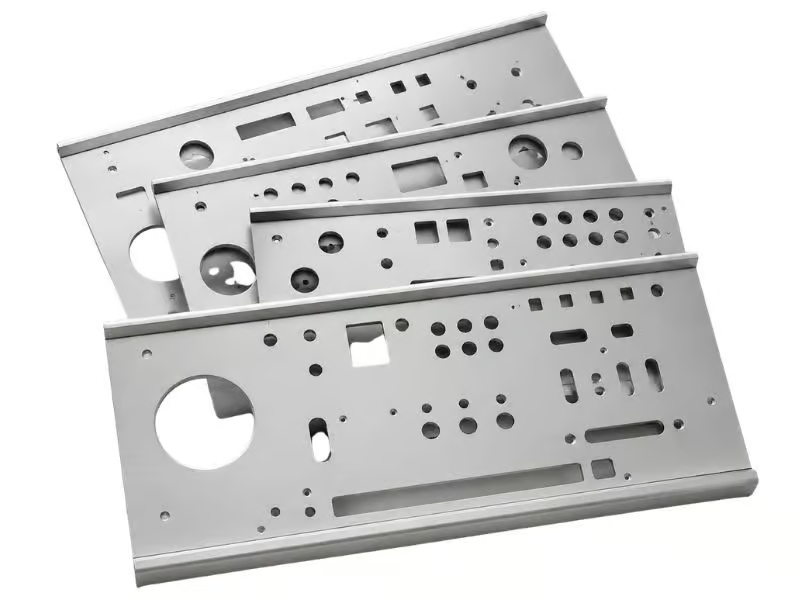
Front Panels

Machined Heat Sinks

Custom Flanges
Reliable 3-Axis CNC Machining Solutions from DZ Making
Key Engineering Considerations for 3-Axis CNC Machining
For each custom part produced on a CNC 3 axis mill, DZ Making reviews tool accessibility, machining direction, datum selection, setup sequence, and tolerance relationships before programming. This engineering review helps reduce unnecessary repositioning, improve dimensional consistency, and confirm whether 3-axis CNC machining provides the most efficient and cost-effective production method.
Tool Access from Fixed Machining Directions
In 3-axis CNC machining, the cutter moves along the X, Y, and Z axes while the tool angle remains fixed. We review pocket depth, internal corner radius, side features, and cutter clearance to keep critical surfaces accessible. Where possible, we limit tool overhang to approximately four times the cutter diameter to reduce vibration, deflection, and poor surface finish.
Workpiece Repositioning and Datum Control
Multi-sided 3-axis machined parts require manual repositioning because the machine does not automatically rotate the workpiece. We select stable datum faces, plan practical clamping areas, and machine related holes, pockets, and assembly surfaces in the same setup. This approach reduces alignment variation and improves flatness, parallelism, and hole-position consistency.
Tight Tolerances Across Multiple Setups
Cross-setup dimensions in 3-axis CNC machining are typically controlled within ±0.02–0.05 mm, while requirements tighter than ±0.02 mm need additional process review. DZ Making confirms tolerance feasibility before production and uses precision fixturing, in-process probing, and CMM inspection for critical feature relationships.
3-Axis CNC Machining Operations We Support
At DZ Making, our 3-axis CNC machining operations include face milling, pocket milling, slot milling, drilling, tapping, boring, reaming, profile cutting, chamfering, and engraving. We select the appropriate cutting tools, machining sequence, and inspection methods based on your part geometry, material, tolerance, and functional requirements. This allows us to produce accurate, consistent, and assembly-ready components for prototypes, low-volume orders, and repeat production.


Cost-Effective Machining for Accessible Geometries
3-axis CNC machining provides a cost-effective solution for custom parts with accessible flat faces, pockets, slots, holes, threads, and external profiles. Direct tool access and established machining methods reduce programming complexity, setup preparation, and machine-hour costs compared with multi-axis machining.
For suitable parts, DZ Making can use standard tooling, reusable CAM programs, and multi-part fixtures to improve production efficiency. This makes 3-axis machining practical for prototypes, low-volume orders, and repeat production without adding unnecessary multi-axis costs.


Stable Accuracy and Repeatability
Precision 3-axis CNC machining provides stable cutting conditions for prismatic parts that rely on flat datums, accurate hole positions, controlled pocket depths, and consistent assembly surfaces. Our team plans the datum structure, clamping method, and machining sequence before production to control dimensional relationships across each setup.
Standardized fixtures, cutting parameters, inspection methods, and approved CAM programs help maintain consistent results across multiple parts and repeat orders. This process supports reliable flatness, parallelism, feature position, and assembly fit for functional components.
Faster Setup and Production Turnaround
3-axis CNC machining uses mature programming, tooling, and workholding methods, which can shorten process preparation and first-article production for suitable parts. Direct toolpaths and standard machining operations also simplify in-process inspection and reduce unnecessary production variables.
DZ Making retains approved programs, fixture information, tool data, and inspection requirements for repeat orders. This allows us to restart production efficiently, maintain consistent quality, and support shorter lead times for recurring brackets, housings, fixture blocks, front panels, heat sinks, and custom flanges.

What International Customers Say About DZ Making?
International engineers and manufacturing teams rely on DZ Making for consistent 3-axis CNC machining services that meet functional requirements, quality standards, and delivery expectations.
The 3-axis CNC machining work from DZ Making matched our drawings and tolerance requirements precisely. Early feedback helped us resolve design details before production.

We received multiple 3-axis CNC machined parts from DZ Making, and the dimensional consistency across batches was very stable. Parts arrived ready for assembly.

Their understanding of functional requirements stood out. DZ Making delivered 3-axis CNC machining results that met our application needs without repeated clarification.

Applications of 3-Axis CNC Machining
3-axis CNC machining is commonly applied across multiple industries where dimensional accuracy, structural reliability, and cost-effective production are essential for functional and precision-engineered components.
01
02
03
FAQs
What tolerances can be achieved with 3-axis CNC machining?
3-axis CNC machining typically holds tolerances around ±0.025 mm. For critical dimensions, DZ Making can tighten this to ±0.01 mm after reviewing the material, part geometry, tool access, and setup strategy. We confirm the achievable tolerance before production and match the inspection method to the drawing requirements.
3-axis CNC machining services are suitable for both prototyping and low- to medium-volume production. The process offers stable repeatability and cost efficiency, making it practical for parts beyond one-off prototypes.
A 3-axis CNC machining service is ideal for parts with straightforward geometries, flat surfaces, pockets, and standard hole features. It is commonly used for brackets, plates, housings, and structural components that do not require multi-angle machining.
A 3-axis CNC machining service is generally more cost-effective and faster for simple to moderate geometries. When parts do not require complex angles or undercuts, 3-axis machining often provides the best balance of accuracy, lead time, and cost.
Yes, many parts can be completed in a single setup using 3-axis CNC machining, including milling, drilling, and threading features. This helps reduce repositioning errors and improves overall dimensional consistency.
What Is 3-Axis CNC Machining?
3-axis CNC machining is a widely used subtractive manufacturing process in which cutting tools move along the X, Y, and Z axes to remove material from a fixed workpiece. It is commonly applied to produce custom CNC machined parts with flat surfaces, pockets, slots, contours, and precisely located holes.
A 3-axis CNC milling is well-suited for parts with straightforward geometries that do not require tool or workpiece rotation during machining. Because the setup remains stable throughout the process, this method delivers reliable accuracy, repeatability, and cost efficiency for prototyping and low-to-medium volume production.
Surface Finishes for 3-Axis CNC Machined Parts
Surface finish affects the appearance, corrosion resistance, wear performance, and assembly fit of 3-axis CNC machined parts. Material type, operating environment, cosmetic requirements, and dimensional tolerances all influence the appropriate finishing method.
DZ Making plans for surface treatment together with the 3-axis CNC machining process. We review coating thickness, masking areas, sealing faces, threaded holes, and precision fits before production to protect critical dimensions and reduce secondary rework.
Common surface finishing options include:
- As-machined: Retains visible cutting marks and commonly achieves a surface roughness of approximately Ra 1.6–3.2 μm, depending on the material, tooling, and cutting parameters.
- Bead blasting: Creates a uniform matte surface and reduces visible machining marks on aluminum and stainless steel parts.
- Anodizing: Improves corrosion resistance, surface hardness, and appearance for aluminum parts. The coating thickness must be considered for threaded holes and precision fits.
- Passivation: Removes free iron from stainless steel surfaces and improves corrosion resistance without adding a thick dimensional coating.
- Powder coating: Adds a durable protective and decorative layer to brackets, housings, panels, and other external components.
- Polishing: Produces a smoother or more reflective surface for visible components, sealing areas, and parts requiring reduced surface friction.
3-Axis CNC Machining Compared with 5-Axis Machining
The primary difference between 3-axis and 5-axis CNC machining lies in tool orientation and workpiece movement. A CNC 3 axis mill moves along the X, Y, and Z axes while keeping the tool angle fixed. A 5-axis machine adds two rotary axes, allowing the cutting tool or workpiece to approach features from multiple angles.
Precision 3-axis CNC machining suits parts with accessible flat faces, pockets, holes, slots, and external profiles. It generally requires simpler programming, less complex workholding, and lower machine-hour costs. For brackets, panels, fixture blocks, housings, heat sinks, and similar prismatic parts, 3-axis milling often provides the more efficient production method.
5-axis machining becomes more suitable when a part includes compound angles, deep side features, undercuts, complex curved surfaces, or critical features distributed across several orientations. It can reduce manual repositioning and complete complex geometry in fewer setups, but its additional capability also increases programming and machining costs.
