
4-Axis CNC Machining Services
DZ Making provides 4-axis CNC machining services for custom parts with multi-sided, radial, and rotary features. We machine metals and engineering plastics from prototypes to repeat production, helping reduce manual setups while maintaining consistent feature positioning across complex component geometries.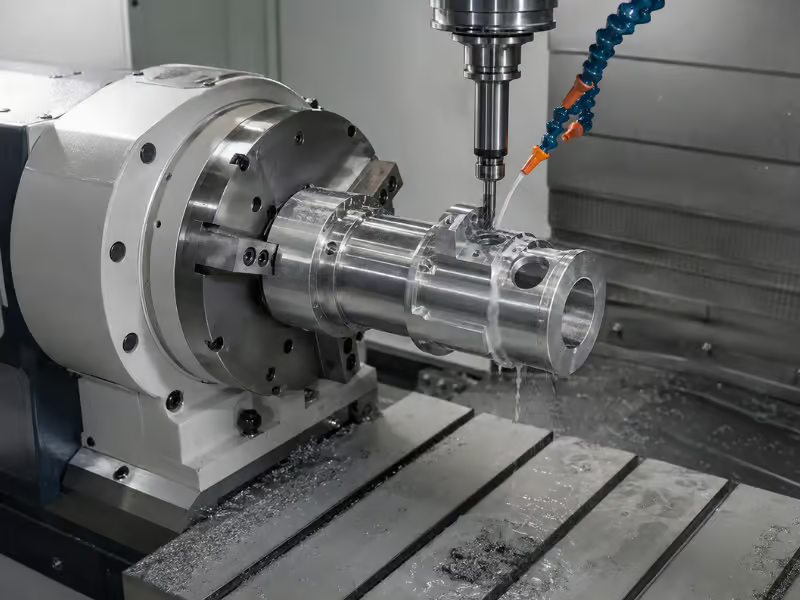
4-Axis Machining Capabilities
| Capability | Specification |
|---|---|
| Machining processes | Milling, drilling, boring, reaming, tapping, slotting |
| 4-axis modes | Indexed and continuous |
| Rotary axis travel | 360° continuous |
| Max. rotary diameter | Ø300 mm |
| Max. workpiece length | 600 mm |
| Rotary positioning accuracy | ±15 arc sec |
| Materials | Metals and engineering plastics |
| Typical tolerance | ±0.02–0.05 mm |
| Tight tolerance | Down to ±0.01 mm |
| Surface roughness | Ra 0.8–3.2 μm |
| Production volume | Prototype to repeat production |
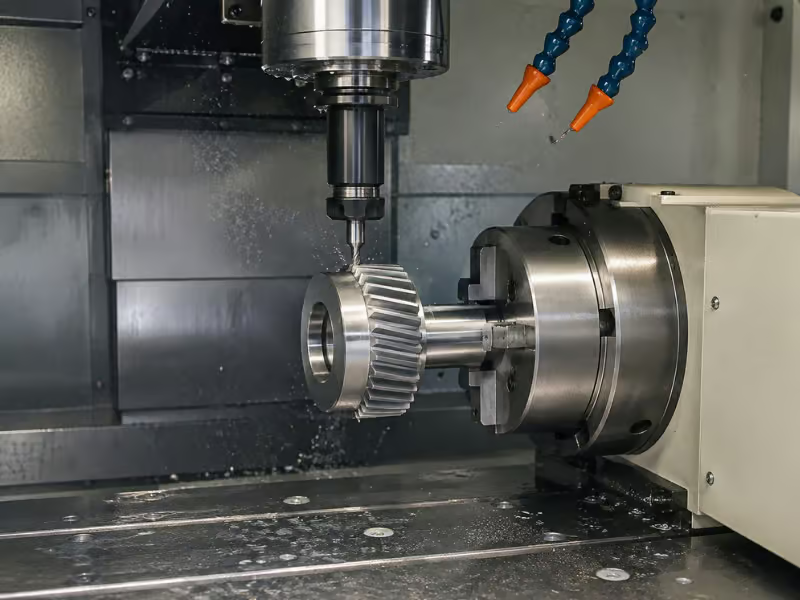
Parts Commonly Suited to 4-Axis Machining

Shafts and Sleeves
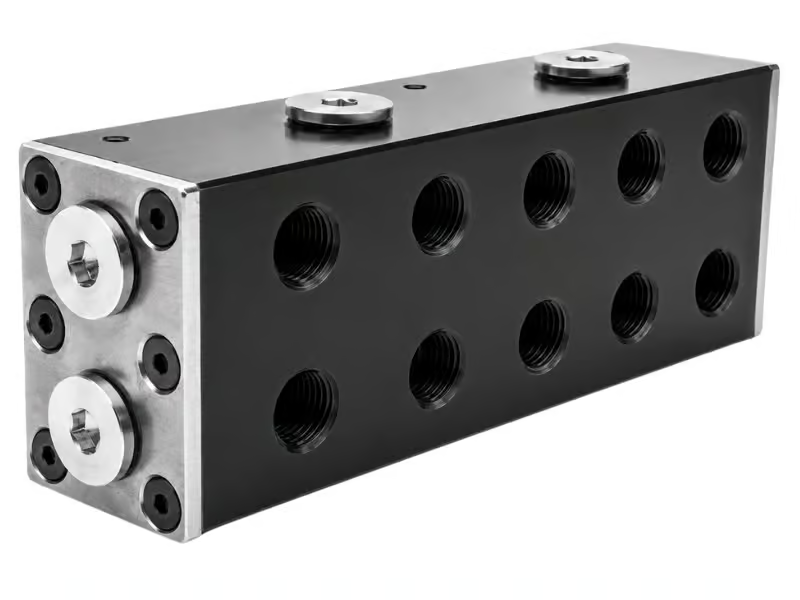
Multi-Port Valve Bodies

Camshafts and Cam Components

Helical Groove Parts
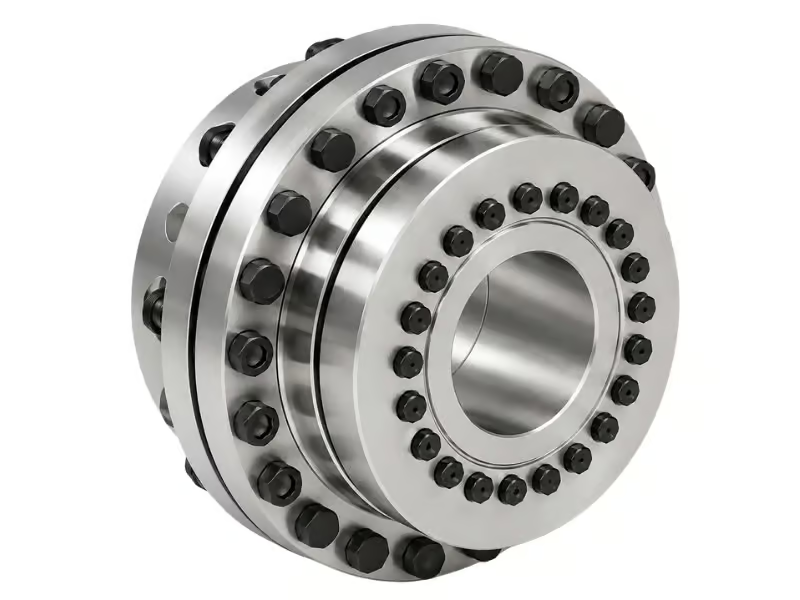
Flanges and Couplings
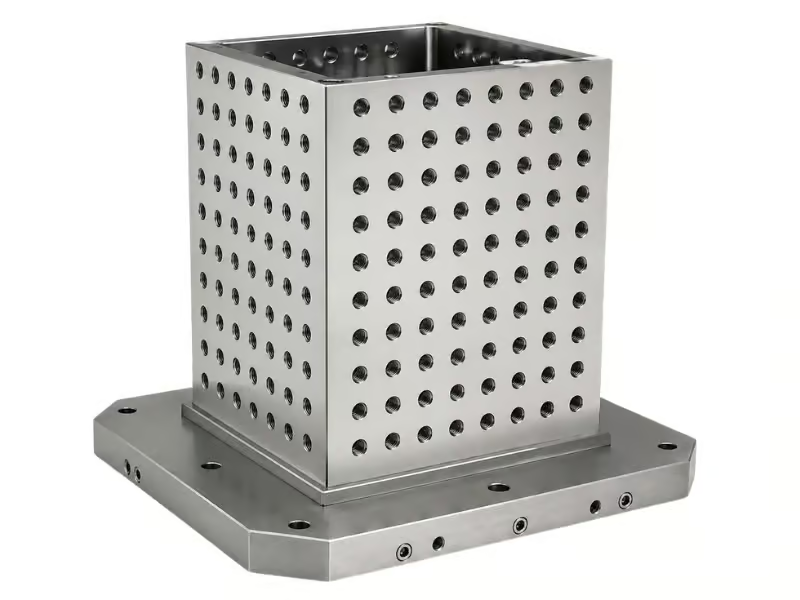
Multi-Sided Housings and Fixtures
Not Sure Whether Your Part Needs 4-Axis Machining?
Why Use 4-Axis Machining?
4-axis CNC milling can reduce setup changes, maintain more consistent relationships between features on different sides, and handle rotary geometry more efficiently when features are arranged around a common axis.
Fewer Manual Setups
Submit your drawings or CAD files for review. Specifications, tolerances, and material requirements are evaluated to provide clear feedback and an accurate, manufacturable quotation.
Better Cross-Side Consistency
These Parts are machined using stable 3-axis CNC processes with controlled parameters. In-process checks and final inspection ensure dimensional accuracy and consistent part quality.
More Efficient Rotary Machining
Required surface finishing, deburring, and final checks are completed before secure packaging and shipment. Parts are delivered ready for assembly or further processing.
4-Axis Machining Across Different Production Needs
As an experienced 4-axis CNC machining manufacturer, we support prototypes, low-volume orders, and repeat production for custom OEM components. Flexible setups accommodate design changes in early-stage projects, while proven programs, fixtures, tooling, and inspection methods help maintain consistency across recurring production runs.


Feature Orientation and Tool Access
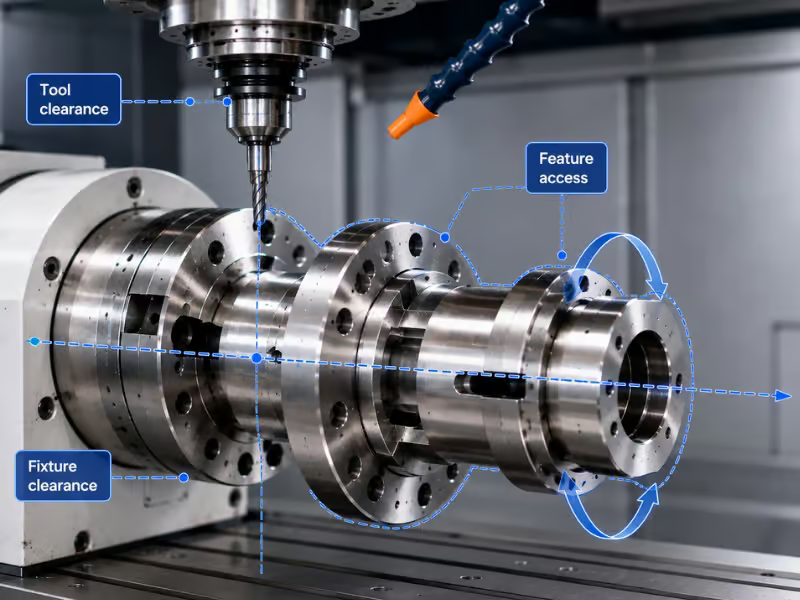
The position of each feature relative to the rotary axis determines whether the cutter can reach it at a stable and practical angle. Deep recesses, shoulders, diameter transitions, and chuck-side features can restrict access even after the workpiece rotates into position. Tool reach, holder clearance, rotational envelope, and fixture interference must therefore be considered together to avoid excessive tool overhang, unstable cutting, or unnecessary secondary setups.
Before programming, we review feature orientation against the planned rotary positions and workholding layout. This helps identify access risks early and determine whether the part can remain in one 4-axis setup or needs a revised fixture, tool approach, or secondary operation.
Workholding and Datum Control
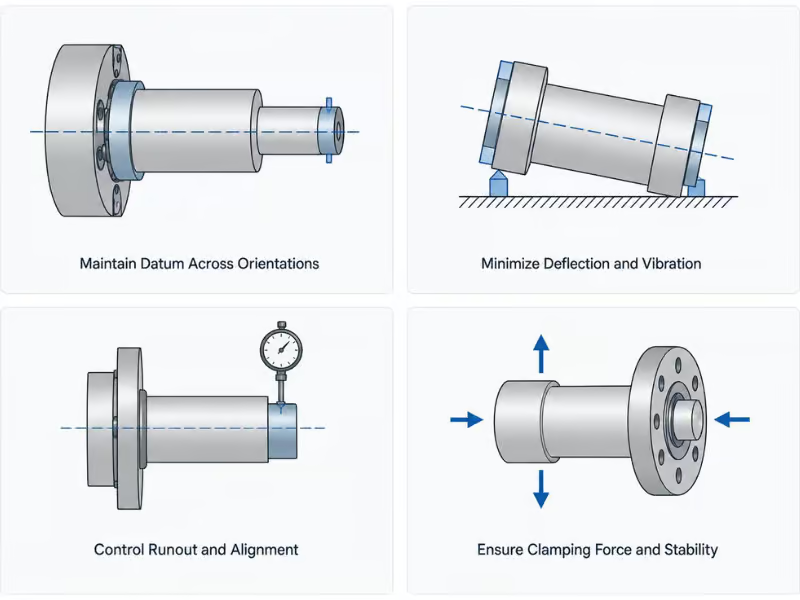
4-axis workholding must secure the part without restricting the orientations needed for machining. Chucks, collets, mandrels, tailstock support, fixture plates, or fixtures may be used depending on part geometry, cutting load, and required access. The datum relationship must remain controlled through each indexed position so features machined at different angles maintain their intended positional relationship.
For long, slender, thin-wall, or asymmetric parts, we evaluate clamping force, support position, deflection, and runout before machining. We plan the fixture and datum strategy together so each CNC component remains stable while preserving access to the required machining orientations.
Tolerance and Rotary Positioning
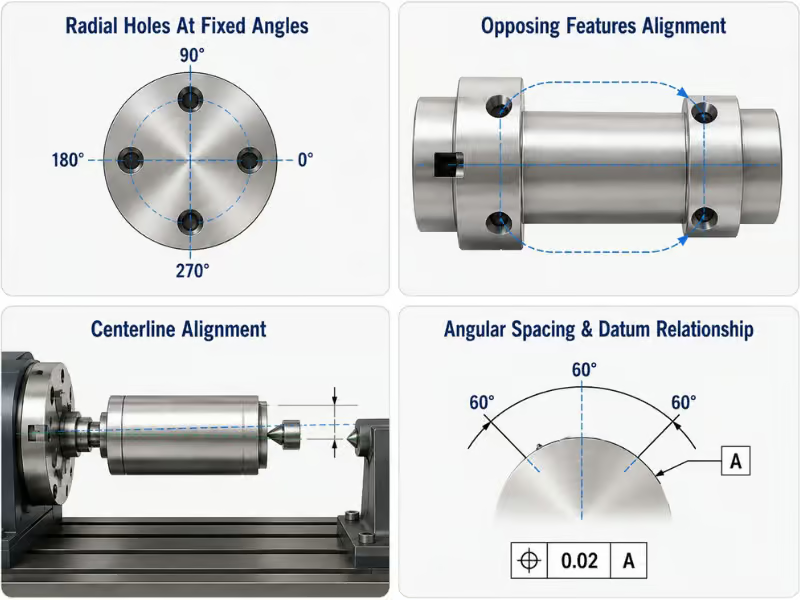
4-axis accuracy depends on both linear-axis control and how precisely the workpiece is positioned around the established rotary centerline. A rotary positioning capability of ±15 arc sec supports accurate angular indexing, while workpiece alignment, fixture accuracy, centerline offset, and cutting conditions still influence the final feature relationship.
When a drawing includes radial holes at fixed angles, opposing features that must align, or bolt patterns referenced to the same centerline, we evaluate their angular position, spacing, runout, and datum relationship together. This helps establish the rotary zero, maintain workpiece alignment, and limit accumulated positioning error as the part indexes from one machining angle to the next.
What Customers Say About Our 4-Axis Machining Services?
Customers typically use our 4-axis CNC machining services for parts with multi-side, radial, or rotary features that need reliable positioning across different orientations. Their feedback often centers on fit, consistency, and how smoothly the parts move from prototype to repeat production.
Our drive shafts required radial cross holes, wrench flats, and keyway features around the diameter. DZ Making used a 4-axis CNC mill to machine the different orientations, and the finished shafts matched the positional requirements on our drawings.

We ordered 316 stainless steel hydraulic valve bodies with four threaded ports positioned around the body, so angular accuracy was important for assembly. DZ Making handled the 4-axis machining well, and the parts fitted our manifold system without additional rework.

We started with a small batch of aluminum housing prototypes before moving into repeat production. The 4-axis CNC milling process worked well for the side features, and the dimensions stayed consistent when we reordered from DZ Making.

Different Ways the 4-Axis Is Used in Machining
A 4-axis CNC machine can use the rotary axis in different ways depending on the part geometry and the feature being machined. The main approaches include fixed-angle indexing, wrapped toolpaths around cylindrical surfaces, and continuous rotary motion coordinated with the linear axes.
01
02
03
FAQs
What is 4-axis CNC machining?
4-axis CNC machining adds a programmable rotary axis to the X, Y, and Z linear axes. This allows the workpiece to rotate between fixed angles or move continuously during cutting, making it suitable for multi-side, radial, circumferential, and helical features.
Tolerance capability depends on part geometry, material, feature relationships, workholding, and inspection requirements. Typical machining tolerances are around ±0.02–0.05 mm, with tighter tolerances possible for suitable features and controlled setups.
Provide a 3D CAD model, 2D drawing, material grade, quantity, tolerances, surface finish, and any inspection requirements. These details help determine the machining method, workholding approach, production time, and quotation.
Yes. A 4-axis CNC mill can index the workpiece to defined angles for radial holes, threaded ports, flats, slots, and other features positioned around a common axis.
Inspection may include CMM measurement, gauges, height measurement, or other methods depending on the drawing. Particular attention is given to angular spacing, true position, runout, and relationships between features machined at different orientations.
Yes, when the machine and CAM strategy support continuous rotary motion. Coordinated movement between the rotary axis and the X, Y, and Z axes allows helical grooves, spiral profiles, and similar continuous features to be machined around the workpiece.
What Is the Structure of a 4-Axis CNC Machine?
A 4-axis CNC machine builds on the X, Y, and Z motion of a conventional CNC mill by adding a programmable rotary axis, typically the A- or B-axis. This rotary system works with the machine’s linear motion, spindle, workholding, and CNC control to position or rotate the workpiece during machining.
- X, Y, and Z linear axes: Control movement along the three primary directions for milling, drilling, slotting, and other cutting operations.
- Rotary axis: Rotates the workpiece around a defined centerline for fixed-angle indexing or continuous 4-axis machining.
- Rotary table or indexer: Provides controlled angular positioning and supports the workholding system during rotation.
- Spindle and cutting tools: Perform material removal while the workpiece remains fixed at an indexed angle or rotates along a coordinated toolpath.
- Workholding system: Uses chucks, collets, mandrels, fixture plates, or other setups to locate and secure the part relative to the rotary centerline.
- CNC control system: Coordinates the linear and rotary axes according to the programmed toolpath, including simultaneous motion when the geometry requires it.
How Does Part Length Affect 4-Axis Machining Stability?
Longer workpieces are more sensitive to deflection, vibration, and support conditions during 4-axis machining. As the cutting point moves farther from the main clamping area, rigidity can decrease, making it harder to maintain stable cutting and consistent feature positioning around the rotary axis.
- Overhang and deflection: Greater unsupported length increases bending under cutting force, which can affect dimensions, surface finish, and feature consistency.
- Reduced rotational stability: Longer parts are more prone to vibration, runout, and movement during indexing or continuous rotation, making angular and cross-side features harder to hold consistently.
- Greater error amplification: Small alignment, support, or centerline errors can produce larger positional differences over a longer workpiece, especially between features located far apart along the same rotary axis.
3-Axis vs 4-Axis vs 5-Axis Machining: Which Should You Choose?
The right axis configuration depends on more than part complexity. Tool access, setup count, machining time, programming effort, and total production cost all affect which process is most practical. More axes increase machining flexibility, but they do not automatically make a part faster or cheaper to produce.
3-Axis Machining for Simpler Geometries
3-axis machining is usually the simplest and most economical option when the required features remain accessible from a few straightforward directions. Programming and setup are generally faster than with 4-axis or 5-axis machining, making it efficient for pockets, holes, planar faces, and basic contours. However, once a part requires repeated flipping and re-clamping, the additional setup time can reduce this cost advantage and make cross-side feature relationships harder to maintain.
4-Axis Machining for Rotary and Multi-Side Features
4-axis CNC machining adds one programmable rotary axis, providing a useful middle ground between 3-axis simplicity and 5-axis flexibility. For shafts, valve bodies, flanges, and other parts with radial, circumferential, or multi-side features, programmed rotation can replace several manual setups and shorten the overall machining sequence. Machine and programming requirements are higher than basic 3-axis milling, but the process can be more economical when one rotary axis provides all the access the part needs.
5-Axis Machining for Complex Tool Orientations
5-axis machining provides the greatest tool-access flexibility by adding a second rotary degree of freedom. It can reduce setups for compound angles, deep cavities, complex surfaces, and features that a single rotary axis cannot expose effectively. Machine rates, programming, and setup planning are typically more demanding than 3-axis or 4-axis machining, so using 5-axis for a part that only needs one rotary direction may add cost without providing a meaningful manufacturing advantage.
In practice, choose 3-axis machining when the geometry stays simple, and setup changes remain limited. Move to 4-axis machining when features sit around one main rotary axis and programmed rotation can replace repeated re-clamping. Choose 5-axis machining when the part requires compound tool angles or access that one rotary axis cannot provide.
