
CNC cutting uses computer-controlled movement to remove, shape, or separate material with repeatable precision. However, the term covers several processes, including milling, turning, laser cutting, plasma cutting, waterjet cutting, and wire EDM. Each method suits different part geometries, materials, tolerances, and production needs, so process selection directly affects cost and part quality.
This guide explains what CNC cutting is, how it works, and how the main processes differ. It also covers machines, cutting tools, suitable materials, selection factors, industrial applications, and practical design considerations for custom parts.
What Is CNC Cutting?
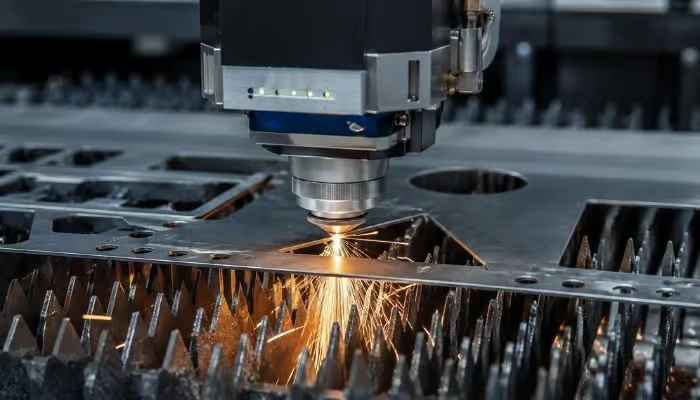
CNC cutting is a computer-controlled process that removes or separates material according to programmed paths. A CNC system controls machine movement, cutting speed, feed, and position based on digital instructions. Depending on the process, CNC cutting may use rotating tools, turning inserts, laser energy, plasma, high-pressure water, or electrical discharge. It can process metals, engineering plastics, and other materials for machined parts that require consistent dimensions and repeatable production.
CNC Cutting vs. CNC Machining: What Is the Difference?
CNC cutting and CNC machining overlap, but they are not identical. CNC cutting focuses on removing or separating material along programmed paths using methods such as milling, turning, laser, waterjet, or EDM. CNC machining covers a broader range of subtractive operations, including drilling, boring, threading, milling, and turning, to create precise features and final part dimensions.
The difference matters when you select a process for a specific design. Laser cutting works well for producing flat profiles from sheet or plate, while CNC machining can create pockets, threads, precision holes, contours, and complex 3D surfaces. In many projects, a part may first undergo a cutting process and then require additional CNC machining to meet its final tolerance and feature requirements.
How Does CNC Cutting Work? Step by Step
CNC cutting follows a digital workflow that turns part geometry into controlled machine movement. The process starts with a CAD model and ends with inspection of the finished part. Each stage affects dimensional accuracy, cutting quality, cycle time, and production consistency.

Step 1: Create the CAD Model
Start with a 2D drawing or 3D CAD model that clearly defines the required geometry and dimensions. Include critical features such as holes, slots, radii, tolerances, and surface requirements when necessary. Accurate design data gives the programming stage a reliable reference and reduces the risk of dimensional or manufacturing errors later.
Step 2: Generate the Toolpath
Import the CAD data into CAM software and generate the path that the machine will follow. Define the cutting sequence, movement direction, entry points, and machining boundaries based on the part geometry. Review the toolpath before production to identify unnecessary movement, possible interference, or areas where the programmed path may not match the design.
Step 3: Set Up the Machine
Prepare the machine, load the required material, install suitable tooling, and secure the workpiece firmly. Set the correct work coordinate system so the machine can match its movements to the programmed geometry. Stable workholding and accurate positioning help prevent movement during cutting and improve consistency from one part to the next.
Step 4: Set Cutting Parameters
Set the cutting parameters according to the material, tooling, part geometry, and required finish. Typical settings control cutting speed, feed rate, depth, and other process conditions. Balanced parameters help maintain dimensional accuracy, stable cutting, acceptable surface quality, and reasonable cycle time without placing unnecessary load on the tool or machine.
Step 5: Run the Cutting Process
Load the verified program and begin the cutting cycle. The CNC system follows the programmed path while controlling machine movement throughout the operation. Monitor the process for unexpected vibration, material movement, tool condition, or cutting instability. Stable conditions allow the same programmed sequence to produce consistent results across repeated production runs.
Step 6: Inspect the Finished Part
Inspect the finished part against the drawing or CAD requirements after cutting. Check critical dimensions, profiles, holes, tolerances, and surface condition with suitable measuring equipment. If any feature falls outside specification, review the setup, program, or process parameters before continuing production to prevent the same issue from affecting additional parts.
Main Types of CNC Cutting Processes
CNC cutting includes several processes that remove or separate material through programmed machine movement. Each method offers different strengths in geometry, material compatibility, dimensional control, edge quality, and production speed. Understanding these differences helps you match the cutting process to the actual requirements of the part.
CNC Milling

CNC milling removes material with rotating cutting tools while the machine controls movement along multiple axes. It can produce flat faces, pockets, slots, holes, bosses, angled surfaces, complex contours, and 3D freeform features. For many machined parts, a general tolerance of around ±0.05 mm is practical, while critical features can reach about ±0.01 mm with suitable equipment, tooling, setup, and inspection.
The process also supports 3-axis, 4-axis, and 5-axis configurations, which allow access to different part surfaces with fewer setups. CNC milling works well for prototypes, low-volume production, and precision components. However, tool diameter limits sharp internal corners, while deep cavities, thin walls, and difficult tool access can increase machining time and complexity.
CNC Turning

In CNC turning, the workpiece spins while a fixed cutting tool removes material from its surface. A CNC lathe follows G-code instructions to control spindle speed, tool position, feed, and cutting sequence. This setup makes the process especially effective for cylindrical, tapered, stepped, grooved, and threaded shapes, including shafts, pins, screws, bushings, and sleeves. For many turned parts, tolerances around ±0.05 mm are practical, while critical diameters can reach about ±0.01 mm under well-controlled machining conditions.
Compared with milling, turning offers less freedom for non-cylindrical geometry, but it performs very well when the part has rotational symmetry. Programmed cycles also make it suitable for repeated production because the machine can reproduce the same diameters and profiles consistently. CNC lathes generally occupy less floor space than large machining centers and can support efficient production of round components.
CNC Routing
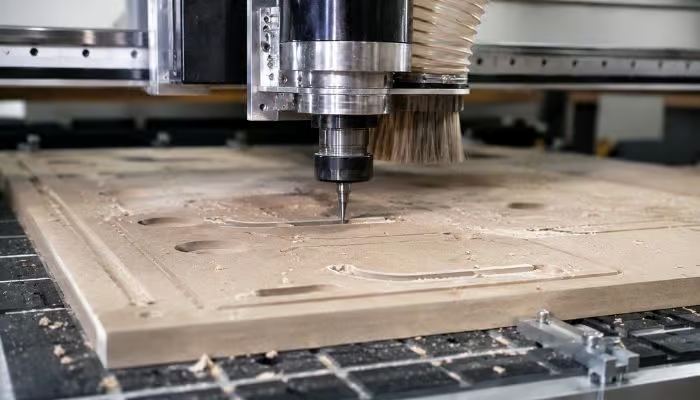
CNC routing uses a high-speed rotating cutter to remove material along programmed paths, but it usually works with lighter machine structures and larger work areas than CNC milling. The process handles plastics, composites, wood, foam, acrylic, and softer metals such as aluminum, making it useful for panels, covers, enclosures, templates, and large flat components.
Its main strength lies in fast cutting over large sheet sizes and relatively simple 2D or 2.5D geometry. CNC routers can produce profiles, pockets, holes, and contours efficiently, but they generally offer lower rigidity than machining centers. For parts that require tight tolerances, deep features, or heavy metal removal, CNC milling usually provides better dimensional control and process stability.
CNC Laser Cutting

CNC laser cutting focuses a high-energy laser beam onto the material while the cutting head follows a programmed path. The concentrated heat melts or vaporizes a narrow section of the workpiece, creating clean 2D profiles, small holes, slots, and detailed contours. It works especially well with sheet metals such as carbon steel, stainless steel, and aluminum.
A narrow kerf and high travel speed make laser cutting effective for thin to medium sheet, especially when parts contain complex outlines or many repeated features. Typical dimensional accuracy can reach around ±0.1 mm in suitable applications, although material type and thickness affect the result. The process also creates a heat-affected zone, so some parts may need secondary finishing or machining afterward.
CNC Plasma Cutting

CNC plasma cutting uses a high-temperature plasma arc to melt and remove electrically conductive metal along a programmed path. It works with carbon steel, stainless steel, aluminum, and other conductive metals, and it is especially suitable for medium to thick plate. Depending on the equipment and material, plasma cutting can handle plate thicknesses from a few millimeters to more than 50 mm.
Its main advantages are fast cutting speed and lower cost for thicker sections compared with many laser applications. However, plasma generally creates a wider kerf, more edge taper, and lower dimensional accuracy than laser cutting. Parts with tight tolerances, precision holes, or critical mating surfaces may still require secondary CNC machining.
CNC Waterjet Cutting

CNC waterjet cutting uses an ultra-high-pressure stream of water, often mixed with garnet abrasive, to erode material along a programmed path. Operating pressure commonly reaches about 60,000–90,000 psi, giving the jet enough energy to cut steel, aluminum, titanium, plastics, composites, glass, and stone without relying on heat.
Because waterjet cutting is a cold-cutting process, it avoids heat-affected zones and thermal distortion. This makes it suitable for heat-sensitive materials and thick sections. It also handles a wider range of materials than many thermal cutting methods, although cutting speed usually decreases as material thickness increases.
CNC Oxy-Fuel Cutting

CNC oxy-fuel cutting first heats carbon steel to its ignition temperature with a fuel-gas flame, then directs a high-purity oxygen jet into the heated zone. The oxygen reacts with the iron and forms oxides, while the gas stream removes the reaction products from the cut. This process works best for carbon and low-alloy steel, especially thick plate, and commonly handles material from about 6 mm to well over 150 mm thick.
Its main advantage is relatively low operating cost for heavy steel sections, and it can process large workpieces effectively. However, oxy-fuel cutting is generally slower than plasma on many medium-thickness jobs and creates a wider heat-affected zone. It also has limited suitability for stainless steel, aluminum, and other metals that do not oxidize in the same way.
Wire EDM Cutting

Wire EDM cuts conductive materials with a thin moving wire and a series of controlled electrical discharges. Instead of pressing a tool against the workpiece, the machine removes material through spark erosion while dielectric fluid cools the cutting zone and flushes away debris. This method works with hardened steel, tool steel, titanium, nickel alloys, and other electrically conductive materials.
A narrow kerf and almost no cutting force make wire EDM suitable for fine profiles, small internal radii, narrow slots, and intricate profiles that are difficult to machine conventionally. Wire diameters commonly range from about 0.1 to 0.3 mm, depending on the required detail. The trade-off is speed, since thick sections and high-accuracy finishing passes can significantly increase cutting time.
| CNC Cutting Process | Principle | Materials | Best For | Main Limitation |
| CNC Milling | Rotating tool | Metals, plastics | 3D features | Tool access |
| CNC Turning | Rotating workpiece | Metals, plastics | Round parts | Rotational shapes |
| CNC Routing | High-speed cutter | Plastics, wood, aluminum | Large panels | Lower rigidity |
| CNC Laser Cutting | Laser beam | Sheet metals | Fine 2D profiles | Heat effects |
| CNC Plasma Cutting | Plasma arc | Conductive metals | Thick plate | Wider kerf |
| CNC Waterjet Cutting | High-pressure jet | Most materials | Heat-sensitive parts | Slower cutting |
| CNC Oxy-Fuel Cutting | Oxygen reaction | Carbon steel | Very thick plate | Limited materials |
| Wire EDM Cutting | Spark erosion | Conductive materials | Fine profiles | Slow speed |
Key Advantages and Limitations of CNC Cutting in Manufacturing
CNC cutting offers clear advantages in repeatability, geometric control, and production consistency, but every process also comes with practical limits. The right choice depends on what the part requires and what the selected cutting method can realistically achieve. The following advantages and limitations show where CNC cutting performs well and where design, material, or process constraints may affect the result.

Advantages of CNC Cutting
CNC cutting gives you more control over geometry, repeatability, and production consistency than manual cutting. The exact benefit depends on the process, but most CNC methods share several advantages that make them suitable for both prototypes and repeat production.
- Wide material compatibility: Different CNC cutting processes can handle aluminum, steel, stainless steel, titanium, copper alloys, engineering plastics, composites, and other materials.
- Consistent repeatability: Programmed machine movements help reproduce the same geometry and dimensions across multiple parts with less manual variation.
- Strong geometric capability: CNC cutting can create 2D profiles, holes, slots, pockets, threads, contours, cylindrical features, and complex multi-axis shapes.
- Flexible production volume: The same digital workflow can support prototypes, small batches, and repeat production without changing the basic manufacturing logic.
- Controllable cutting parameters: Speed, feed, toolpath, power, pressure, and other settings can be adjusted to match the material, geometry, and finish requirements.
Limitations of CNC Cutting
CNC cutting also has practical limits that vary by process. Geometry, material properties, thickness, tolerance, heat input, and setup complexity can all affect whether a method remains suitable and economical for a specific part.
- Process-specific geometry limits: Tool diameter, kerf width, cutting direction, and machine travel can restrict small features, sharp corners, or difficult-to-reach areas.
- Different material restrictions: Some methods only work with conductive metals, while others become less practical as material hardness or thickness increases.
- Higher cost for tight tolerances: Narrow tolerance ranges often require slower cutting, additional setups, finishing passes, and more inspection.
- Possible heat or edge effects: Laser, plasma, and oxy-fuel cutting can create heat-affected zones, while waterjet and plasma may produce taper or rougher edges.
- More complex setup for difficult parts: Irregular shapes, thin walls, large components, or multi-sided features may require special workholding, additional tooling, or multiple setups.
What Machines Are Used for CNC Cutting?
CNC cutting relies on different machine configurations because each process controls motion, tooling, and material in a different way. The machine type determines available axes, workpiece size, achievable geometry, cutting stability, and production efficiency. The main systems range from machining centers and lathes to laser, plasma, waterjet, routing, and EDM equipment.
CNC Milling Machines and Machining Centers

CNC milling machines usually control movement along the X, Y, and Z axes and use a rigid table to support the workpiece. Vertical machining centers provide easy access for general machining, while horizontal machining centers offer better chip evacuation and multi-side access. Spindle power, machine travel, rigidity, table size, and tool capacity directly affect the size and complexity of parts the machine can handle.
CNC Lathes and Turning Centers

CNC lathes hold the workpiece with a chuck or collet and use a tool turret to position different cutting tools. Turning centers may add live tooling, sub-spindles, Y-axis movement, or bar feeders, allowing several operations to run in one setup. These features reduce manual repositioning and help maintain alignment between turned, drilled, or milled features.
Multi-Axis and 5-Axis CNC Machines
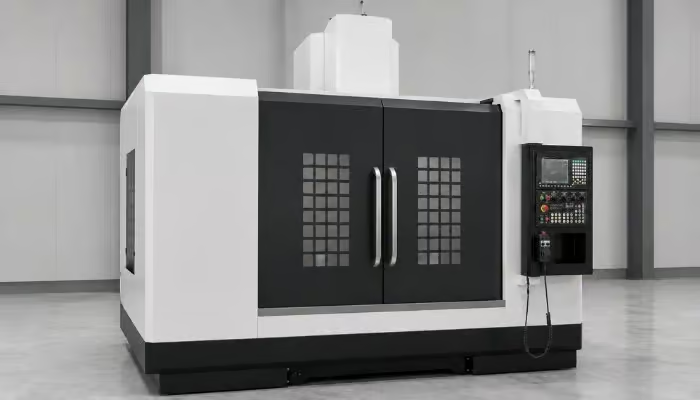
Multi-axis machines add rotary motion to standard linear movement. A 4-axis machine introduces one rotary axis, while a 5-axis machine combines three linear axes with two rotary axes. This configuration gives the cutting tool access to multiple faces and angled features without repeatedly reclamping the part, which can improve feature alignment and reduce setup time.
CNC Laser, Plasma, and Waterjet Systems

Laser, plasma, and waterjet machines commonly use a large cutting bed with a gantry that moves the cutting head across a sheet or plate. The bed size, gantry travel, motion accuracy, source power, and height-control system determine practical part dimensions and cutting capacity. Automated loading or nesting systems can also improve productivity for repeated sheet and plate cutting.
CNC Routers and Wire EDM Machines

CNC routers usually combine a large gantry-style work area with a high-speed spindle, making them suitable for large panels and lighter cutting loads. Wire EDM machines use upper and lower wire guides, a continuous wire-feed system, and a dielectric tank. Independent guide movement can also create tapered profiles, while the machine structure maintains precise control over the wire path.
Common Mechanical CNC Cutting Tools and Their Functions
CNC cutting tools determine how material is removed, what features the machine can create, and what surface finish the process can achieve. Tool geometry, diameter, material, and cutting edge design directly affect accuracy, cutting forces, chip evacuation, and tool life. The following tools are commonly used in CNC milling, turning, drilling, and related mechanical cutting operations.

End Mills and Face Mills
End mills use side and end cutting edges to machine slots, pockets, profiles, shoulders, and contours, while face mills use a wider cutter body with replaceable inserts to machine large flat surfaces efficiently. End mills commonly use helix angles around 30°–45° to improve chip evacuation, while face mills often use 45° or 90° insert approaches to balance cutting force, material removal, and surface finish.
Drills, Reamers, and Boring Tools
Drills create the initial hole and usually use helical flutes with common point angles of 118° or 135° to support penetration and chip evacuation. Reamers then remove a small amount of material to improve hole diameter and surface finish, while boring tools enlarge or correct existing holes with greater control. Together, these tools suit bearing seats, dowel holes, bushings, and other precision-fit features where hole size, alignment, and finish matter.
Turning, Grooving, and Parting Tools
Turning tools normally use single-point carbide inserts to machine external diameters, internal bores, shoulders, tapers, threads, and profiles on rotating parts. Insert geometry changes with the feature and cutting conditions; for example, 35° and 55° insert shapes provide better access for profiling, while stronger insert geometries suit heavier material removal. Nose radius and chip-breaker design also affect surface finish, cutting force, and chip control.
Grooving tools use narrow cutting edges to produce seal grooves, O-ring seats, snap-ring grooves, and relief features with controlled width and depth. Parting tools use a similarly narrow, blade-like geometry to separate finished components from bar stock while limiting material loss. Both operations require stable tool alignment and effective chip evacuation because the cutting zone provides less clearance than general turning.
Thread Mills and Taps
Thread mills use a cylindrical cutter with helical flutes to create internal or external threads, commonly including standard 60° metric and UNC thread forms. Their helical cutting action supports chip evacuation and gives better control when machining harder materials, large thread diameters, or parts where tool breakage would be costly.
Taps cut internal threads directly in a pre-drilled hole and usually work faster for standard sizes such as M6 or 1/4-20 UNC. Straight or helical flute designs help manage chips and reduce cutting load, especially in softer metals.
Chamfer and Form Cutters
Chamfer cutters create angled edges for deburring, countersinking, edge preparation, and assembly clearance, with common included angles such as 60°, 90°, and 120° depending on the feature. Form cutters use a predefined profile to machine radii, grooves, undercuts, or repeated contours in fewer passes. Their main advantage is consistency when the same special geometry appears across multiple parts.
Materials Commonly Used in CNC Cutting
Material choice affects cutting speed, tool wear, edge quality, achievable tolerance, and overall production cost. CNC cutting can process a wide range of metals and engineering plastics, but each material reacts differently to heat, cutting forces, and tool contact. Matching the material with the right cutting process helps improve dimensional control and reduce unnecessary secondary work.

Aluminum Alloys
6061 and 7075 aluminum are widely used for housings, brackets, structural parts, and other precision aluminum components because they combine low weight with good machinability. CNC milling and turning suit pockets, holes, threads, thin walls, and complex contours, while laser or waterjet cutting can handle sheet and plate efficiently when the part mainly requires 2D profiles before secondary machining.
Steel and Stainless Steel
Steel components and stainless steel parts cover a wide range of grades, including 1018, 4140, 304, and 316. Milling and turning are well-suited when a part requires precise holes, threads, bores, or mating surfaces. For sheet and plate, laser and plasma cutting provide faster profile cutting, while oxy-fuel cutting is particularly useful for thick carbon steel sections.
Titanium Alloys
Titanium alloys, especially Ti-6Al-4V, are suitable for CNC cutting but require controlled parameters because low thermal conductivity keeps heat near the cutting zone. CNC milling and turning work well for precision features, while waterjet cutting suits titanium plate when you want to avoid thermal effects. Wire EDM is also effective for detailed profiles because titanium conducts electricity.
Brass and Copper
Brass parts machine cleanly and often appear in fittings, valve components, connectors, and precision hardware. Copper components are more common in electrical contacts, conductive parts, and thermal applications. Milling and turning suit both materials, although copper’s ductility and thermal conductivity can make chip control and surface finish more demanding.
Engineering Plastics
POM, PEEK, nylon, PTFE, and polycarbonate are widely used for engineering plastic parts that need low weight, corrosion resistance, electrical insulation, or low friction. CNC milling and routing are often the best choices for pockets, holes, profiles, and contours. Heat buildup and clamping force need careful control because plastics can deform or melt more easily than metals.
How Do You Choose the Right CNC Cutting Process?
Choosing the right CNC cutting process depends on the part shape, stock form, accuracy requirements, and overall production cost. No single method fits every project. A process that works well for flat sheet may be inefficient for a complex 3D component, while a high-precision method may add unnecessary cost to a simple profile.

Part Geometry
Part geometry often determines the most practical CNC cutting method. You should first look at whether the part is flat, rotational, three-dimensional, or requires narrow internal features, because each process handles these shapes differently.
- Flat profiles: Laser, plasma, and waterjet cutting suit sheet and plate parts with 2D outlines.
- Rotational shapes: CNC turning works best for shafts, pins, bushings, sleeves, and similar round parts.
- 3D features: CNC milling suits pockets, holes, slots, angled faces, and complex contours.
- Fine internal features: Wire EDM works well for narrow slots, detailed profiles, and sharp internal geometry in conductive materials.
Material Form and Thickness
Material form and thickness can quickly narrow the available CNC cutting options. Sheet, plate, bar, tube, and billet stock each suit different processes, while increasing thickness usually reduces cutting speed and changes edge quality, kerf, and cost. A practical comparison can use the following ranges:
- Thin sheet, below about 6 mm: Laser cutting usually offers fast cutting, narrow kerf, and detailed 2D profiles.
- Medium plate, about 6–25 mm: Laser, plasma, or waterjet cutting may all work, depending on material, tolerance, and edge requirements.
- Thick plate, about 25–50 mm: Plasma and waterjet become more practical for many applications; plasma systems commonly support recommended cutting capacities into the 30–40 mm range.
- Very thick steel, above about 50 mm: Waterjet or oxy-fuel cutting often makes more sense, especially for heavy carbon steel sections.
- Bar, billet, and block stock: CNC milling or turning usually provides better control when the finished part needs pockets, bores, threads, shoulders, or other dimensional features.
Accuracy and Surface Requirements
Tolerance and surface finish requirements often eliminate unsuitable cutting methods early. If the part includes mating surfaces, precision holes, bearing fits, or other controlled dimensions, milling or turning usually provides better dimensional control than profile-cutting methods. General dimensional tolerances may also follow standards such as ISO 2768 when a drawing does not specify an individual tolerance for every dimension.
- Tight tolerances, around ±0.01–0.05 mm: CNC milling or turning is usually the better choice for precision features and finished dimensions.
- Moderate tolerances, around ±0.1 mm: Laser cutting can suit many sheet-metal profiles when edge quality and heat effects remain acceptable.
- Looser tolerances, around ±0.5 mm or above: Plasma or oxy-fuel cutting may be sufficient for structural plate and rough-profile applications.
Production Volume and Cost
Production volume affects setup cost, cycle time, tooling use, and unit price. For small batches, flexible processes with low setup requirements usually make more sense, while larger volumes favor faster cutting methods that reduce cost per part. You should compare total production cost rather than cutting speed alone.
- Prototypes and small batches: CNC milling, turning, waterjet, and laser cutting offer good flexibility without dedicated tooling.
- Medium-volume production: CNC milling and turning become cost-effective for repeat precision parts, while laser cutting suits repeated sheet-metal profiles.
- Large-volume sheet parts: Laser cutting usually provides fast cycle times and lower unit cost for thin and medium sheet.
Common Applications of CNC Cutting Across Different Industries
CNC cutting supports industries that need controlled dimensions, repeatable geometry, and efficient material removal. The right process depends on part shape, material, tolerance, and production volume. Typical applications range from aerospace parts and automotive components to medical devices, electronic housings, robotic structures, and industrial machinery parts.
Aerospace

Aerospace production often relies on aluminum, titanium, stainless steel, and high-performance alloys. CNC milling and 5-axis machining suit aerospace machined parts such as brackets, housings, structural components, and complex multi-surface parts, while waterjet or laser cutting can prepare sheet and plate blanks before further machining.
Automotive Manufacturing

CNC cutting supports automotive CNC parts including shafts, transmission components, housings, brackets, fixtures, and prototype parts. Turning suits rotational components, while milling handles complex housings and mounting features. Laser and plasma cutting also work well for sheet-metal brackets, panels, and structural profiles.
Medical Devices

Medical parts often require small features, controlled tolerances, and materials such as stainless steel, titanium, and engineering plastics. Milling, turning, and wire EDM can produce medical device components such as surgical instrument parts, precision housings, mechanisms, and implant-related parts where dimensional control matters.
Electronics and Instrumentation

CNC cutting is widely used for electronic enclosure parts and related components such as heat sinks, mounting brackets, connector parts, panels, and precision housings. Milling creates pockets and mounting features, while laser cutting handles thin sheet covers and panels efficiently.
Robotics and Automation

Robotics and automation systems rely on robotics components such as joints, shafts, mounting plates, brackets, housings, and actuator parts. Milling and turning provide the dimensional control needed for bearing fits and alignment features, while laser or waterjet cutting can prepare structural plates before secondary machining.
Industrial Machinery and Equipment
Industrial equipment often requires industrial machinery parts such as shafts, flanges, tooling plates, fixtures, guards, housings, frames, and replacement components. Milling and turning complete precision interfaces, while plasma, waterjet, and oxy-fuel cutting can prepare larger plate sections before final machining.
How Can You Design Parts for Better CNC Cutting Results?
Good part design can reduce cutting time, tool wear, setup complexity, and unnecessary secondary work. You should match geometry, tolerances, access, workholding, and surface requirements to the limits of the selected CNC process. Small design changes often make a part easier to cut without changing its function.

Add Internal Corner Radii
Avoid specifying perfectly sharp internal corners unless the function truly requires them. Milling and routing tools always leave a radius based on cutter diameter, while wire EDM also has a minimum internal radius determined by wire diameter and spark gap. Laser, plasma, and waterjet can create smaller radii, but kerf width still limits extremely fine corners. Practical radii improve cut consistency and reduce secondary finishing.
Set Practical Tolerances
Apply tight tolerances only to dimensions that affect fit, alignment, sealing, or function. Extremely narrow tolerances often require slower cuts and additional finishing passes. Engineering drawings can use standardized GD&T practices, such as those defined in ASME Y14.5, to communicate these requirements clearly. Practical tolerances allow more stable cutting conditions and make it easier to maintain consistent dimensions across repeated parts without unnecessary corrections during production.
Improve Tool Access
Provide enough access for the cutting tool, cutting head, or wire to reach each feature without interference. Milling needs clearance for cutter diameter and tool length, while laser, plasma, and waterjet require suitable lead-in paths and enough spacing between nearby features. Wire EDM also needs a practical wire path and, for enclosed internal profiles, a starter hole. Better access improves cutting stability and feature accuracy.
Plan for Workholding
Include stable surfaces that allow the workpiece to remain firmly supported throughout cutting. Thin sections or poorly positioned features can flex under cutting forces and shift the final dimensions. Stable workholding reduces vibration and part movement, helping maintain flatness, feature position, and dimensional repeatability from one component to the next.
Define Surface Finish Requirements
Specify surface finish only where the part function requires it. Critical sealing, sliding, bearing, or visible surfaces may need additional finishing passes, while non-functional areas can accept standard machining marks. Clear finish requirements help select suitable cutting parameters and toolpaths, producing the required surface quality without adding unnecessary machining operations.
Get Custom CNC Cutting Support from DZ Making
DZ Making supports custom CNC cutting projects for metal and engineering plastic parts, including profiles, slots, holes, contours, and other machined features. We can review your part geometry, material, tolerance, thickness, and production volume to determine whether milling, turning, or another CNC cutting approach fits the project requirements.
Send us your CAD file, technical drawing, material grade, quantity, tolerance, and surface requirements for evaluation. We can help you select a practical CNC cutting process, reduce unnecessary machining steps, and prepare a production plan that balances accuracy, cutting quality, and cost.
Conclusion
CNC cutting covers a wide range of computer-controlled processes, from milling and turning to laser, plasma, waterjet, oxy-fuel, routing, and wire EDM. Each method has different strengths in geometry, material compatibility, thickness range, tolerance, edge quality, and production cost, so the best choice depends on the actual requirements of the part rather than the process name alone.
For custom parts, you should evaluate the design, stock form, accuracy requirements, and production volume before selecting a CNC cutting process. A well-matched process can reduce secondary machining, improve consistency, and control total production cost while delivering the required part quality.
FAQs
1. Which CNC cutting process offers the highest accuracy?
CNC milling, turning, and wire EDM generally provide tighter dimensional control than plasma or oxy-fuel cutting. The best choice depends on part geometry, material, feature size, and whether the design requires profiles, bores, threads, or 3D surfaces.
2. Which CNC cutting method works best for thick metal?
Plasma and waterjet cutting work well for many medium-to-thick metal plates, while oxy-fuel cutting is especially suitable for very thick carbon steel. Waterjet becomes useful when the part must avoid heat-affected zones or thermal distortion.
3. Can CNC cutting process plastics?
Yes. CNC cutting can process engineering plastics including POM, PEEK, nylon, PTFE, polycarbonate, and acrylic. Milling and routing suit pockets, holes, profiles, and contours, but cutting speed, heat buildup, and clamping pressure require careful control.
4. Is laser cutting cheaper than plasma cutting?
For thin to medium sheet metal, laser cutting is often more cost-effective because of its speed and narrow kerf. For thick plate, plasma cutting usually becomes the more economical option, since laser cutting speed and cost efficiency drop as thickness increases. The right choice depends on material thickness, required tolerance, and production volume rather than cost alone.
