
CNC Plastic Machining Services
Custom plastic parts require machining plans that reflect material behavior, critical tolerances, and functional requirements. As a CNC plastic machining manufacturer, we support prototypes, low-volume orders, and repeat production from your CAD files and technical drawings, with the machining approach adapted to each part’s material and geometry.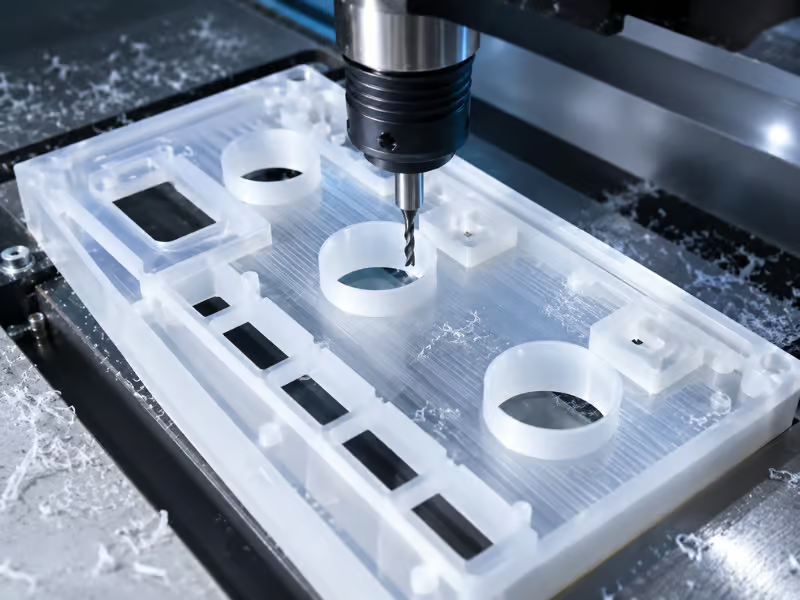
Plastic CNC Machining Capabilities
| Item | Capability |
|---|---|
| Machining Processes | CNC milling, turning, drilling, tapping, boring, grinding |
| Axis Capability | 3-axis, 4-axis, 5-axis, turn-mill machining |
| Plastic Materials | POM/Delrin, Nylon, PEEK, ABS, PTFE, PC, PMMA, UHMWPE, HDPE, PVC, PVDF, G10/FR4 |
| Typical Tolerance | ±0.02–0.05 mm |
| Tight Tolerance | ±0.01 mm |
| Surface Roughness | Ra 0.8–3.2 μm as-machined |
| Maximum Milling Capacity | 1200 × 700 × 500 mm |
| Maximum Turning Capacity | Ø450 × L600 mm |
| Production Support | Prototypes, low-volume orders, and batch production |
| MOQ | Project-based; confirm part design, material, and required quantity in the RFQ |
| Prototype Lead Time | 3–7 days |
| Production Lead Time | 3–5 weeks |
| Inspection | FAI, CMM, dimensional gauges, thread testing, sampling inspection |
| Documents | Supplier material report, inspection report, packing list, and invoice upon request |
| Accepted Project Data | 3D CAD files and 2D technical drawings |
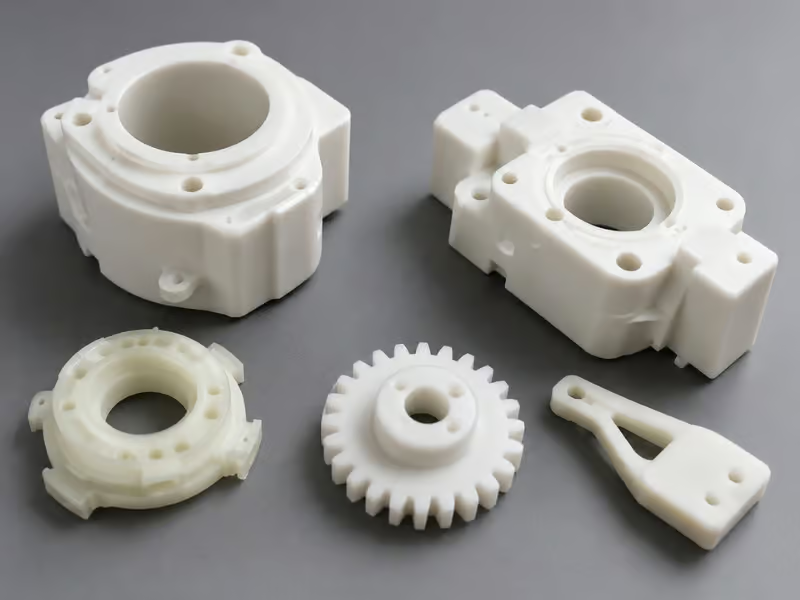
Explore Plastic Materials for CNC Machining
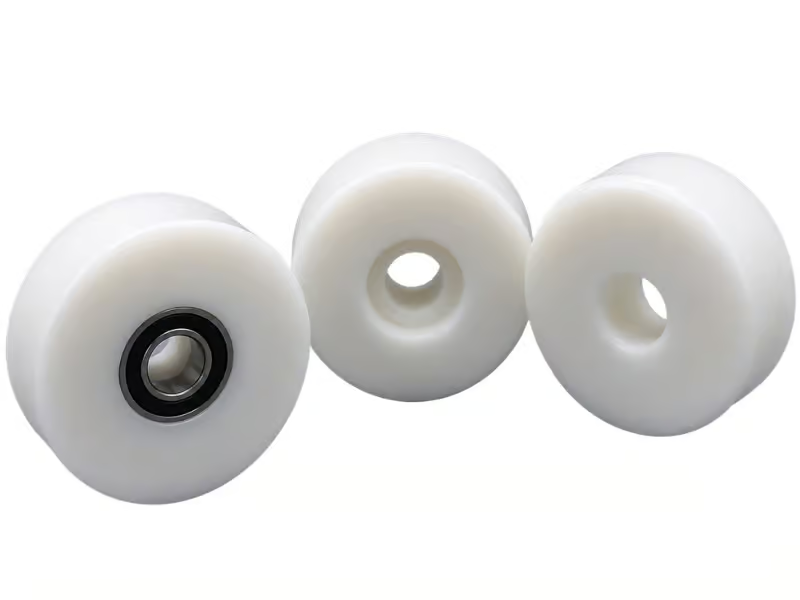
POM / Delrin CNC Machining
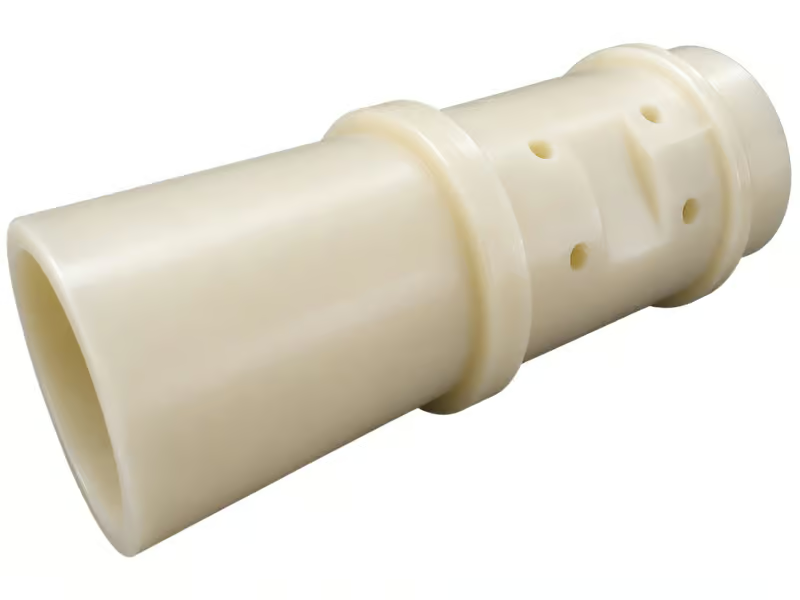
Nylon CNC Machining
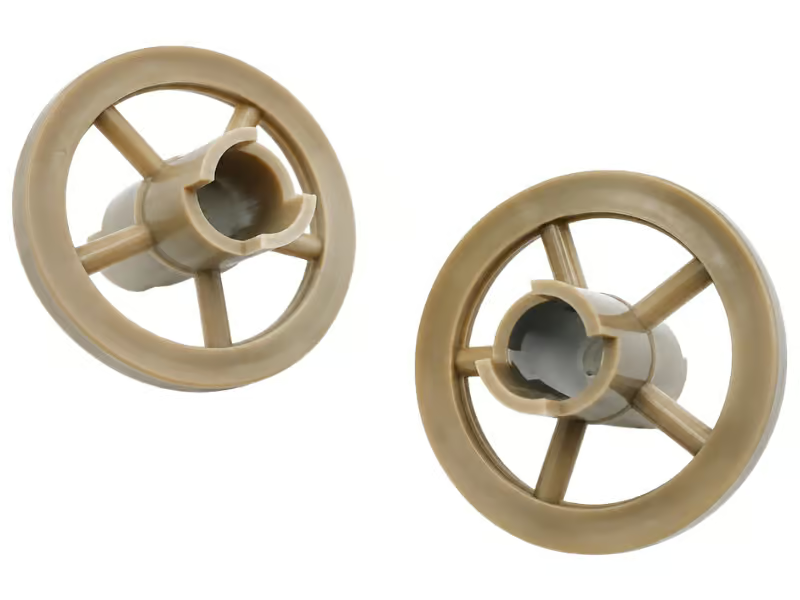
PEEK CNC Machining
ABS CNC Machining
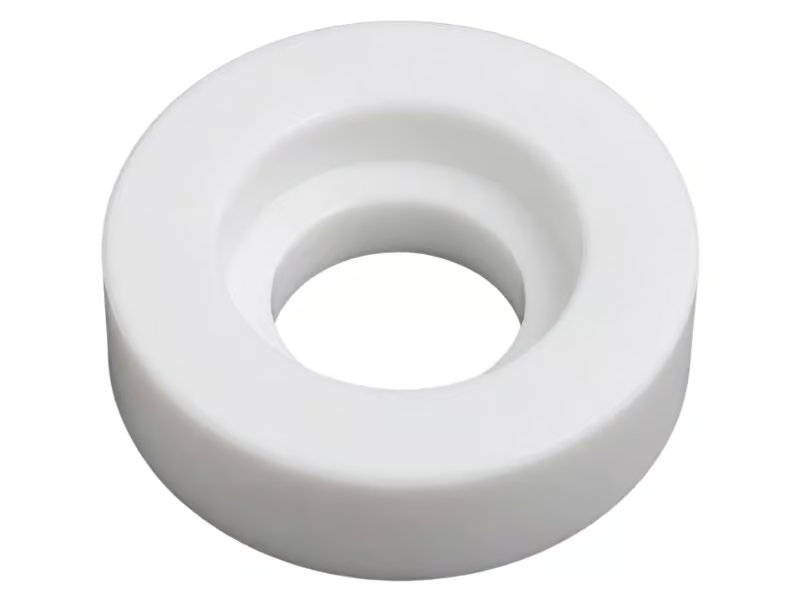
PTFE CNC Machining
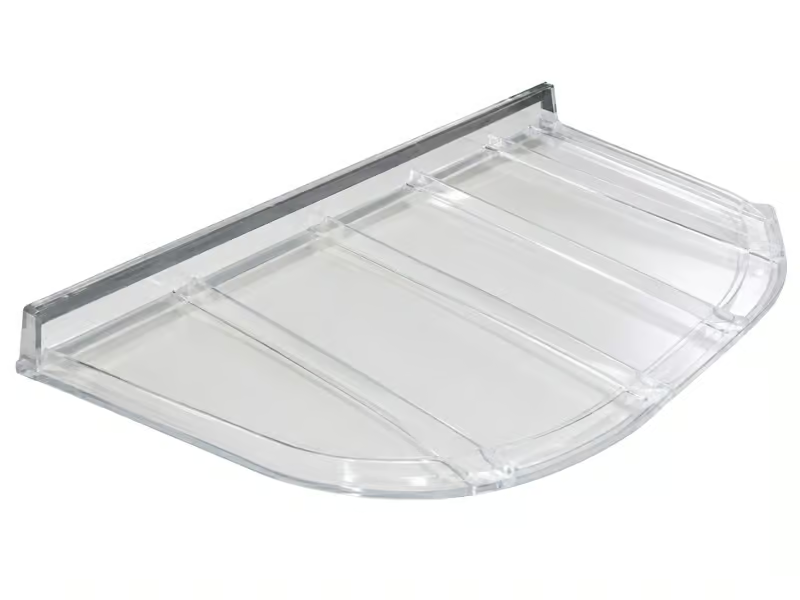
Polycarbonate CNC Machining
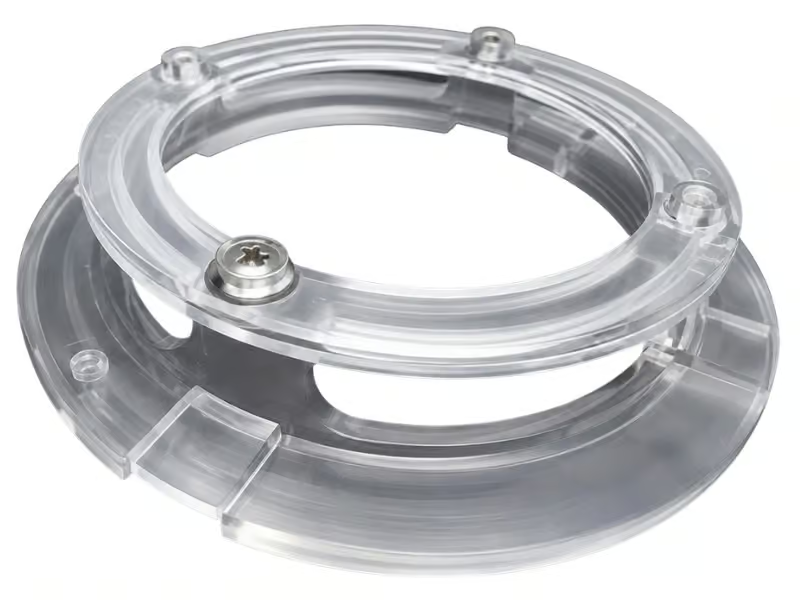
Acrylic / PMMA CNC Machining
UHMWPE CNC Machining
HDPE CNC Machining
PVC CNC Machining
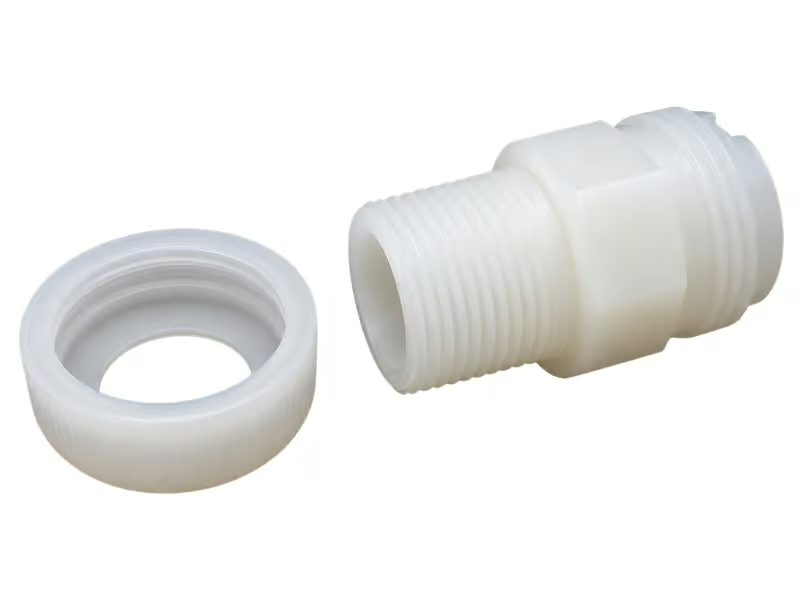
PVDF CNC Machining
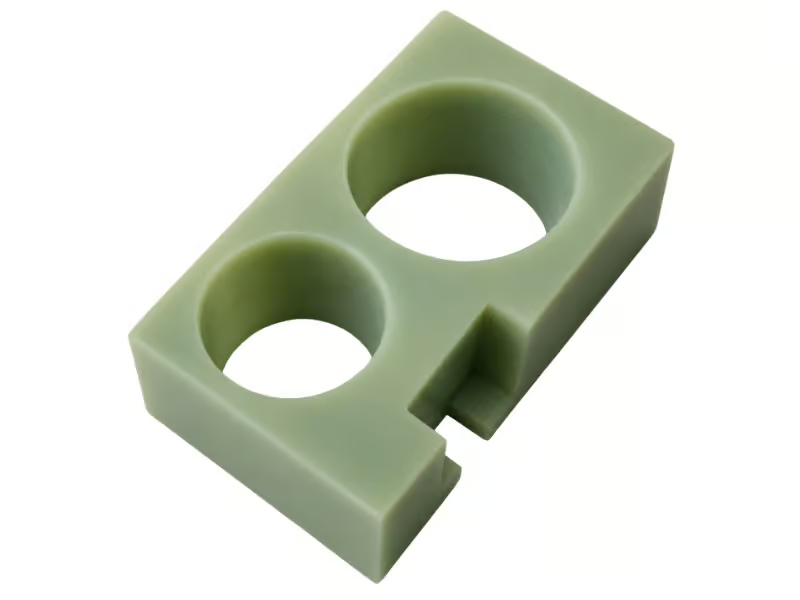
G10 / FR4 CNC Machining
Get an Engineering-Reviewed Quote for Your Plastic Parts
How Do We Control Common Plastic Machining Challenges?
Machining plastic parts requires careful control of heat, clamping, and material removal. We adjust tooling, workholding, and machining sequence according to the plastic grade and part geometry.
Heat Buildup and Dimensional Change
Plastics dissipate heat less efficiently than metals, so excessive cutting heat can affect surface condition and dimensions, especially on thin features. In CNC plastic machining, tooling, cutting parameters, chip evacuation, engagement, and finishing passes are controlled to limit heat buildup and maintain dimensional stability.
Warping and Clamping Deformation
Softer plastics and thin-wall parts can deform under excessive clamping force, while insufficient support may allow movement during cutting. Wider contact areas, soft jaws, or added support can reduce local pressure on machined plastic parts, while roughing most material first and leaving a lighter finishing pass can improve dimensional stability.
Burrs, Cracking and Edge Quality
Soft plastics may produce burrs or stringing, while brittle materials can chip or crack around holes, thin edges, or poorly supported features. Sharp, material-suitable tools, controlled feed rates, stable support, and suitable entry and exit paths help reduce edge damage, while deburring or edge breaking improves the final condition of CNC machined plastic parts.
Quality Inspection of Machined Plastic Parts
We inspect machined plastic parts against the approved drawing at key production stages, checking material grade, critical dimensions, hole and thread sizes, flatness, and visible defects such as burrs, cracks, or scratches. Measurement methods are selected by feature and tolerance, using CMM, micrometers, pin gauges, thread gauges, and other suitable tools; dimension-sensitive plastic parts may also be allowed to stabilize after machining and unclamping before final inspection.


Machining Strategies for Different Plastic Behaviors
Different plastics respond differently to cutting heat, clamping pressure, chip formation, and material removal. We support CNC plastic machining with milling, turning, drilling, threading, grinding and multi-axis machining, adapting tooling, workholding, cutting parameters, and machining sequence to the material and part geometry.
Softer plastics such as HDPE may require broader support, sharp tooling, and controlled cutting conditions to limit deformation and burr formation during HDPE machining, while brittle or heat-sensitive grades need more controlled tool engagement, chip evacuation, and finishing conditions. For complex machined plastic parts, 4-axis or 5-axis machining can reduce setups and repeated clamping, helping maintain critical feature relationships.
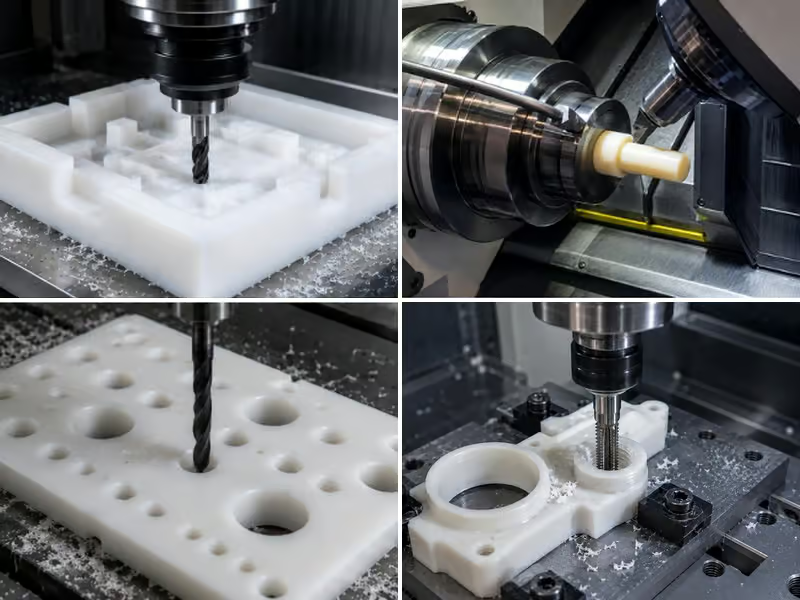
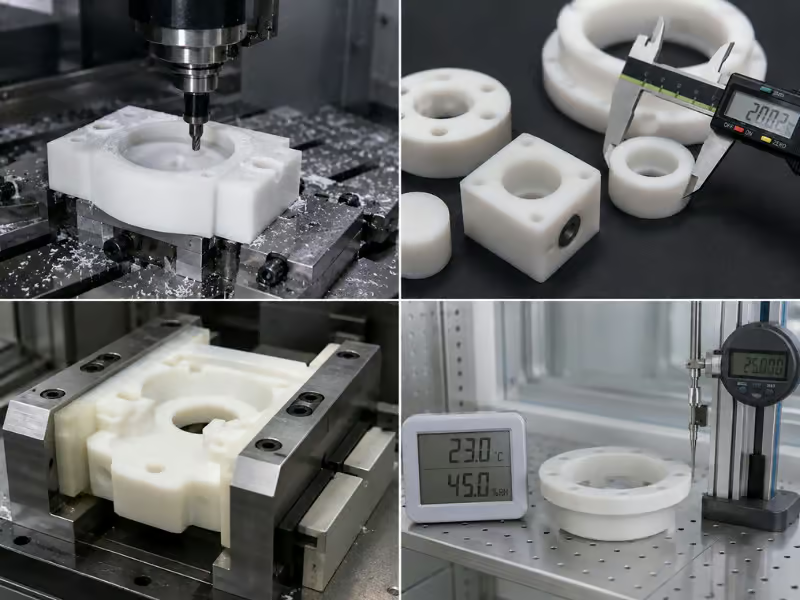
Dimensional Control in CNC Machined Plastic Parts
Plastic dimensions can shift during machining, unclamping, and inspection. We plan roughing, finishing, workholding, and measurement around each material so critical features reach the required size in the finished condition.
- Roughing and Finishing: Heavy material removal can shift the part as stress is released, so critical bores, faces, and profiles are left with allowance for final machining.
- Critical Feature Sizing: Tight-fit bores, diameters, sealing faces, and mating surfaces receive controlled finishing cuts rather than reaching final size during rough machining.
- Controlled Workholding: Soft jaws, broader contact areas, and added support help reduce deformation in PTFE, UHMWPE, nylon, and thin machined plastic parts.
- Material Condition: Moisture-sensitive nylon and thermally responsive plastics require closer control of material and measurement conditions when dimensions directly affect fit or assembly.
- Final Stabilization: Dimension-sensitive CNC machined plastic parts are checked after machining heat dissipates and clamping force is removed, helping final inspection reflect the stable part condition.
Material-Specific Post-Machining for CNC Plastic Parts
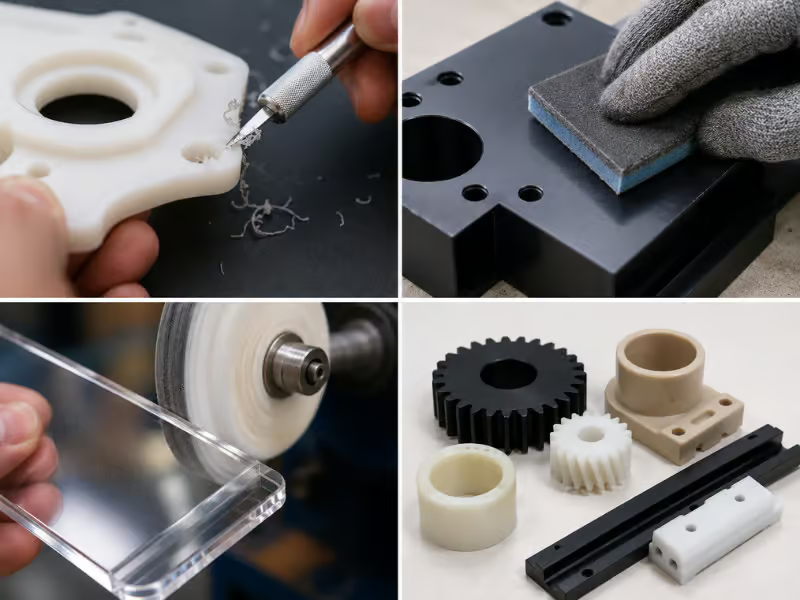
We support deburring, sanding, polishing, painting, and part marking for CNC machined plastic parts, selecting each post-machining operation according to the plastic grade, surface condition, and functional or appearance requirements.
- Edge Cleanup: PTFE, PE, and some nylons may leave soft or stringy burrs after machining. Controlled deburring removes residual material while avoiding excessive rounding of critical edges.
- Surface Smoothing: Sanding can reduce light tool marks or prepare compatible plastics such as ABS for coating, while pressure and abrasive selection should remain controlled to avoid heat or uneven surfaces.
- Clear Edge Polishing: Acrylic / PMMA edges can be polished when improved clarity or smoother exposed surfaces are required, with heat carefully controlled to prevent whitening, distortion, or surface damage.
- Functional Surfaces: POM and PEEK parts often remain as-machined where dimensional accuracy, fit, wear, or low-friction performance matters more than cosmetic appearance.
- Part Marking: Laser marking or other identification methods can add part numbers, serial codes, or logos to suitable CNC machined plastic parts, depending on resin type, color, and surface condition.
Customer Feedback on Our CNC Plastic Machining
As a CNC plastic machining supplier, we support customers with custom parts that must meet specific drawing, fit, and assembly requirements. Feedback often focuses on dimensional accuracy, assembly performance, and consistency from initial samples to repeat orders.
The POM guide blocks from DZ Making matched the mounting holes and sliding dimensions on our drawing. The sample fitted our assembly without modification, and the repeat order remained consistent with the approved parts.

We ordered PEEK insulating spacers from DZ Making with several critical bore and thickness requirements. The parts arrived with the requested inspection results, and the production batch matched the dimensions approved during sampling.

DZ Making machined our acrylic equipment covers from revised CAD files after the prototype review. The final parts had clean edges, accurate hole positions, and fitted the enclosure correctly during assembly.

Custom CNC Plastic Parts for Different Applications
Custom plastic machining supports a wide range of mechanical, electrical, and fluid-handling requirements. Common machined plastic products include precision moving parts, insulating components, and chemical-resistant parts used in functional assemblies.
01
02
03
FAQs
Can plastic be CNC machined?
Yes. CNC milling, turning, and drilling can machine POM, nylon, PEEK, ABS, PTFE, acrylic, and other engineering plastics. Cutting conditions should match each material’s stiffness, heat response, and dimensional stability.
There is no single best option. POM suits stable precision parts, nylon wear components, PEEK demanding environments, PTFE low-friction applications, and acrylic or PC transparent parts.
Yes. Acrylic can be CNC milled and drilled for windows, covers, panels, and display parts. Controlled tooling, support, and cutting conditions help reduce cracking, chipping, and heat buildup.
Typical tolerances are ±0.02–0.05 mm, with tighter tolerances down to ±0.01 mm on suitable features. Actual capability depends on material, geometry, wall thickness, and inspection requirements.
Yes. We machine PEEK, PTFE, nylon, and Delrin parts, with machining parameters and tolerance planning adjusted to each material’s stiffness, heat response, and dimensional behavior.
Send your 3D CAD file, 2D drawing, plastic grade, quantity, tolerances, surface requirements, and inspection needs for an accurate CNC plastic machining services quote.
Packaging depends on part geometry and surface sensitivity. Precision, thin, or transparent plastic parts may use protective film, separation, trays, or cushioning to prevent scratches, bending, and impact.
How to Choose the Right Plastic for CNC Machining?
Choosing the right plastic depends on the part’s function, operating environment, and dimensional requirements. Material selection should balance end-use performance with how each material behaves during CNC plastic machining.
- Mechanical Load and Wear: Choose POM for low-friction precision parts such as gears and bushings, nylon for tougher wear components, and PEEK when higher strength and demanding operating conditions are required.
- Temperature and Chemical Exposure: PEEK suits higher-temperature applications, PTFE works well where low friction and broad chemical resistance matter, while PVDF is often selected for chemical and fluid-handling parts.
- Moisture and Dimensional Stability: POM is a practical choice for dimension-critical parts because of its low moisture absorption, while nylon requires more consideration where humidity may affect tight fits or tolerances.
- Electrical or Optical Requirements: G10/FR4, PTFE, and PEEK suit different insulating applications, while acrylic offers higher optical clarity and polycarbonate provides better impact resistance for transparent parts.
- Machinability and Cost: ABS and POM are practical choices for many prototypes and general-purpose custom plastic parts, while higher-cost materials such as PEEK should be selected when their performance is functionally necessary.
CNC Machining vs Injection Molding: Which Is Better for Plastic Parts?
CNC machining and injection molding can both produce functional plastic parts, but they suit different project conditions. The better choice depends on design maturity, production volume, lead time, cost structure, and part geometry.
Design Flexibility and Product Development
CNC machining works well during product development because revised CAD files can move directly into the next machining iteration. Engineers can change dimensions, hole positions, interfaces, or other features between batches with relatively little disruption. Injection molding is better suited to mature designs where major geometry changes are unlikely after production begins.
Cost, Lead Time, and Production Volume
CNC plastic machining generally has a lower initial investment and can deliver prototypes or lower-volume batches without a lengthy production setup. Its unit cost remains relatively dependent on machine time and material usage. Injection molding requires greater upfront investment and preparation time, but its unit cost can fall substantially once production reaches sufficiently high and repeatable volumes.
Part Geometry and Manufacturing Requirements
CNC machining suits custom plastic parts with thick sections, deep pockets, precise bores, threaded features, tight fits, or geometry that can be efficiently cut from solid stock. Injection molding favors parts designed with more consistent wall thickness, draft angles, molded ribs, and geometry that supports reliable filling, cooling, and ejection.
What Affects Plastic CNC Machining Cost?
The cost of plastic CNC machining depends on material choice, part geometry, machining time, tolerance requirements, and order quantity. Each of these factors changes the amount of material, machine time, setup work, or inspection needed.
- Material Grade and Stock Size: High-performance plastics such as PEEK or PVDF cost more, but stock utilization also matters. Oversized blanks, thick sections, or heavy material removal increase both material waste and machining time.
- Geometry and Machining Access: Deep pockets, thin walls, narrow slots, small internal radii, and multi-sided features may require longer tools, slower cutting, added support, or extra setups, increasing machining time.
- Tolerance Distribution: Tight tolerances throughout the drawing increase the number of finishing passes and inspection effort. Applying them only to functional fits, bores, sealing faces, and mating features can control cost more effectively.
- Setup and Part Orientation: Features that cannot be completed in one setup may require repositioning, dedicated fixtures, and repeated datum alignment, adding labor, machine time, and inspection steps.
- Quantity and Repeatability: Prototype orders spread programming, setup, and first-part inspection across fewer pieces. Larger or repeat orders can spread these preparation costs across more CNC-machined plastic parts.
- Secondary and Inspection Requirements: Polishing, inserts, marking, special deburring, detailed inspection reports, or additional dimensional checks add processing steps beyond the core machining cycle.
