
Custom CNC Machined Shafts
DZ Making manufactures custom machined shafts to your drawings and application requirements, including stepped diameters, bearing journals, threads, keyways, grooves, bores, and other non-standard features. With CNC turning, milling, grinding, and secondary machining support, we help you achieve the required fit, runout, concentricity, surface finish, and dimensional accuracy for prototypes, low-volume orders, and repeat production.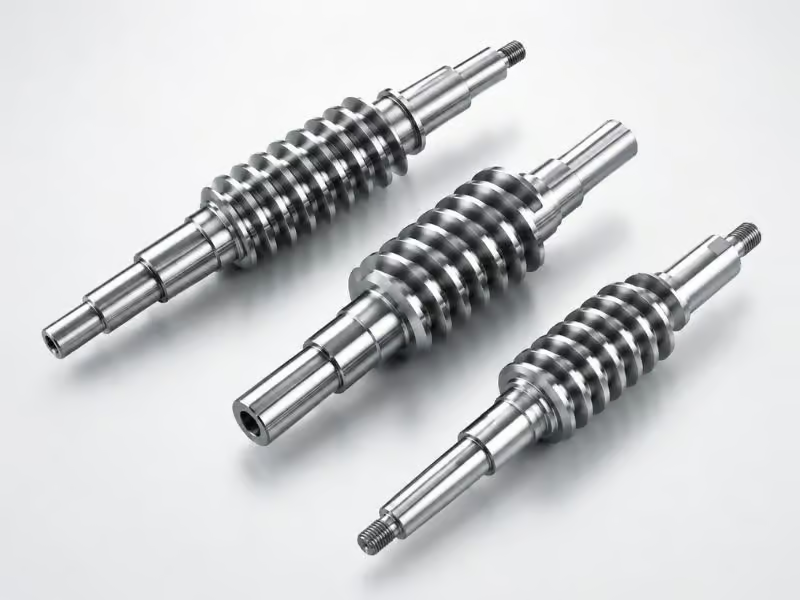
Custom Machined Shaft Capabilities at a Glance
| Parameter | Capability |
|---|---|
| Processes | CNC turning, milling, drilling, grinding |
| Shaft Diameter | Up to Ø200 mm |
| Shaft Length | Up to 500 mm |
| Turning Tolerance | Up to ±0.025 mm |
| Grinding Tolerance | ±0.002–±0.005 mm |
| Concentricity | 0.01–0.03 mm |
| Surface Roughness | Ra 0.2–0.8 μm |
| Features | Steps, journals, keyways, grooves, threads, bores |
| Materials | Steel, stainless steel, aluminum, titanium, copper alloys |
| Production Volume | Prototype to repeat production |
| Inspection | CMM, micrometers, gauges, roughness testing |
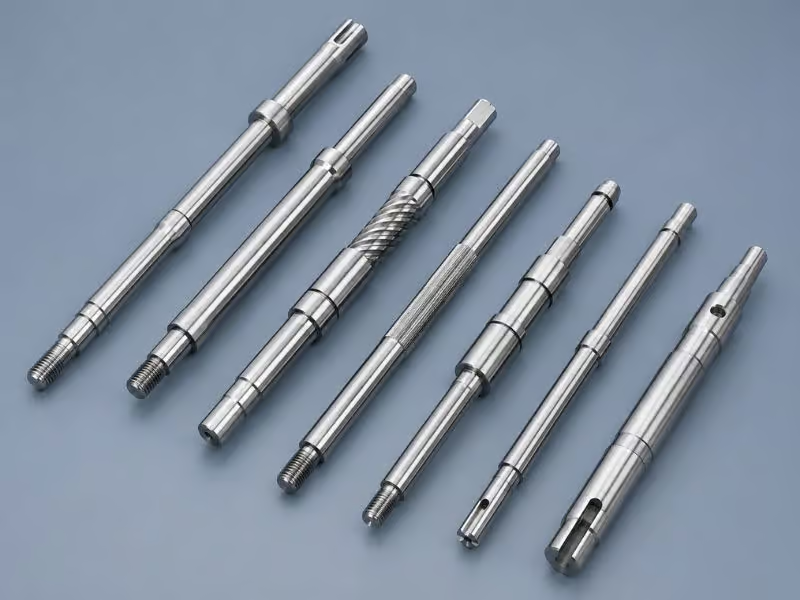
Types of Custom Machined Shafts We Manufacture
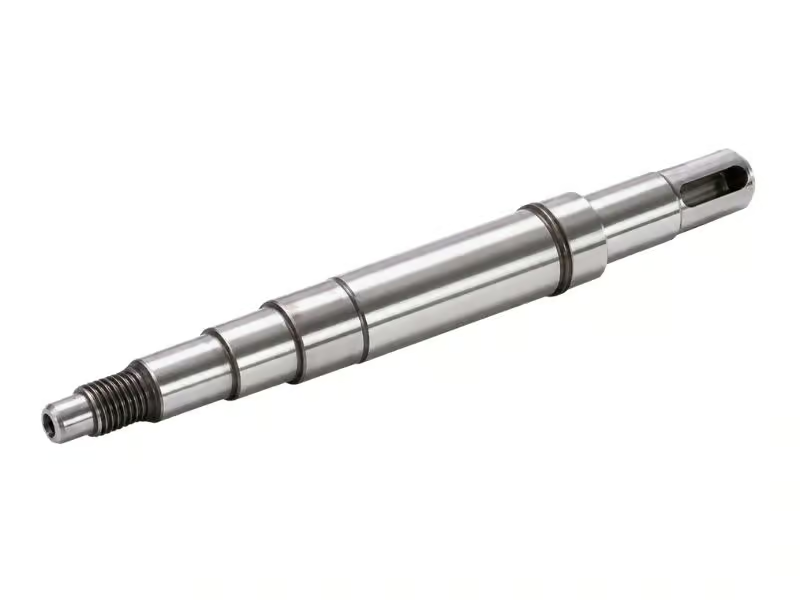
Stepped Shafts
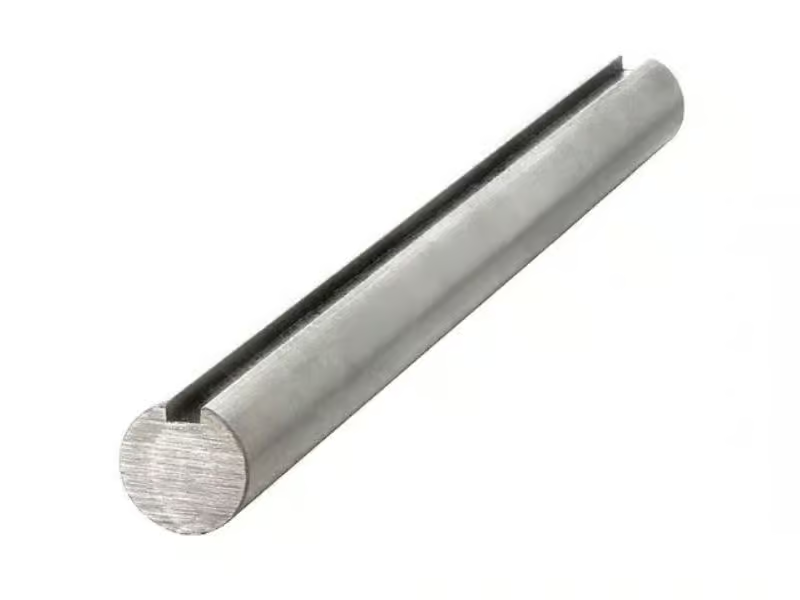
Keyed Shafts
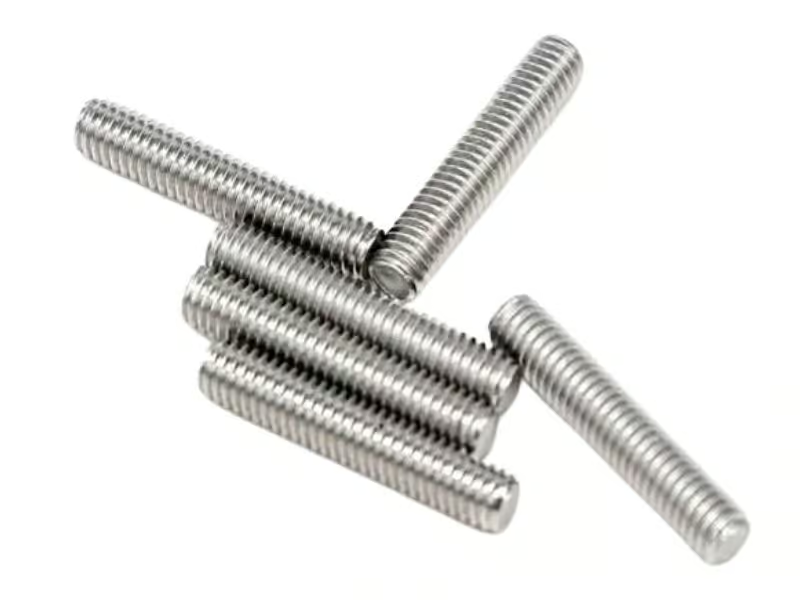
Threaded Shafts
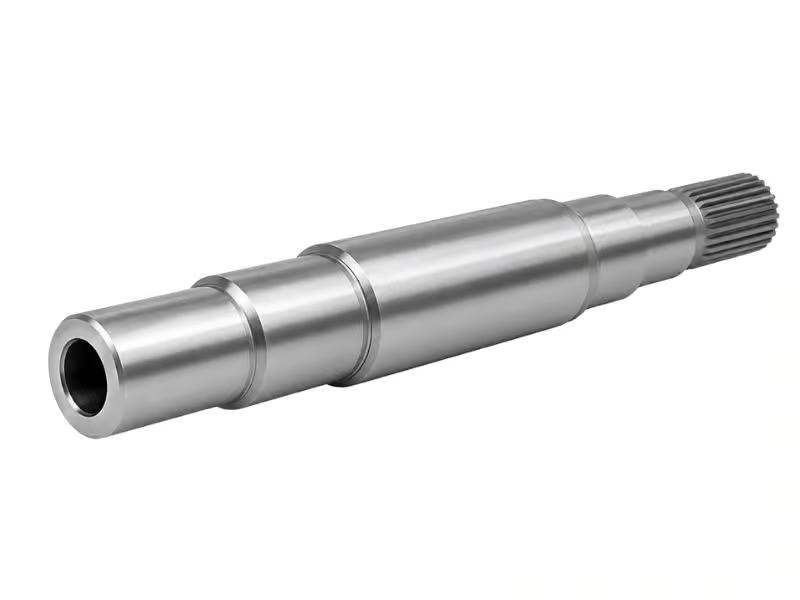
Hollow Shafts
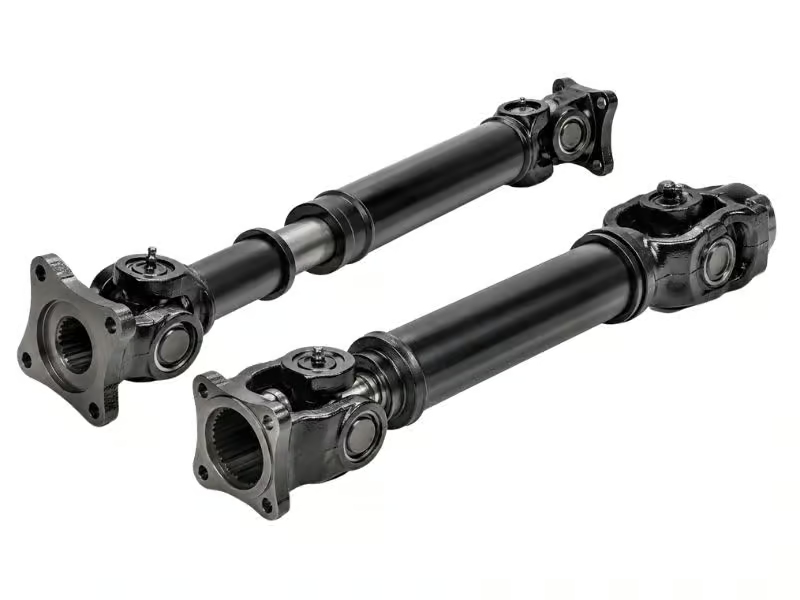
Drive Shafts
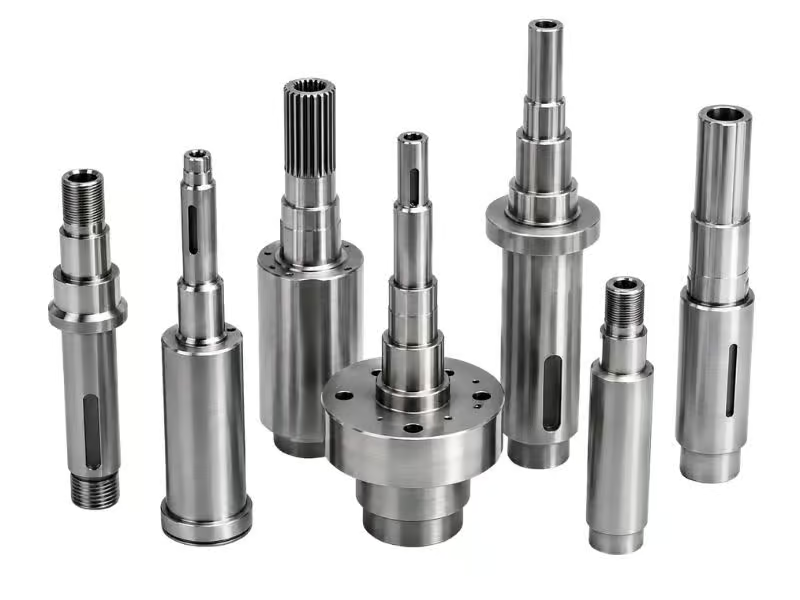
Motor Shafts

Spindle Shafts
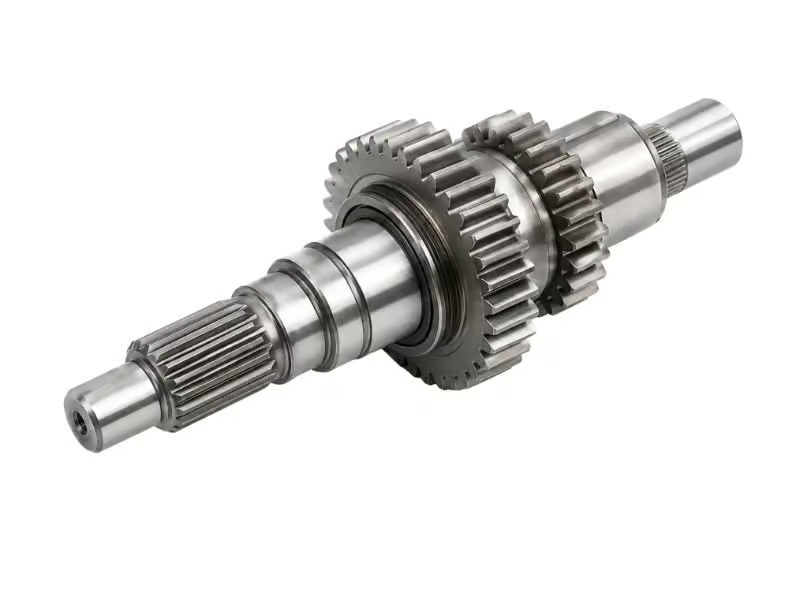
Gear Shafts
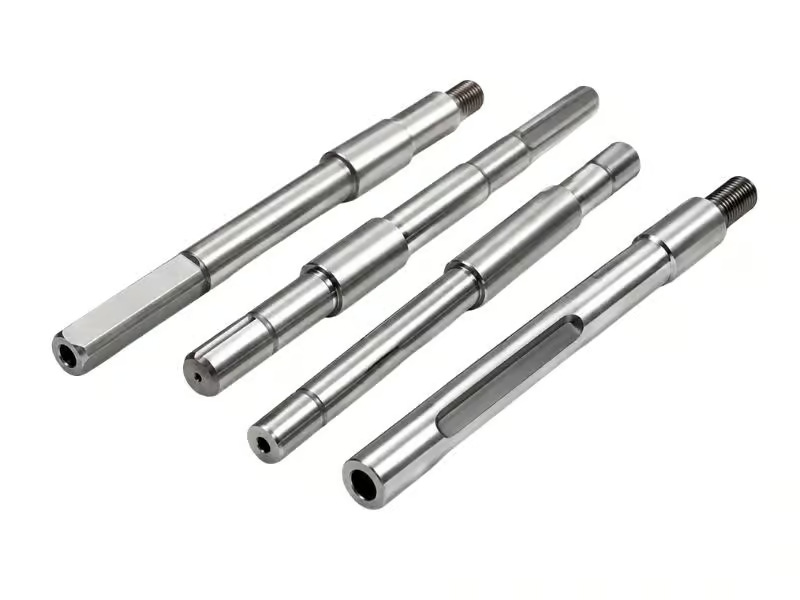
Pump Shafts
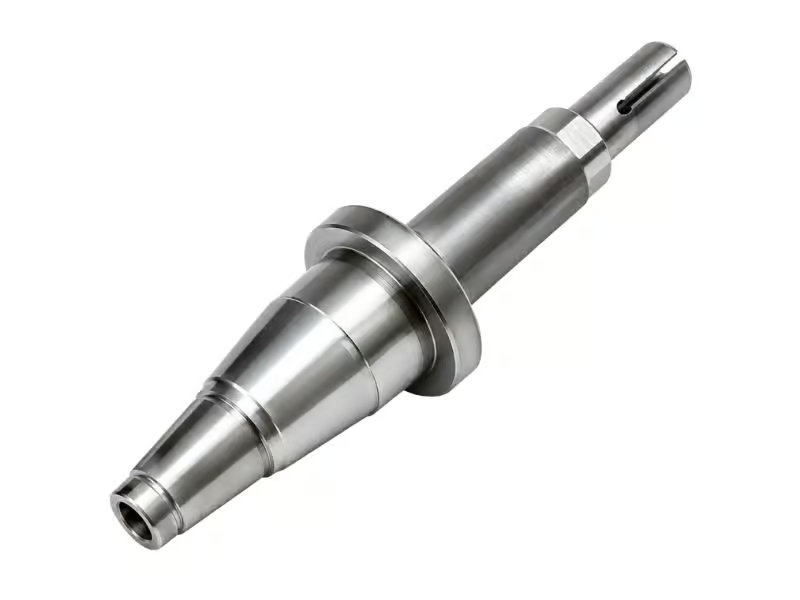
Tapered Shafts
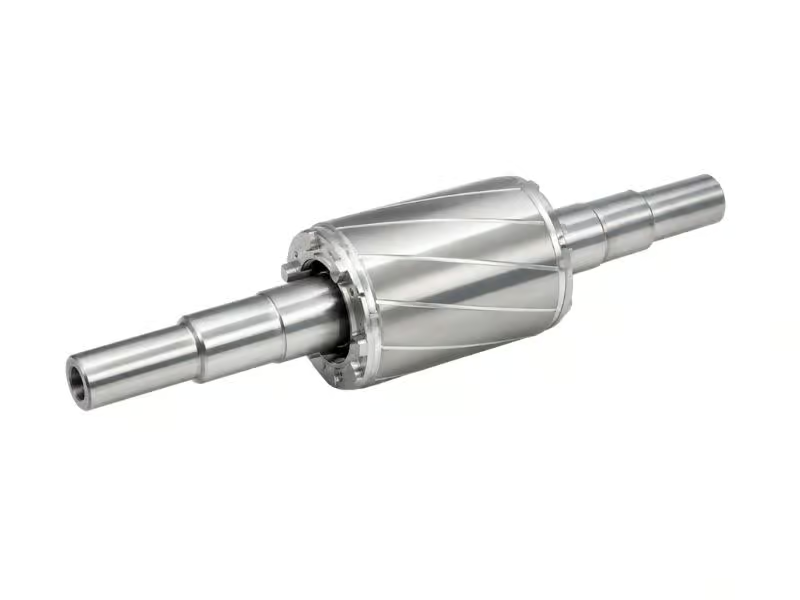
Rotor Shafts
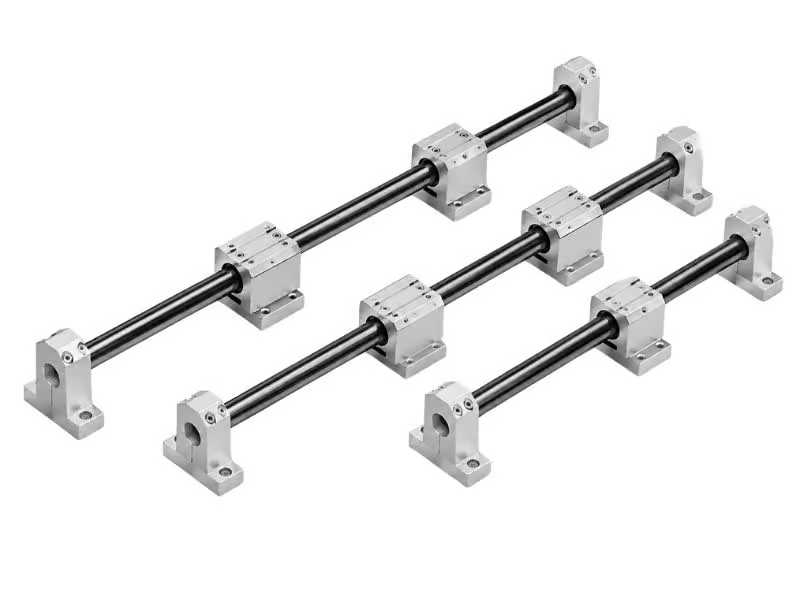
Linear Motion Shafts
Start Your CNC Shaft Machining Project with DZ Making
Critical Features and Tolerances in Precision Shaft Machining
Critical shaft features such as concentricity, bearing fits, roundness, and straightness require controlled machining and inspection to ensure stable rotation, accurate assembly, and reliable performance.
Runout and Concentricity Control
For precision shafts, concentricity can typically be controlled within 0.01–0.03 mm, depending on geometry and setup. Controlled datums and machining sequences help keep bearing journals and stepped diameters aligned, reducing vibration and uneven loading.
Bearing Fits and Functional Diameters
Standard CNC turning can hold shaft diameters to around ±0.025 mm, while precision grinding can achieve ±0.002–±0.005 mm on suitable critical journals. This supports tighter bearing fits, accurate assembly, and more consistent rotational performance.
Straightness and Dimensional Stability
Long and slender shafts require careful support and a machining sequence to minimize deflection and distortion. For ground functional surfaces, roundness can reach 0.002 mm, with surface roughness of Ra 0.2–0.8 μm where geometry and material allow.
Why Choose DZ Making for Custom Machined Shafts?
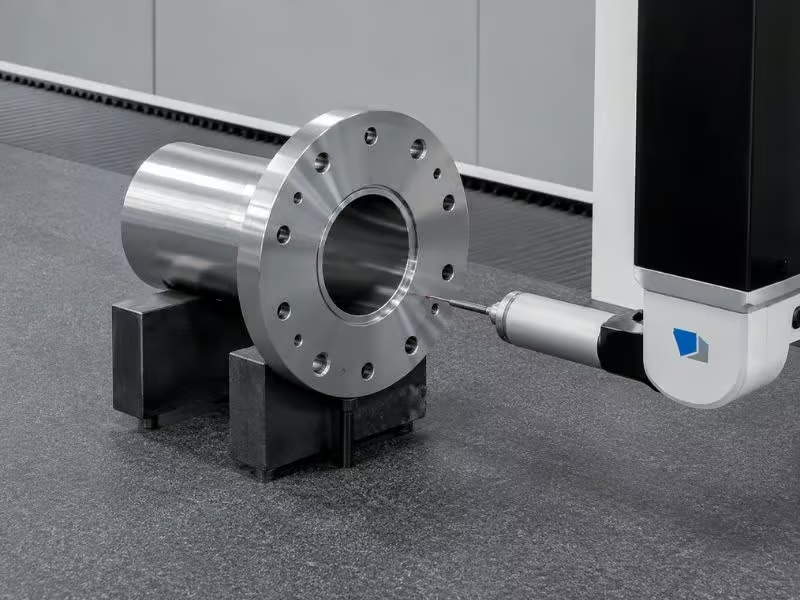
DZ Making inspects custom-machined shafts using micrometers, dial indicators, CMMs, thread gauges, and surface roughness testers in accordance with drawing requirements. Critical diameters, bearing journals, runout, concentricity, straightness, threads, and surface finish are checked before shipment to confirm fit, rotational accuracy, and dimensional compliance.


CNC Machining Processes for Precision Shafts
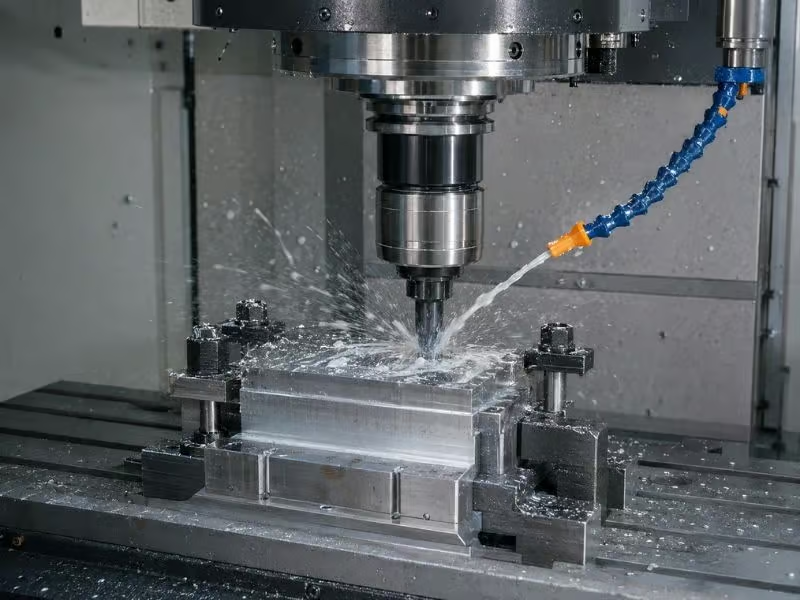
Precision shafts often require multiple machining processes to achieve the specified geometry, fits, and rotational accuracy. The process route depends on shaft length, diameter, material, feature complexity, tolerance, and surface requirements, with secondary operations added only where they improve functional performance.
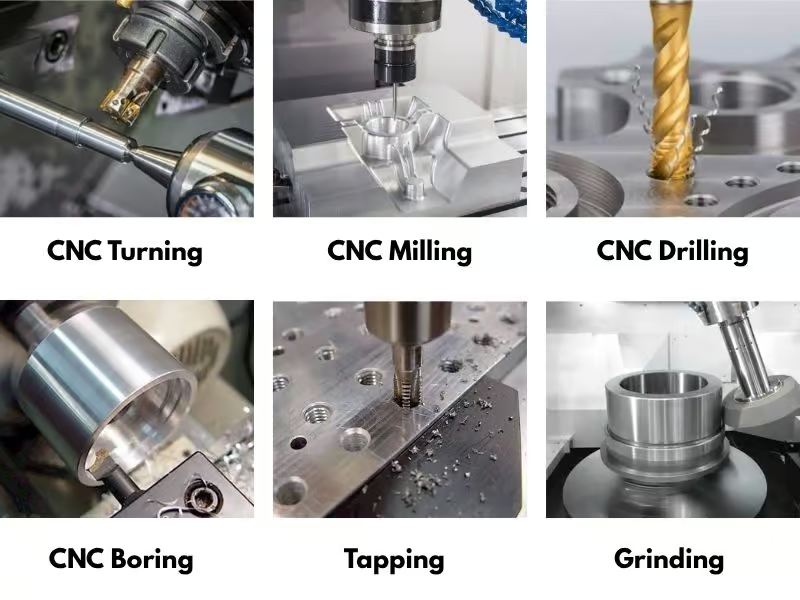
- CNC Turning: Produces stepped diameters, bearing journals, shoulders, tapers, grooves, and external threads.
- CNC Milling: Adds keyways, flats, slots, cross holes, and other non-rotational features.
- Precision Grinding: Finishes critical journals where tighter diameter control, roundness, or smoother surfaces are required.
- Drilling & Boring: Creates axial holes, internal bores, cross holes, and hollow shaft features.
- Thread Machining: Produces internal and external threads according to specified pitch, class, and fit requirements.
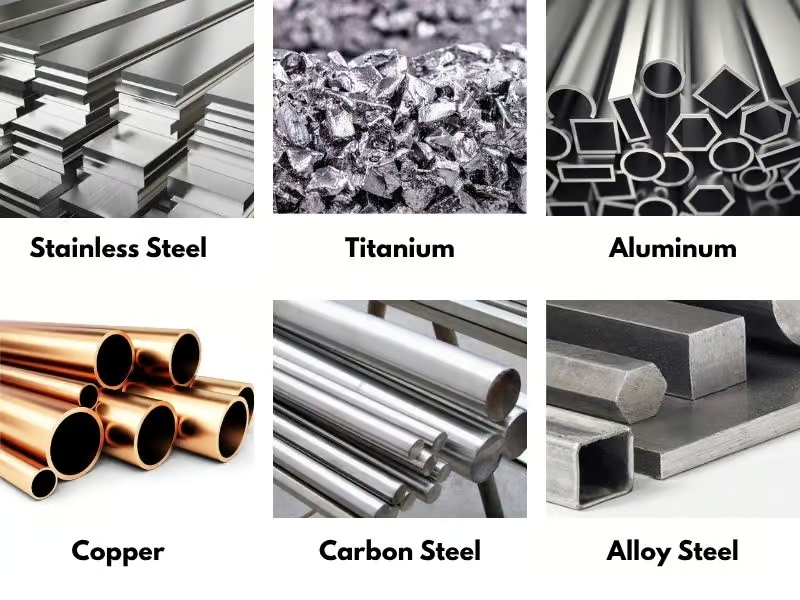
Materials for Custom Machined Shafts
We manufacture custom machined shafts from a wide range of metals and alloys. Material grades can be selected based on your required strength, wear resistance, corrosion resistance, weight, heat treatment, and operating conditions.
- Carbon Steel: Common grades include 1018, 1045, and 12L14, suitable for general mechanical shafts requiring good machinability, strength, and cost control.
- Alloy Steel: 4140, 4130, and 4340 are commonly selected for shafts requiring higher strength, toughness, fatigue resistance, or subsequent heat treatment.
- Stainless Steel: 303, 304, 316, and 17-4 PH provide different combinations of machinability, corrosion resistance, strength, and environmental durability.
- Aluminum: 6061 and 7075 are suitable for lightweight shafts where reduced mass, good machinability, and moderate to high strength are required.
- Titanium: Grade 2 and Grade 5 are available for applications requiring low weight, corrosion resistance, and a high strength-to-weight ratio.
- Copper Alloys: Brass, bronze, and C110 copper can be machined for specialized shafts requiring corrosion resistance, conductivity, or specific wear characteristics.
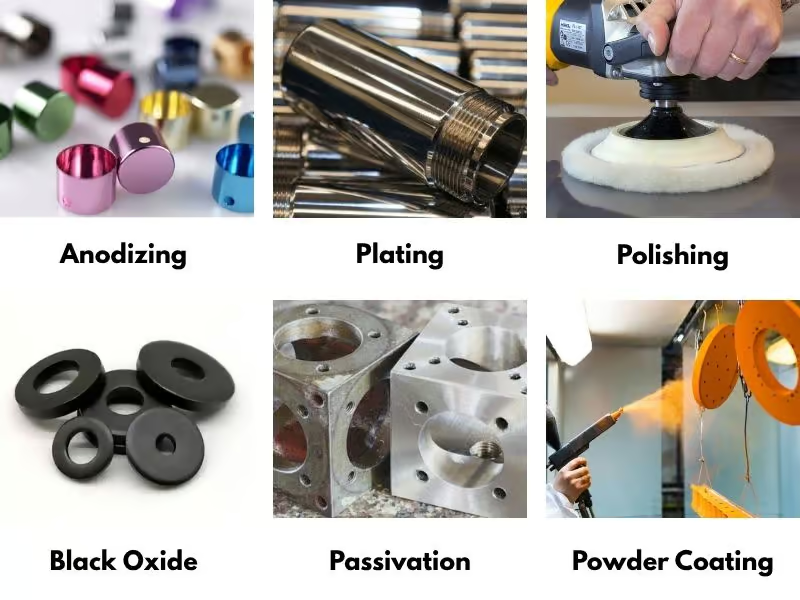
Surface Finishing for Machined Shafts
We offer multiple surface finishing options for custom machined shafts to improve corrosion resistance, wear performance, surface quality, and appearance. Your shaft material, working environment, mating conditions, and functional requirements help determine the most suitable finish.
- Plating: Zinc, nickel, and chrome plating improve corrosion resistance, wear resistance, and surface durability for steel and other metal shafts.
- Black Oxide: Provides basic corrosion protection for carbon and alloy steel shafts while causing minimal dimensional change.
- Anodizing: Type II and Type III anodizing improve corrosion resistance, surface hardness, and wear performance for aluminum shafts.
- Passivation: Improves the corrosion resistance and surface cleanliness of stainless steel shafts after machining.
- Polishing: Creates smoother bearing journals, seal-contact areas, and visible surfaces where lower roughness or improved appearance matters.
- Coating: PVD and other specialized coatings add hardness, wear resistance, or additional surface protection for demanding shaft applications.
What Our International Customers Say About DZ Making?
Customers across different industries trust DZ Making for reliable shaft machining, consistent dimensional accuracy, responsive technical communication, and stable quality from prototype development through repeat production.
DZ Making handled our CNC precision machining shaft project accurately, especially the bearing journals and critical diameters. The inspection results matched our specifications, and the finished shafts assembled smoothly without additional fitting, adjustment, or rework.

We ordered a machined gear shaft from DZ Making with stepped diameters, key features, and tight positional requirements. The batch showed good dimensional consistency, and our repeat order maintained the same reliable fit, accuracy, and machining quality.

DZ Making communicated clearly throughout the prototype stage and identified machining concerns before production. Their technical feedback helped us finalize the shaft design efficiently, and the approved samples transitioned smoothly into our subsequent low-volume production order.

How Does Shaft Surface Quality Affect Sealing and Friction?
Surface quality directly influences how shafts interact with seals, bearings, bushings, and other mating components. Controlling roughness, edge condition, and contact-surface consistency helps reduce leakage, friction, premature wear, and assembly problems during long-term operation.
01
02
03
FAQs
What information do you need to quote a custom machined shaft?
Please send your 2D drawing and, if available, a 3D CAD model together with the material, quantity, tolerances, surface finish, heat treatment, and inspection requirements. Clear notes for bearing journals, fits, runout, and other critical features help us provide a more accurate quotation.
Tolerance capability varies with shaft geometry, material, length, and machining process. CNC turning can typically hold around ±0.025 mm, while precision grinding can achieve approximately ±0.002–±0.005 mm on suitable critical diameters. Tighter GD&T requirements should be reviewed from the drawing before production.
Yes. We review datum relationships, bearing journals, stepped diameters, and other rotating features when planning the machining sequence. Concentricity can typically reach 0.01–0.03 mm, depending on part geometry and setup, while specific runout requirements are confirmed according to the drawing.
Yes. DZ Making supports prototype, low-volume, and repeat production for custom shafts. Prototype parts can help verify fit, functional dimensions, and assembly performance before you approve a larger production order.
Yes. CNC shaft machining can combine turning with milling, drilling, threading, and other secondary operations to produce stepped diameters, keyways, flats, grooves, cross holes, bores, and threaded features according to your drawing.
Applications of Custom Machined Shafts
Custom machined shafts support industries that require controlled rotation, torque transmission, positioning, or linear motion. Each application places different demands on shaft strength, bearing fits, runout, surface condition, corrosion resistance, and dimensional stability, so shaft design and machining should follow the actual operating conditions.
Automotive and Electric Vehicles
In automotive and EV systems, motor shafts, drive shafts, and gear shafts support electric drive units, transmissions, and actuator assemblies. These precision auto parts require accurate bearing journals, controlled runout, and reliable torque-transfer features to maintain stable rotation, efficient power transmission, and consistent performance under repeated loads.
Industrial Machinery
Stepped shafts, spindle shafts, and keyed shafts are common in gearboxes, conveyors, machine tools, and other rotating equipment. Consistent diameters, shoulder positions, and feature alignment help these machined components assemble correctly, maintain accurate motion, and withstand continuous mechanical loads throughout demanding industrial operating cycles.
Robotics and Automation
For robotics and automated equipment, linear motion shafts, motor shafts, and hollow shafts support positioning, actuation, and rotary movement. Precision robotics components need controlled concentricity, reliable bearing fits, and accurate feature locations to achieve repeatable motion and stable interaction with motors, encoders, guides, and transmission mechanisms.
Pumps and Fluid Equipment
Pump shafts, drive shafts, and rotor shafts connect motors, impellers, bearings, and sealing components in fluid-handling equipment. Good straightness, controlled runout, corrosion resistance, and smooth seal-contact surfaces help reduce leakage, vibration, uneven bearing loads, and premature wear during extended operation.
What Makes Long and Slender Shaft Machining Difficult?
Long and slender shafts create challenges beyond basic dimensional tolerance. Their low rigidity makes cutting more sensitive, while extended machining lengths increase the difficulty of workholding, surface consistency, datum control, and final inspection. Each factor requires a different approach during process planning.
Deflection and Chatter During Cutting
A slender shaft has lower rigidity than a short, thick component, so cutting forces can push it away from the tool or trigger vibration. Controlled cutting parameters, sharp tooling, appropriate support, and balanced stock removal help reduce taper, chatter marks, and dimensional variation during long shaft CNC turning.
Workholding and Datum Control
Long shafts often require chucks, centers, tailstocks, or steady rests to maintain support throughout machining. Poor locating or excessive clamping force can shift the machining axis and increase runout. A stable datum strategy helps keep bearing journals, shoulders, and other critical diameters correctly aligned.
Diameter and Surface Consistency
Maintaining the same diameter and surface condition over a long machining length is more difficult than finishing a short journal. Tool wear, vibration, cutting conditions, and multiple passes can create size or roughness variation, so critical surfaces may require staged finishing or precision grinding.
What Affects the Cost and Lead Time of Custom Machined Shafts?
The cost and lead time of custom machined shafts reflect more than overall diameter and length. An experienced machined shaft manufacturer evaluates feature complexity, tolerance requirements, material availability, secondary operations, inspection scope, and order quantity before defining the manufacturing route and delivery schedule.
- Shaft Size and Geometry: Long shafts, large diameters, stepped profiles, deep bores, keyways, grooves, splines, and cross holes require additional machining time, setups, or specialized workholding.
- Tolerance and GD&T: Tight bearing fits, low runout, concentricity, straightness, and fine surface requirements may require more controlled setups, intermediate inspection, or precision grinding, increasing both production time and cost.
- Material and Heat Treatment: Common steels and aluminum grades are usually easier to source, while special alloys can extend material lead time. Hardening, nitriding, carburizing, or other heat treatments also add processing steps.
- Secondary Machining and Finishing: Projects that combine CNC turning with milling, grinding, plating, polishing, or other finishing processes require additional handling and scheduling. Heat-treated shafts may also need final grinding to restore critical dimensions.
- Order Quantity and Inspection: Prototype quantities carry a higher setup cost per part, while repeat orders can distribute setup time across larger batches. Full dimensional reports, material certificates, hardness testing, or special inspection requirements can also affect the final quotation and delivery schedule.
