
Fabrication and Welding Services
DZ Making provides professional fabrication and welding services for metal parts, structures, and assemblies. We combine flexible manufacturing capabilities with precise process control to deliver reliable components that meet your dimensional, structural, and production requirements.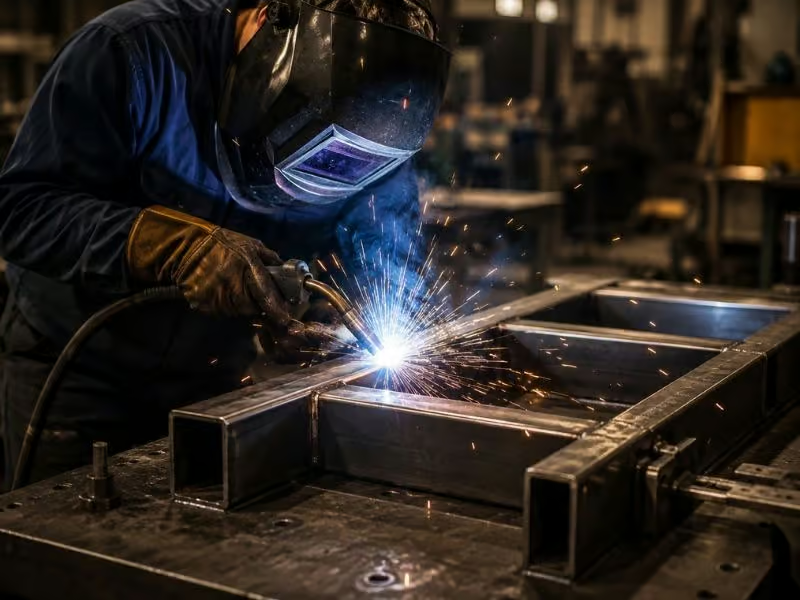
Technical Specifications for Fabrication and Welding Services
| Parameter | Capability |
|---|---|
| Welding Processes | MIG, TIG, Stick, Orbital, Laser |
| Fabrication Processes | Cutting, bending, forming, drilling |
| Materials | Carbon steel, stainless steel, aluminum, alloy steel |
| Part Forms | Sheet, plate, angle, channel, beam, tube, pipe |
| Fabrication Tolerance | Typically ±0.5–1.0 mm |
| Large Structure Tolerance | Typically ±1–3 mm |
| Surface Finishing | Coating, plating, anodizing, polishing, blasting |
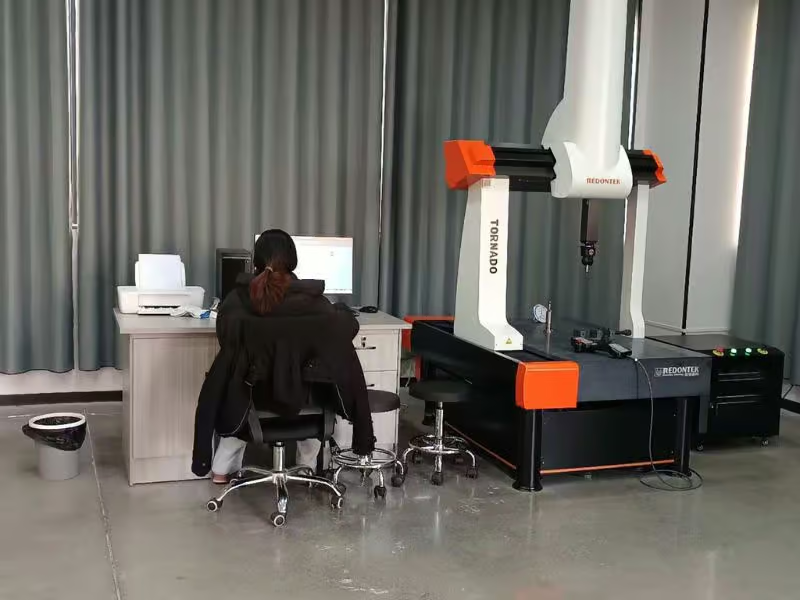
| Inspection | Dimensional, weld, and final inspection |
| Production Volume | Prototype to repeat production |
| File Formats | 2D drawings and 3D CAD files |
Fabricated and Welded Metal Components
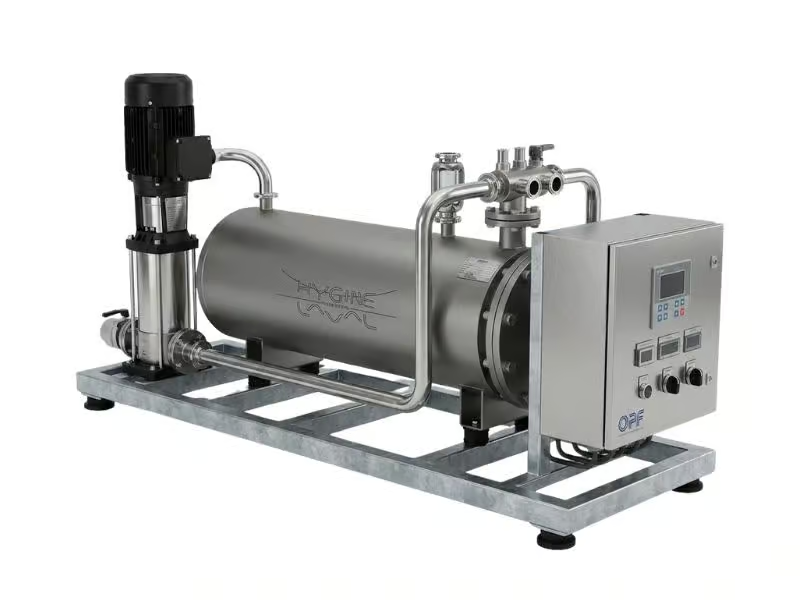
Heat Exchanger Components
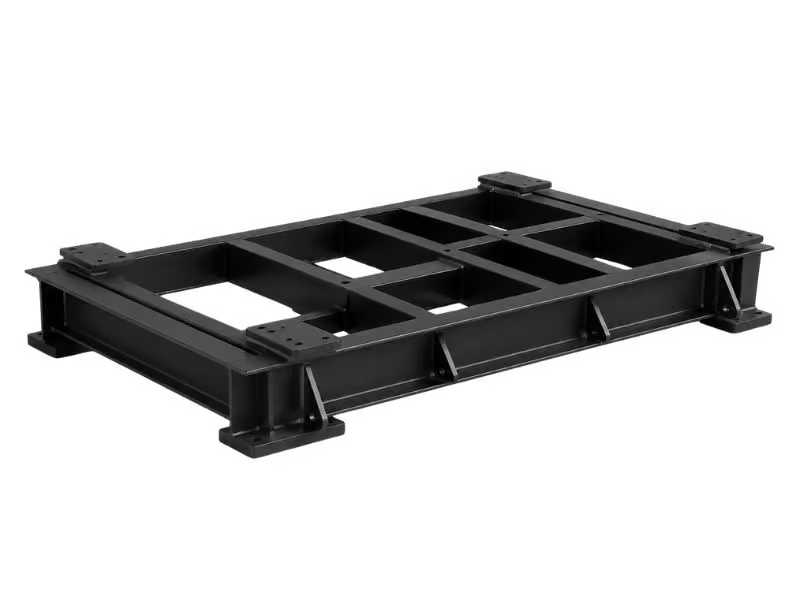
Structural Skid Bases
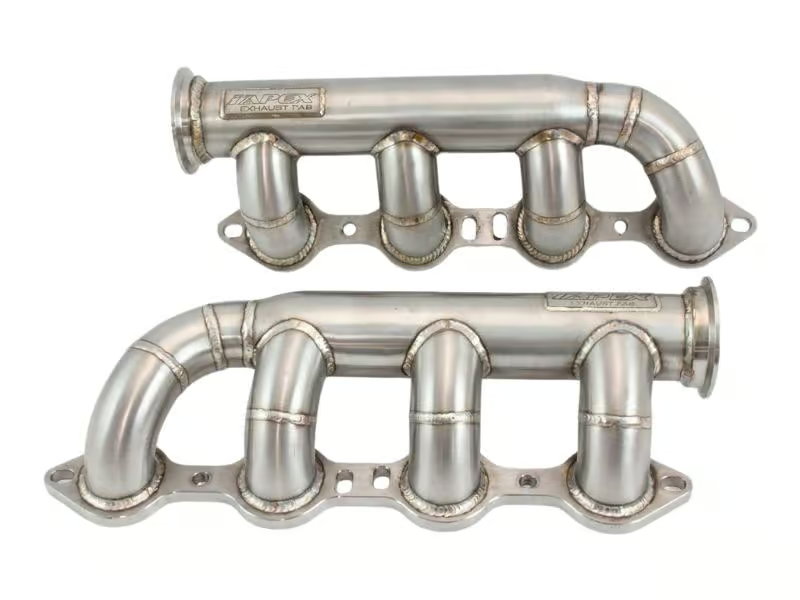
Welded Manifolds
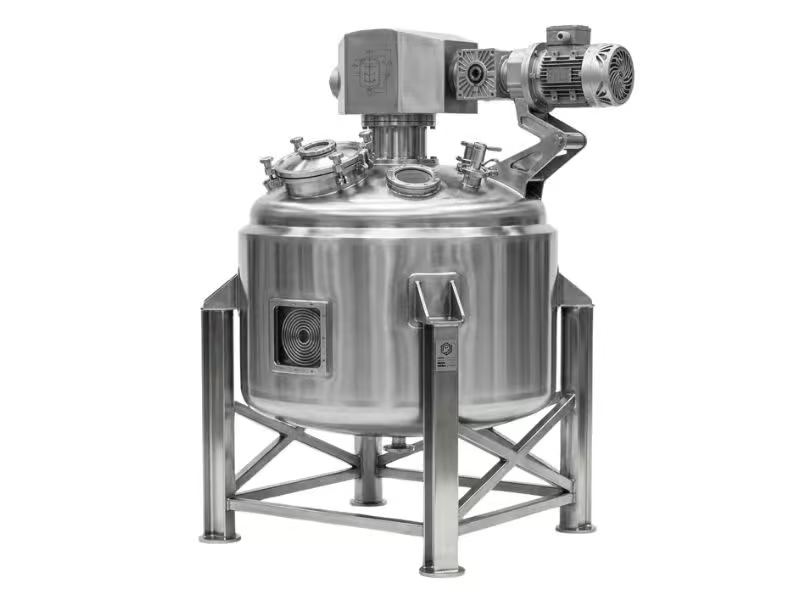
Industrial Process Tanks
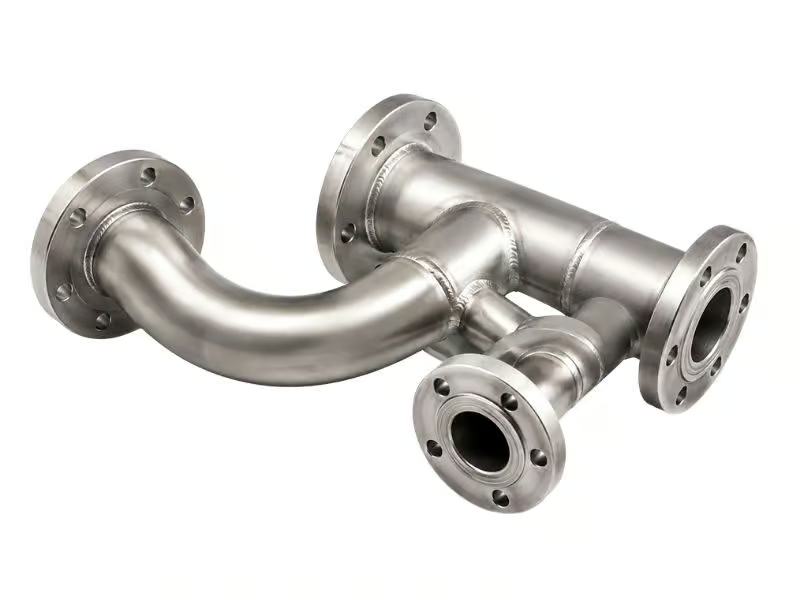
Industrial Pipe Spools
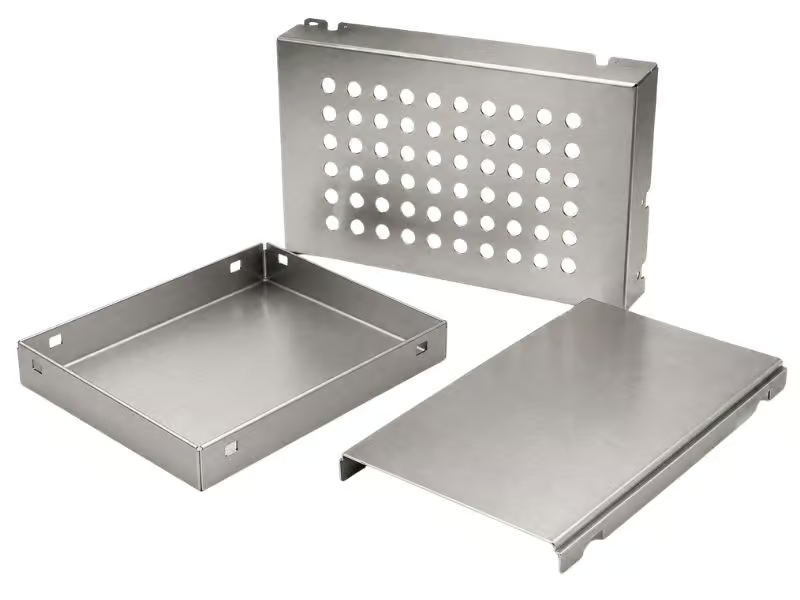
Sheet Metal Enclosures
Start Your Fabrication and Welding Project at DZ Making
Key Benefits of Fabrication and Welding
Fabrication and welding offer a practical way to create strong, complex, and large metal structures while balancing structural performance, design flexibility, and production efficiency.
Strong Structures
Fabrication and welding join multiple metal sections into rigid structures, distributing loads effectively while maintaining strength for frames, bases, supports, and other load-bearing components in service.
Flexible Geometry
Separate sections can be cut, formed, positioned, and joined into complex shapes that would be difficult or inefficient to produce from a single piece of material while maintaining practical manufacturing flexibility.
Efficient Large Parts
Building large components from plates, tubes, beams, and sections avoids excessive stock removal, reduces material waste, and provides a practical route for structurally complex parts.
How DZ Making Controls Fabrication and Welding Quality?
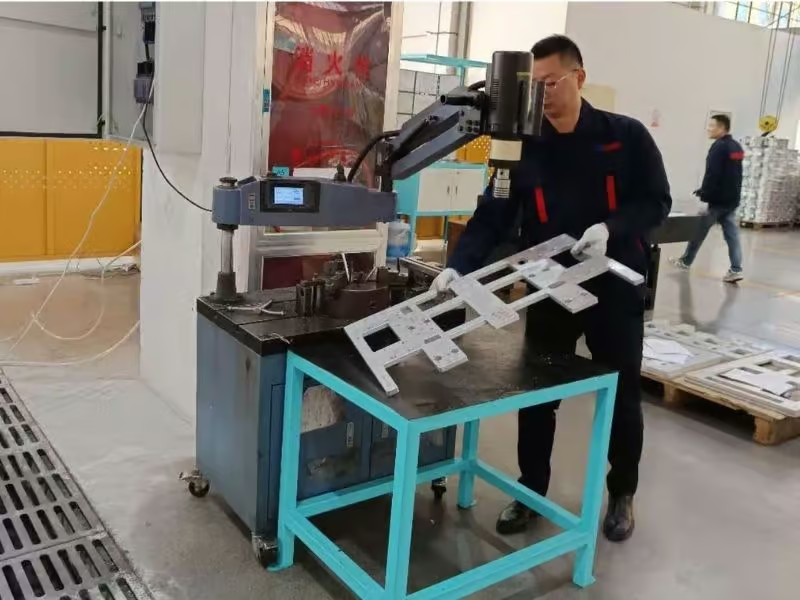
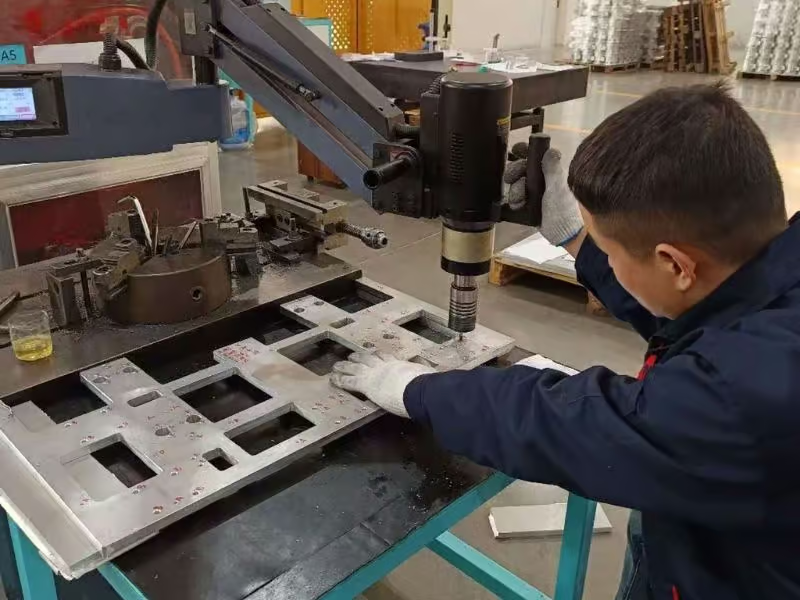
DZ Making controls quality through drawing review, material verification, fit-up checks, welding sequence control, and in-process dimensional inspection. Critical dimensions, joint alignment, weld condition, and surface quality are verified again before shipment to reduce distortion, misalignment, defects, and assembly-related rework.
Welding Options for Different Joint Requirements
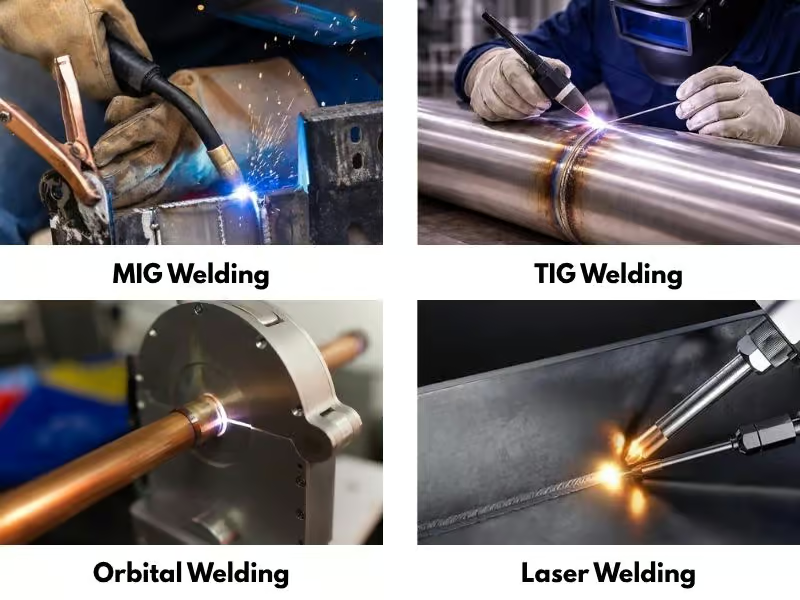
DZ Making supports multiple welding processes to match different materials, joint designs, thicknesses, and production requirements. The welding method is selected according to heat input, penetration, accessibility, appearance, and dimensional control rather than using one process for every fabricated component.
- MIG Welding: Suitable for efficient welding of steel and general fabricated structures.
- TIG Welding: Provides greater heat control for stainless steel, aluminum, thin sections, and cleaner visible joints.
- Orbital Welding: Supports repeatable circumferential welds on suitable tubes and pipes.
- Stick Welding: Well suited to thicker sections and structural fabrication where strong joints are required.
- Laser Welding: Enables narrow, controlled welds with limited heat input for suitable precision components.
Metal Fabrication Processes
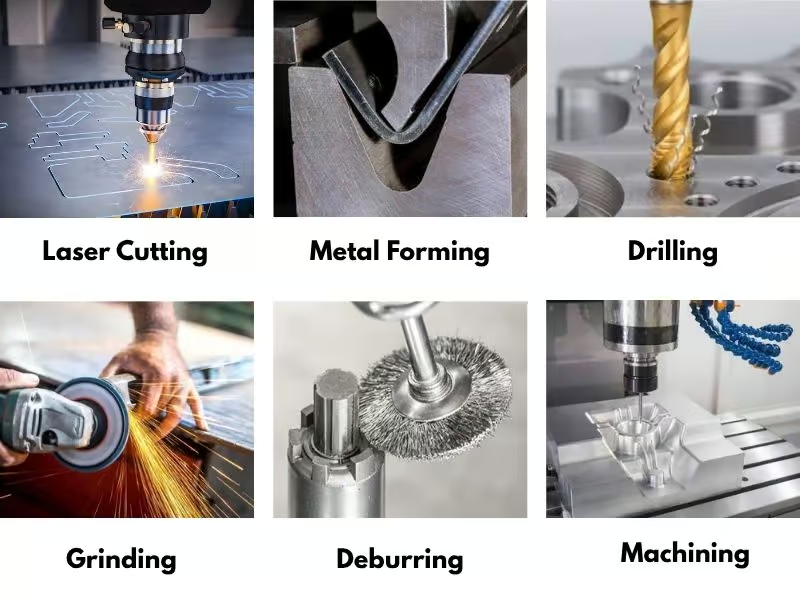
Our fabrication capabilities cover the operations required to turn sheet, plate, tube, pipe, and structural sections into production-ready components. Individual processes can be combined according to part geometry, assembly requirements, tolerance needs, and the welding sequence specified for the finished structure.
- Laser Cutting: Produces profiles, openings, slots, and blanks from sheet and plate.
- Metal Forming & Bending: Creates angles, flanges, channels, panels, and formed structural features.
- Drilling & Hole Making: Adds mounting holes, clearance holes, and other assembly features.
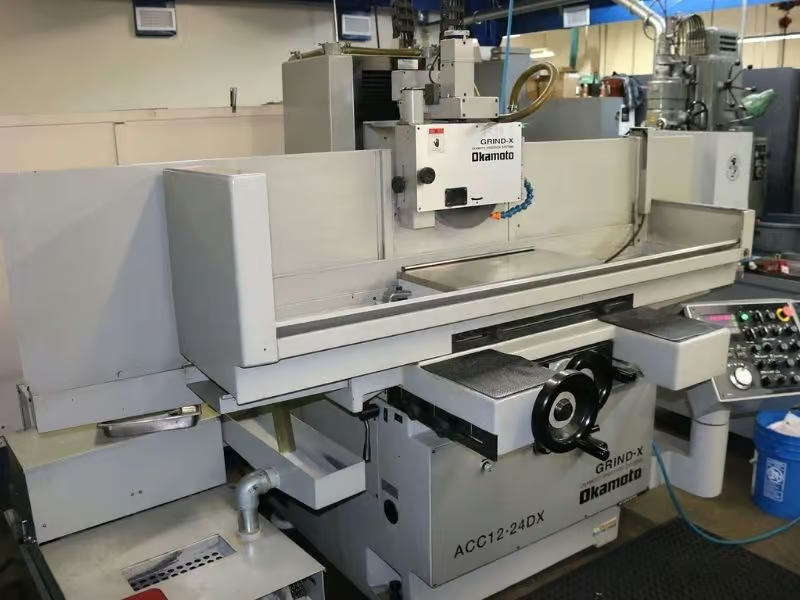
- Grinding & Deburring: Removes sharp edges, burrs, weld excess, and surface irregularities.
- CNC Machining: Finishes critical faces, bores, holes, threads, and mating features where tighter accuracy is required.
Metals for Fabrication and Welding
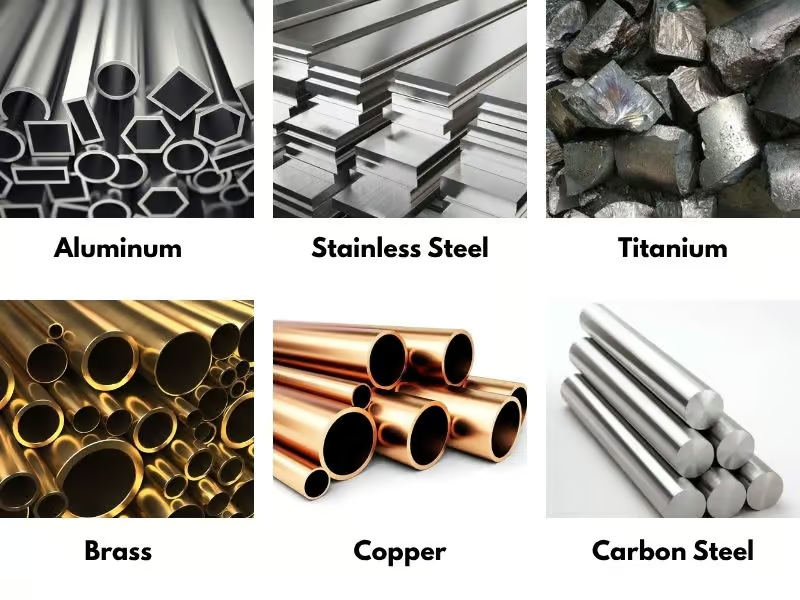
Material choice affects formability, weldability, strength, corrosion resistance, heat distortion, and finishing requirements. DZ Making works with commonly specified engineering metals and can match the material grade and form to the structural, environmental, and manufacturing needs of your project.
- Carbon Steel: Commonly used for frames, bases, supports, and general structural components.
- Stainless Steel: Suitable for corrosion-resistant enclosures, piping, process equipment, and exposed structures.
- Aluminum: Offers lower weight and good corrosion resistance for fabricated panels, frames, and assemblies.
- Copper & Copper Alloys: Applied where electrical conductivity, thermal performance, or corrosion resistance is required, with fabrication methods selected by alloy grade.
- Nickel Alloys: Suitable for demanding environments involving heat, corrosion, chemicals, or aggressive service conditions.
- Titanium: Used for lightweight, corrosion-resistant components where high strength-to-weight ratio and controlled welding conditions are important.
Surface Finishing for Fabricated Metal Parts
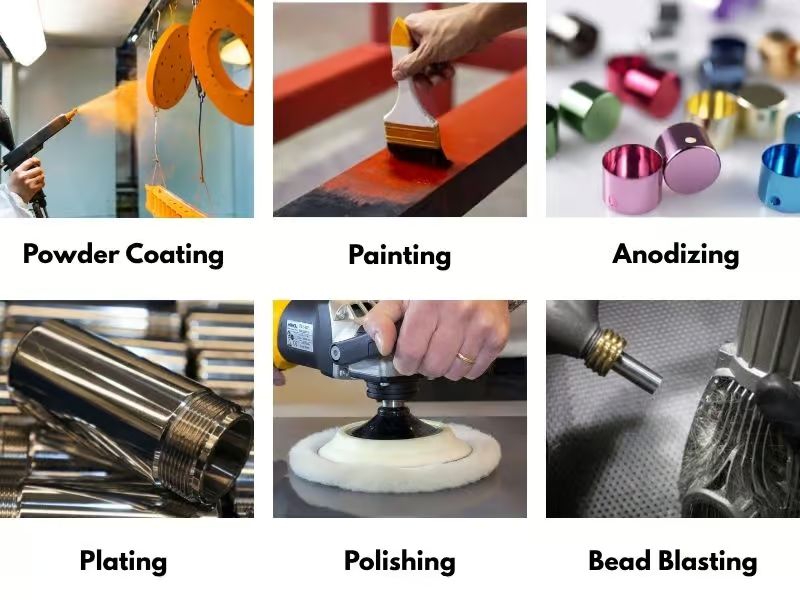
Surface finishing can be applied after fabrication and welding to improve corrosion resistance, appearance, cleanliness, or wear performance. The appropriate finish depends on the base material, service environment, dimensional requirements, and whether welded areas require grinding, polishing, or preparation before coating.
- Powder Coating: Provides a durable protective and decorative coating for steel components.
- Painting: Suitable for corrosion protection and color requirements on fabricated structures.
- Anodizing: Adds a protective oxide layer to suitable aluminum components.
- Plating: Options such as zinc plating can improve corrosion resistance on compatible metal parts.
- Polishing & Brushing: Improves the appearance and surface condition of stainless steel and other suitable metals.
- Bead Blasting: Creates a more uniform surface texture and prepares parts for subsequent finishing.
What International Customers Say About DZ Making?
Feedback from overseas customers highlights our consistent weld quality, dimensional control, and reliable fabrication results across different materials, part geometries, and production requirements.
DZ Making’s welding services gave us consistent joint quality across repeated batches. The welds were clean, dimensions stayed within our drawing requirements, and the parts arrived ready for assembly with minimal rework on our side.

We chose DZ Making for metal fabrication services because the fit-up and dimensional control were reliable from the first batch. Cut features, formed sections, and mounting points matched our drawings well, which made final assembly much easier.

The aluminum welding services were especially helpful on our lightweight assemblies. DZ Making controlled heat distortion well, kept the welds neat, and maintained the critical geometry we needed, reducing adjustment work during installation and final assembly.

Custom Welding and Fabrication Services Across Demanding Industries
DZ Making supports fabrication and welding projects for robotics, mobile equipment, and aerospace applications where structural integrity, dimensional accuracy, and reliable joint performance are critical.
01
02
03
FAQs
Can critical dimensions be machined after welding?
Yes. Mounting faces, bores, locating holes, threads, and other precision features can be CNC machined after the fabricated structure is welded. This is often preferable when welding heat could affect the final position or alignment of critical features.
Packaging is selected according to part size, weight, surface finish, and risk of movement or impact during transport. Finished components can be protected with wrapping, separators, reinforced cartons, pallets, or wooden cases where appropriate to reduce handling and shipping damage.
Distortion is managed through joint planning, controlled fit-up, appropriate restraint, welding sequence, heat-input management, and consideration of the structure’s stiffness. For features requiring tighter dimensional control, final machining can be performed after welding rather than relying entirely on pre-weld geometry.
Please provide your 2D drawings or 3D models, material grade, quantity, dimensional tolerances, welding requirements, surface finish, and any inspection or documentation requirements. For welded assemblies, identifying critical mounting surfaces and functional dimensions also helps us review the project more accurately.
Avoiding unnecessary weld length, unrealistic tolerances, excessive finishing, difficult-to-access joints, and overly complex component geometry can reduce manufacturing effort. Standard material sizes and practical joint designs can also improve production efficiency without compromising function.
For general fabricated and welded parts, we typically maintain ±0.5–1.0 mm on smaller dimensions and ±1–3 mm on larger structures, depending on part size, material thickness, joint layout, and heat input. Critical mounting faces, bores, and locating features can be CNC machined after welding to achieve ±0.02–0.05 mm where the geometry allows.
What Is the Difference Between Metal Fabrication and Welding?
Metal fabrication is the broader manufacturing process used to turn raw metal into finished parts or structures, while welding is a joining process used to connect separate metal components. Fabrication can include cutting, bending, forming, drilling, machining, and assembly. Welding is often one stage within that larger process.
In a typical fabrication and welding project, sheet, plate, tube, channel, or structural sections are first cut and formed to the required geometry. The prepared components are then fitted and welded together, followed by grinding, machining, surface finishing, or inspection when needed. This sequence means the accuracy of fabrication directly affects weld fit-up and final assembly quality.
The two processes therefore need to be planned together. Poor cutting, bending, or hole positioning can create alignment problems before welding begins, while uncontrolled heat input can introduce distortion into accurately fabricated parts. Effective metal fabrication and welding require coordinated control of geometry, joint preparation, fit-up, welding sequence, and final dimensions.
Key Design Considerations for Fabricated and Welded Parts
Good design for fabricated and welded parts should account for material behavior, joint geometry, fit-up, and heat-related distortion before production begins. These factors directly affect manufacturability, weld consistency, dimensional accuracy, and the amount of rework required after assembly.
- Material and Thickness: Material grade, section type, and thickness influence formability, weldability, heat input, and distortion. Thin sheet and heavy plate require very different fabrication and welding strategies.
- Joint Design and Accessibility: Butt, lap, corner, and T-joints should provide enough access for welding, inspection, and finishing while supporting the required load and assembly conditions.
- Fit-Up and Fixturing: Accurate gaps, alignment, locating features, and fixture points help keep components in position before and during welding, reducing cumulative dimensional errors.
- Distortion and Machining Allowance: Welding heat can affect flatness, squareness, and hole positions. Critical mating surfaces or bores may need machining allowance for final CNC finishing after welding.
How DZ Making Maintains Dimensional Stability in Fabricated and Welded Parts?
Dimensional stability is managed by planning the manufacturing sequence around heat movement, structural stiffness, and final datum requirements. DZ Making reduces deformation by controlling when parts are formed, joined, stress-relieved, and finish-machined, helping critical interfaces remain stable after the welded structure is completed.
- Sequence Planning: Cutting, forming, welding, and machining are arranged in an order that limits accumulated deformation and avoids locking dimensional error into the structure.
- Distortion Compensation: For structures prone to shrinkage or warping, allowances can be built into forming, joint layout, or pre-set geometry so the finished part moves closer to its intended dimensions after welding.
- Structural Stiffness Management: Temporary supports, stiffeners, or controlled restraint can be used on larger frames and plate structures to reduce movement during heating and cooling.
- Final Datum Machining: Critical mounting faces, bores, and locating features can be machined after welding, allowing final dimensions to reference the completed structure rather than relying on pre-weld geometry.
