
CNC machining becomes much more demanding when a material combines high hardness, poor thermal conductivity, work hardening, toughness, or abrasive behavior. Titanium alloys, nickel-based superalloys, hardened steels, tungsten alloys, and advanced ceramics can shorten tool life, raise cutting temperatures, and make dimensional control more difficult.
The hardest materials to CNC machine are not simply the materials with the highest hardness values. This article explains which materials create the greatest machining challenges, why they are difficult to cut, which strategies help control those problems, and how material difficulty affects cost and process selection.
What Does Material Hardness Mean in CNC Machining?
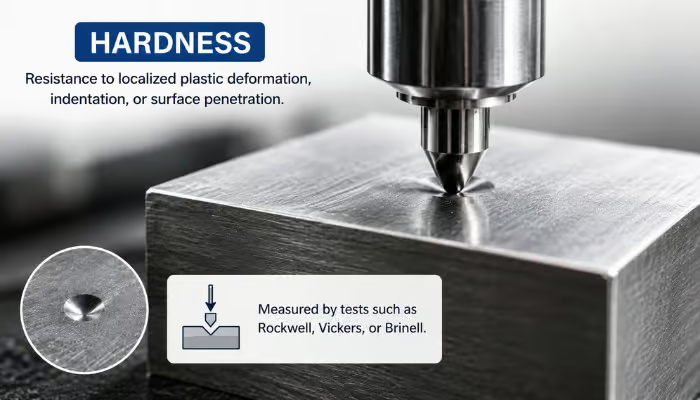
In CNC machining, material hardness describes a material’s resistance to localized plastic deformation, indentation, or surface penetration. Rockwell, Vickers, and Brinell tests are common ways to measure this property. Each test uses a defined indenter, load, and measurement method, so hardness values should always be interpreted together with the test scale.
Hardness is different from strength. Strength describes how much stress a material can withstand before it yields or fails, while hardness focuses on resistance to localized deformation. A material can have high strength without having the highest hardness, and the reverse can also be true. ASM International treats hardness as one indicator related to properties such as wear resistance, tensile strength, and machinability rather than a complete measure of material behavior.
Factors That Make a Material Difficult to Machine
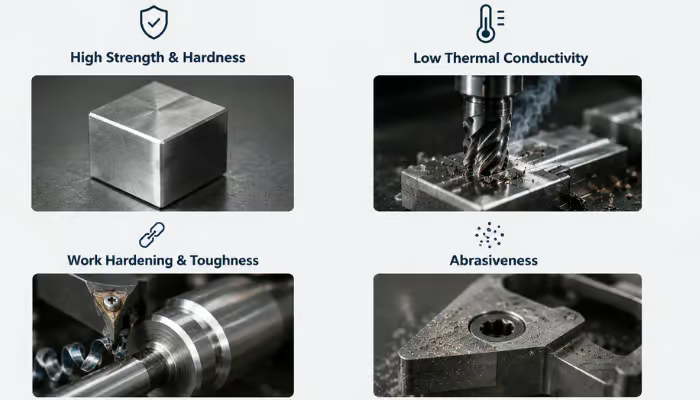
Material machinability depends on how the workpiece responds to cutting force, deformation, heat, and tool contact. No single property determines whether a material is easy or difficult to machine. Hardness, strength, toughness, work hardening behavior, abrasiveness, and thermal properties often interact to define the overall machining difficulty.
Hardness, Strength, and Abrasiveness
High hardness increases resistance to cutting edge penetration, while high strength raises the force needed to deform and shear the material. Together, hardness and strength increase cutting resistance, while abrasiveness adds continuous wear at the cutting edge. This combination increases mechanical load on the tool and can accelerate flank wear, edge chipping, and tool failure even when the overall material hardness is only moderate.
Toughness, Ductility, and Work Hardening
Tough and ductile materials resist fracture and undergo more deformation before the chip separates. This makes chip formation less controlled and can lead to long continuous chips, built-up edge, and higher cutting forces. Some alloys also harden as they deform during cutting. If the next pass enters this hardened layer, cutting resistance rises further, and the tool has to remove material that is harder than the original surface. Stainless steels and nickel-based superalloys are typical examples.
Thermal Conductivity and Heat Buildup
Low thermal conductivity slows the transfer of cutting heat away from the cutting zone. As more heat stays concentrated near the cutting edge, temperature rises and increases the risk of coating damage, accelerated tool wear, and changes in surface integrity. Titanium and nickel-based superalloys are especially affected because they dissipate heat poorly while still resisting deformation at elevated temperatures.
7 of the Hardest Materials for CNC Machining
Some materials become especially difficult to machine because several demanding properties act together. The main challenge is controlling tool wear, cutting heat, chip formation, and dimensional accuracy while maintaining stable material removal. These challenges vary with each material’s hardness, strength, toughness, thermal behavior, and wear resistance.
Nickel-Based Superalloys
Nickel-based superalloys such as Inconel 718 retain high strength at temperatures where many conventional metals begin to soften. Inconel 718 also gains much of its strength from precipitation hardening and develops additional hardness when it deforms during cutting. The cutting edge must remove material that stays strong at high temperatures while the surface can harden further during deformation, which keeps cutting resistance high throughout the cut.
Low thermal conductivity adds another difficulty because heat does not dissipate efficiently away from the cutting zone. At elevated temperatures, nickel alloys can also interact strongly with tool materials, increasing adhesion and wear at the cutting interface. Retained strength, concentrated heat, and strong tool material interaction make cutting conditions harder to control than with conventional steels or aluminum.
Titanium Alloys
Titanium alloys combine high strength with poor heat conductivity and relatively low stiffness, which creates demanding cutting conditions. Ti 6Al 4V is one of the most widely used titanium grades and shows these characteristics clearly. Its thermal conductivity is about 6.92 W/m·K near room temperature, so heat tends to stay close to the cutting edge instead of dissipating quickly into the workpiece.
Its relatively low stiffness creates a second challenge in titanium machining. Thin walls and slender features can deflect under cutting force and spring back after the tool passes. With heat concentrated around the cutting edge and flexible features moving under load, maintaining stable cutting conditions and consistent dimensions becomes much more difficult.
Stainless Steels
High ductility, toughness, strong work hardening, and relatively low thermal conductivity make many stainless steels difficult to machine. Austenitic grades such as 304 and 316 deform substantially before fracture, so the material tends to stretch rather than separate cleanly at the cutting zone. This behavior promotes long continuous chips and a built-up edge, while repeated plastic deformation can harden the machined surface and increase cutting resistance. Low thermal conductivity then keeps more heat near the cutting zone, making stainless steel CNC machining more demanding in terms of chip control, heat, and tool stability.
Hardened Steels and Tool Steels
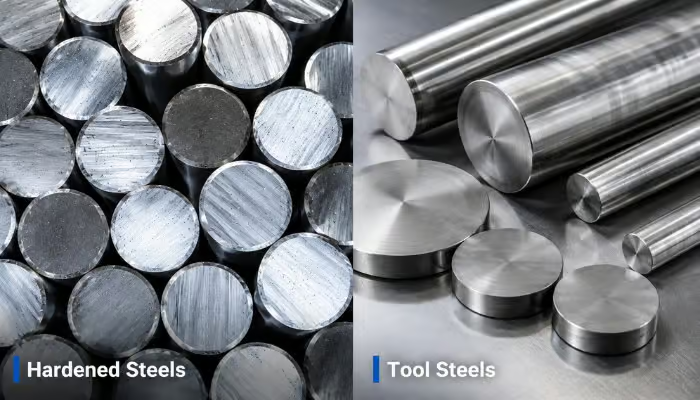
Heat treatment can bring some tool steels to 60 HRC or higher, which sharply reduces their ability to deform under the cutting edge. The material therefore resists penetration and chip formation much more strongly than softer steels. This higher resistance increases the mechanical load at the cutting zone and makes material removal more difficult.
Tool steels can become even more difficult because chromium, vanadium, tungsten, or molybdenum may form very hard carbide phases within the steel matrix. The cutting edge repeatedly crosses material regions with different hardness, which creates uneven resistance and strongly abrasive cutting conditions. This makes their machining behavior more severe than hardness value alone would suggest.
Tungsten and Tungsten Alloys
Pure tungsten combines very high hardness, stiffness, density, and melting temperature with limited ductility at room temperature. This means the material does not shear as smoothly as more ductile metals and can fracture locally under concentrated cutting stress. Edges, thin sections, and small features are therefore more vulnerable to chipping during material removal.
Tungsten heavy alloys behave differently because hard tungsten particles are bonded within a softer metallic matrix. The softer binder improves toughness, but the cutting edge repeatedly moves between hard tungsten particles and the softer binder during material removal. The difference in hardness causes local changes in cutting resistance, while tungsten particles may fracture or pull away from the matrix, making it more difficult to produce a smooth and consistent machined surface.
Cobalt-Based Superalloys
Cobalt-based superalloys retain high strength at elevated temperatures and often contain hard carbide phases within a tough metal matrix. Stellite is a well-known family within this material group. During machining, the tough matrix resists deformation while the harder carbide regions create sudden changes in local cutting resistance.
This mixed structure prevents the cutting edge from seeing a uniform material response. Chip formation becomes less consistent, and cutting resistance changes as the tool moves through different phases. The difficulty comes from the combination of toughness and localized hardness rather than from bulk hardness alone. The difficulty comes from the combination of toughness and localized hardness rather than from bulk hardness alone.
Advanced Ceramics
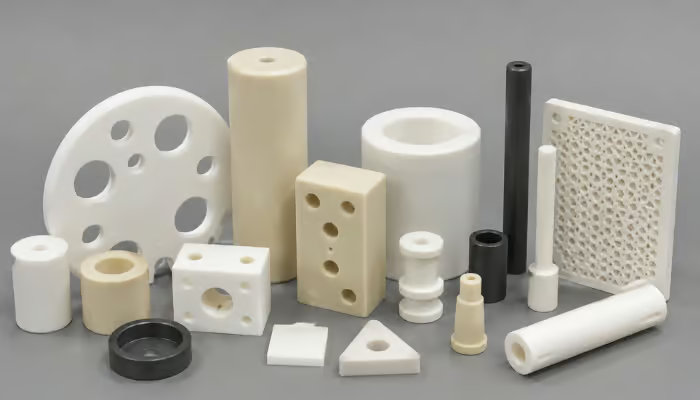
Advanced ceramics such as alumina, silicon carbide, and silicon nitride differ fundamentally from metallic hard-to-machine materials. Their extreme hardness and wear resistance come from strong atomic bonding, but they have very limited ductility. Instead of plastically deforming under cutting forces, ceramics tend to fracture once local stresses exceed their fracture strength.
This brittle behavior makes dimensional control especially difficult around holes, edges, thin walls, and small features. Microcracks can develop below the visible surface even when the external geometry appears acceptable, while larger cracks can propagate suddenly through the part. Silicon carbide and alumina are also highly abrasive, so machining involves both extreme hardness and fracture-sensitive material removal rather than conventional chip formation.
Comparison of Hard-to-Machine Materials
Hard-to-machine materials differ in heat behavior, work hardening, abrasiveness, cutting resistance, and fracture response. These differences change the way each material affects tool wear, cutting stability, surface quality, and dimensional control. A useful comparison should therefore focus on the dominant machining mechanisms rather than assigning one general difficulty rating to every material.
| Material | Heat control demand | Work hardening | Abrasive wear | Brittle fracture/chipping | Main machining concern |
| Nickel-based superalloys | High | High | Moderate | Low | High cutting resistance as temperature rises |
| Titanium alloys | High | Moderate | Low to moderate | Low | Heat concentration and elastic deflection |
| Stainless steels | Moderate to high | High | Moderate | Low | Work-hardened surface and difficult chip control |
| Hardened steels and tool steels | Moderate | Low | High | Moderate | High hardness and carbide abrasion |
| Tungsten and tungsten alloys | Moderate | Low | Moderate to high | High in pure tungsten | Local fracture and uneven cutting resistance |
| Cobalt-based superalloys | High | Moderate | High | Low to moderate | Tough matrix with hard carbide phases |
| Advanced ceramics | Low relevance | None | Very high | Very high | Brittle fracture and subsurface cracking |
Best Practices for Machining Difficult Materials
Machining difficult materials requires tighter control over the cutting process than conventional materials. Tool material, cutting parameters, heat control, and machining stability should work together rather than be treated as separate adjustments. A change in one area can affect cutting force, temperature, chip formation, and tool life across the whole operation.
Choose the Right Tool Materials
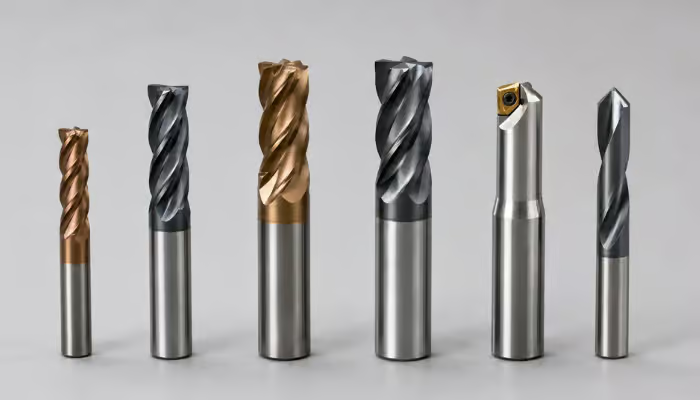
Tool material should match the hardness, abrasiveness, cutting temperature, and deformation behavior of the workpiece. Different difficult materials place very different demands on the cutting edge, so no single tool material works best across all applications.
- Carbide: Common for titanium, stainless steel, and many nickel-based alloys because it offers a useful balance of hardness, toughness, and heat resistance.
- CBN: Better suited to hardened steels and other ferrous materials at high hardness levels where carbide may wear too quickly.
- Ceramic: Useful for some nickel-based and cobalt-based superalloys where the cutting zone reaches very high temperatures.
- PCD: Mainly used for abrasive nonferrous materials and composites. It is generally unsuitable for ferrous alloys because diamond reacts with iron at elevated cutting temperatures.
Tool coatings also matter. TiAlN and AlTiN type coatings can improve hot hardness and oxidation resistance, while edge geometry must still provide enough toughness for interrupted cuts or variable engagement. The hardest tool material is not always the most reliable choice if the cutting condition is unstable.
Optimize Cutting Parameters
Cutting parameters determine the mechanical and thermal conditions at the cutting edge. For difficult materials, cutting speed, feed per tooth, axial depth of cut, and radial engagement should be balanced as a system rather than reduced independently. The suitable values depend on the material grade, tool material and geometry, machining operation, coolant condition, and machine rigidity.
- Cutting Speed (Vc): Use a more conservative surface speed when the material retains strength at elevated temperatures or conducts heat poorly. Titanium and nickel-based superalloys are especially sensitive because excessive speed can raise cutting temperature quickly and shorten the stable cutting window.
- Feed per Tooth (fz): Maintain enough chip thickness for the cutting edge to shear material cleanly instead of rubbing across the surface. Feed that is too light can increase rubbing and work hardening in stainless steels and nickel alloys, while excessive feed can overload the cutting edge.
- Axial Depth of Cut (ap): Avoid repeated shallow passes through the same affected surface layer. A sufficient and consistent axial depth can keep the tool cutting below work-hardened material and distribute cutting along more of the cutting edge.
- Radial Engagement (ae): Control the width of cut to keep cutting force and engagement more consistent during milling. Lower radial engagement can reduce peak load, while constant engagement toolpaths help prevent sudden increases in cutter contact through corners and pockets.
Control Cutting Heat
Heat control should focus on removing heat from the cutting zone before it accumulates around the tool and workpiece. For titanium and nickel-based superalloys, intermittent engagement can reduce continuous thermal loading, while toolpaths that avoid prolonged contact help prevent heat from concentrating at one cutting edge for too long.
Direct coolant precisely at the tool-chip interface rather than applying it broadly around the work area. High-pressure coolant can penetrate narrow cutting zones, improve chip evacuation, and carry heat away from the cutting edge more effectively. In deep pockets, grooves, and internal features, through-tool coolant or targeted nozzles usually provide better access than general flood coolant. Clear chip evacuation is also important because recutting hot chips adds heat and abrasive contact back into the process.
Improve Rigidity and Workholding Stability
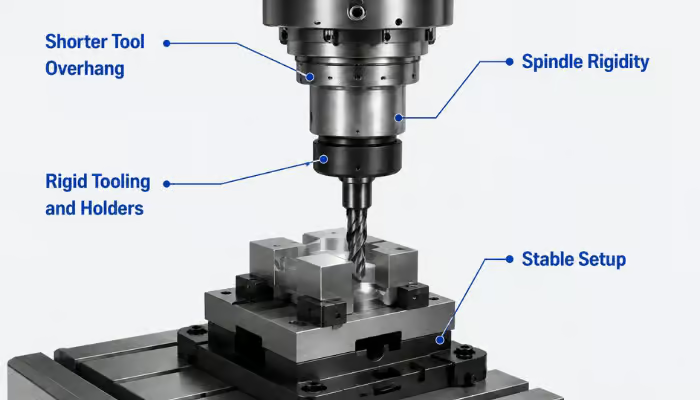
Rigidity becomes more critical as cutting forces rise, material response becomes less uniform, or the workpiece tends to spring back during cutting. Difficult materials can magnify small weaknesses in the tool, fixture, and part support, so stability should be planned around the specific source of force, deflection, or vibration.
- Reduce Tool Overhang: Use the shortest tool and holder combination that can reach the feature. High cutting resistance in hardened steels, tungsten alloys, and nickel alloys can amplify tool deflection, so deep features should be approached with longer tools only as additional reach becomes necessary.
- Support Flexible Features: Add support near thin walls, slender shafts, and other weak sections. Titanium is especially sensitive because its lower elastic modulus allows thin features to deflect under cutting force and spring back after the tool passes.
- Control Clamping Force: Apply enough force to prevent movement without distorting the workpiece. Thin sections and tough materials can carry substantial cutting load, but excessive clamping can introduce dimensional error before machining even begins.
- Place Support Near High Load Areas: Position fixture contact points close to features where cutting resistance is highest. This becomes important with hardened steels and tungsten alloys, where concentrated cutting forces can make unsupported sections vibrate or shift.
- Maintain Support as Material Is Removed: Leave temporary ribs, tabs, or surrounding stock in place during heavy roughing where possible. As material is removed, stiffness can drop quickly, especially on thin titanium parts or precision components with large pockets. Delaying removal of support features helps preserve rigidity until the highest cutting loads are finished.
How Does Material Difficulty Affect CNC Machining Cost?
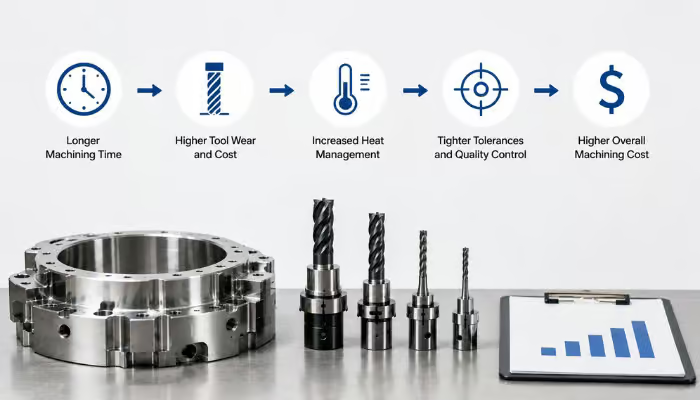
Difficult materials increase CNC machining cost mainly by slowing material removal, increasing tooling demand, adding process control, and raising scrap risk. The cost impact comes from the entire production route rather than the raw material price alone. Two parts with the same geometry can have very different machining costs if one material requires slower cutting, more tool changes, additional setups, or tighter inspection.
Tooling and Machining Time
Tooling cost rises when difficult materials shorten tool life or require more specialized cutting materials. Hardened steels may need CBN or coated carbide tools, while titanium and nickel alloys can consume inserts more quickly under high heat and cutting resistance. Machining time also increases when cutting speed, depth of cut, or tool engagement must be reduced to keep cutting stable. Difficult materials may require slower roughing, additional passes, or more controlled finishing before the part reaches final size. The longer the machine remains occupied by each part, the higher the machining cost becomes.
Setup and Quality Control
Setup cost comes from the extra preparation needed before stable cutting can begin. Higher cutting forces may require stronger fixtures, custom soft jaws, additional supports, or more rigid toolholding, while thin or flexible parts may need dedicated clamping methods to control distortion. Fixture preparation, alignment, tool presetting, and trial setup all add cost without contributing directly to material removal.
Quality control adds a separate layer of cost through measurement and process verification. Tool wear, heat, springback, or part deformation may require critical features to be checked between operations rather than only at final inspection. In process probing, CMM inspection, offset verification, and dimensional checks increase labor and inspection resource use, especially on tight tolerance parts.
Scrap and Production Risk
The cost impact becomes much larger when a machining error occurs late in the process. Difficult materials are often expensive in raw stock form, so a rejected part can create a large direct material loss. This is especially relevant for titanium, nickel alloys, tungsten, and other specialty materials with high stock value.
Late-stage defects also reduce the chance of recovery. Once a bore, thin wall, sealing surface, or tight tolerance feature reaches final size, there may be little or no material left for correction. Cracks, edge damage, dimensional oversize, or surface defects can therefore turn into full part rejection rather than rework. Higher scrap risk also increases replacement material demand, schedule uncertainty, and the chance that one rejected part disrupts a small batch or matched component set.
When Should Alternative Manufacturing Processes Be Considered?
Alternative processes become useful when conventional milling or turning cannot produce a feature efficiently or with acceptable risk. Extreme hardness, brittle behavior, complex geometry, tight surface requirements, or heavy material removal can make conventional cutting inefficient. EDM, grinding, waterjet cutting services, and additive manufacturing can replace specific operations or complement CNC machining.
EDM for Complex Hard Material Features

EDM removes conductive material through controlled electrical discharges rather than mechanical cutting. Because material removal does not rely on direct cutting force, hardness is far less limiting than in conventional milling or turning. This makes EDM particularly useful for hardened tool steels, tungsten alloys, and other conductive materials that are difficult to cut mechanically.
EDM becomes practical for deep narrow slots, small internal corners, intricate cavities, and features that would require very small or long reach cutting tools. Different types of EDM machining suit different feature requirements: wire EDM works well for through profiles and precision contours, while sinker EDM is better suited to blind cavities and complex internal forms. Its relatively slow removal rate means it is usually reserved for features where conventional cutting becomes inefficient rather than replacing CNC machining for the entire part.
Precision Finishing With Grinding

Grinding becomes a strong option when the material is already hardened, and the part requires tight dimensional control or a fine finished surface. Abrasive wheels remove very small amounts of material with controlled contact, which makes the process suitable for hardened steels, tool steels, carbide-related components, and many ceramics. Grinding is often used after rough machining to finish bores, shafts, flat surfaces, or other critical features where conventional cutting would struggle to maintain the required size or surface condition.
Waterjet Cutting for Initial Profiling

Waterjet cutting can remove large amounts of stock without creating a heat-affected zone, which makes it useful for rough profiling difficult materials before precision machining. Thick titanium plate, stainless steel, tool steel, and some composite materials can be cut close to the required outline first. CNC machining can then focus on holes, mating surfaces, tolerances, and detailed features instead of removing the entire stock volume. Waterjet therefore works best as a preparation process that brings the material close to its final shape rather than replacing precision machining.
Additive Manufacturing for Complex Geometries

Choose additive manufacturing when complex internal channels, lattice structures, or highly integrated shapes would require extensive material removal from solid stock. Metal additive processes can build parts close to their final shape from titanium, nickel alloys, and other difficult materials, which can reduce waste when conventional machining would remove a large amount of expensive stock. Critical surfaces, holes, threads, and tight tolerance features usually still require CNC machining after printing, so 3D printing and CNC machining often work together rather than serving as complete substitutes.
Partner with DZ Making for Hard Material Machining
Machining titanium, hardened steels, stainless steels, nickel alloys, and other difficult materials requires careful coordination between material properties, part geometry, tolerances, tooling, and machining strategy. DZ Making reviews these requirements before production to identify challenging features, potential deformation or tool access issues, and suitable machining processes for each part.
Our CNC machining capabilities support prototypes, low-volume parts, and repeat production with dimensional inspection based on drawing requirements. Send us your CAD files or technical drawings with the material grade, quantity, tolerances, surface finish, and inspection requirements. Our team can review your project and prepare a manufacturing plan and quote.
Conclusion
The hardest materials to CNC machine present different challenges depending on their hardness, strength, toughness, thermal behavior, abrasiveness, and tendency to work harden. Nickel-based superalloys, titanium, hardened steels, tungsten alloys, cobalt alloys, stainless steels, and advanced ceramics each require machining strategies suited to their specific material behavior.
Successful machining depends on matching tooling, cutting parameters, heat control, workholding, and process planning to the material and part requirements. When certain features are inefficient to produce with conventional cutting, EDM, grinding, waterjet cutting, or additive manufacturing can complement CNC machining. Material selection should therefore be evaluated together with part geometry, tolerance requirements, and the overall production route.
FAQs
1. What are the top 5 hardest materials to machine?
Five of the most difficult material groups to machine are nickel-based superalloys, titanium alloys, hardened steels, tungsten alloys, and advanced ceramics. Their machining difficulty comes from different combinations of hardness, heat concentration, work hardening, brittleness, and abrasive behavior rather than from hardness alone.
2. Is Inconel harder to machine than titanium?
In many applications, Inconel is considered more difficult to machine because it retains strength at high temperatures and work hardens rapidly during cutting. Titanium creates severe heat concentration and elastic deflection, but nickel-based superalloys often place greater combined demands on tool life, cutting force, and process stability.
3. Does higher hardness always mean poorer machinability?
No. Hardness is only one factor that affects machinability. A material with moderate hardness can still be difficult to machine if it has high toughness, low thermal conductivity, strong work hardening behavior, or abrasive phases. Stainless steel and titanium are common examples.
4. Can hardened steel be CNC machined?
Yes. Hardened steel can be CNC machined, although the suitable process depends on its hardness, geometry, tolerance, and surface requirements. Carbide and CBN tools are commonly used for hard turning or milling, while grinding may be more suitable for very hard materials or precision finishing.
5. Can CNC machines cut tungsten?
Yes, but tungsten grade and material condition matter. Pure tungsten can be brittle and difficult to cut without edge damage, while tungsten heavy alloys are generally more machinable because their metallic binder improves ductility. Both still require careful control because of high stiffness and cutting resistance.
6. What cutting tools are used for hard materials?
Carbide, CBN, ceramic, and PCD are common cutting tool materials for difficult applications. Carbide covers a wide range of metals, CBN is especially useful for hardened ferrous materials, ceramics can handle some high-temperature superalloy cutting, and PCD suits abrasive nonferrous materials and composites.
7. What is the hardest cutting tool material?
Diamond is the hardest known cutting tool material, and polycrystalline diamond is widely used in machining abrasive nonferrous materials, composites, graphite, and some plastics. It is generally unsuitable for machining steels at high temperatures because carbon can react with iron and accelerate tool degradation.
8. Why are titanium and Inconel expensive to machine?
Titanium and Inconel usually cost more to machine because they require slower or more controlled cutting conditions, place greater demands on tooling, and need tighter heat and process control. Their raw stock is also relatively expensive, so setup complexity, inspection requirements, and scrap risk can have a larger effect on the final part cost.
