
A part can look complete in CAD and still create problems on the shop floor. Poor tool access, deep pockets, thin walls, sharp internal corners, and overly tight tolerances can make a CNC part difficult to machine. These design choices often require longer tools, additional setups, slower cutting, and more inspection, which can increase costs and lead times.
This guide explains how to design parts for CNC machining with practical rules for feature geometry, setup planning, tolerances, materials, finishing, and technical drawings, so you can prepare more manufacturable parts before requesting a quote.
What Does Design for CNC Machining Mean?

Design for CNC machining is the process of defining a part’s geometry and technical requirements for accurate and consistent production. It applies to processes such as CNC milling, CNC turning, and multi-axis machining. Beyond the final shape, the design defines dimensions, tolerances, datum relationships, and other requirements that control the part’s function.
CNC design is a process-specific application of Design for Manufacturability (DFM). CNC DFM connects design intent with the capabilities and limitations of CNC manufacturing. Its goal is to preserve the features that control fit and performance while avoiding unnecessary constraints that increase machining difficulty without adding functional value.
Key Design Constraints in CNC Machining
CNC part design must account for three basic constraints: cutting tool geometry, tool rigidity, and physical access to the workpiece. Together, they determine which features a machine can produce and whether the process can maintain the required accuracy.
Cutting Tool Geometry
Most CNC end mills and drills have round, cylindrical bodies with a fixed diameter and limited cutting length. As the tool removes material, its shape influences the geometry left on the part. A standard end mill, for example, always leaves a radius in a vertical internal corner because a rotating round cutter cannot create a perfectly sharp inside corner.
Tool geometry also affects slot widths, pocket floors, blind holes, and fine details. A standard drill usually leaves an angled point at the bottom of a blind hole, while a flat-bottom hole may require an end mill, boring operation, or special tool. Match part features to standard tool shapes unless the function clearly requires a different result.
Tool Reach and Rigidity
A cutting tool must extend far enough from its holder to reach the full depth of a pocket, cavity, bore, or tall wall. However, a longer tool overhang reduces rigidity. Cutting forces can then deflect the tool and cause chatter, dimensional variation, poor surface finish, or premature tool wear.
Deep features often require more reach than their nominal depth because the tool shank must also clear the surrounding walls. A narrow opening makes the problem worse. It limits the cutter diameter and may force us to use a longer, thinner tool, which further reduces stability.
You should avoid deep, narrow features where possible and provide enough clearance around the cutting area. A wider opening lets us use a larger-diameter tool with a shorter overhang, which improves cutting stability and dimensional control.
Tool Access and Workholding
The cutting tool needs a clear approach path to every machined feature. On a 3-axis machine, the tool normally approaches the part from one direction during each setup. Features on the underside, behind a wall, or inside a restricted area may require another setup, a special cutter, or multi-axis machining.
Grouping related holes, pockets, and surfaces along the same machining direction allows us to reach more features in one setup, reducing part rotation and repositioning. Five-axis machining can improve access to angled or multi-sided features, but the spindle, tool holder, fixture, and workpiece still need enough clearance to move without collision.
Tool access also depends on how we hold the part. We need stable clamping surfaces that resist cutting forces without blocking critical features. A practical design leaves enough material for secure workholding while keeping all required machining areas accessible.
Design Guidelines for Common CNC Part Features
Common features in CNC parts require different design decisions because each feature interacts with the cutting tool in a different way. Cavities, internal corners, thin walls, holes, threads, slots, undercuts, and lettering all need practical dimensions, adequate tool access, and enough structural support to maintain machining stability and dimensional accuracy.

Cavities and Pockets
Keep cavity depth within about four times the smallest internal width where possible. For example, a pocket with a minimum width of 20 mm should generally stay within about 80 mm deep as an initial DFM target. This proportion gives the cutter enough space and helps limit excessive tool overhang.
If only one area requires extra depth, use a stepped or variable-depth pocket instead of extending the full cavity. Wider openings and open-sided pockets also improve tool access and chip removal. Deep, narrow, and fully enclosed pockets usually require longer tools, slower cutting, and additional finishing passes.
Internal Corners and Radii
Use the largest vertical internal corner radius that the part function allows. A radius of about one-third of the cavity depth provides a practical starting point. The specified radius should also be slightly larger than the cutter radius, which allows the tool to follow a smoother path through the corner.
For the floor edge, use no intentional radius, R0.5 mm, or R1.0 mm, where the function allows. These standard options usually fit common flat-bottom or corner-radius tools. Larger floor fillets may require a ball end mill and additional finishing process. If a square mating component must fit inside the pocket, use dog-bone or T-bone reliefs instead of specifying sharp internal corners.
Thin Walls and Tall Features
Use wall thicknesses of at least about 0.8 mm for metals and 1.5 mm for engineering plastics where possible. For tall walls, keep the unsupported height within about four times the wall thickness as an initial design target. Thin or tall features can deflect during cutting, making wall thickness, flatness, and surface finish harder to control.
If the part requires a thin or tall feature, increase the local thickness, reduce the unsupported height, or connect it to nearby geometry with ribs or supports. Avoid placing tight tolerances on flexible free edges unless the function clearly requires them, because the feature may move during machining and spring back after cutting.
Holes and Bores
Choose standard metric or imperial drill bit sizes whenever the part function allows. Standard drill sizes support direct machining and provide more options for later reaming or boring. Keep general holes within about 4D, based on the nominal hole diameter. Holes between 4D and 10D need suitable drills and closer process control, while holes above 10D usually require a dedicated deep-hole drilling process.
Always consider the hole diameter and depth together. For blind holes, state the required cylindrical depth and add space for the drill point. For precision bores, define the fit, diameter tolerance, and surface finish so we can select drilling, reaming, or boring correctly.
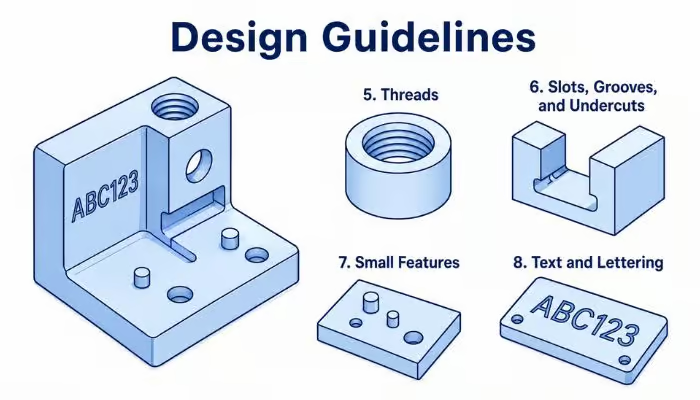
Threads
Choose standard metric, UNC, or UNF thread sizes and pitches whenever possible. M3 and larger usually provide a practical balance of tool strength, chip clearance, and inspection access. Smaller threads remain possible, but they need closer review in hard materials or deep blind holes.
Set the engagement length according to the joint load and tapped material. As a practical starting point, use about 1D–1.5D in steel and 1.5D–2D in aluminum. Full thread depths above 3D rarely improve joint strength and usually add machining time and tool risk.
For blind threaded holes, specify the usable full thread depth separately from the total drilled depth. Leave about 1D to 1.5D of additional depth below the full thread as an initial allowance for the drill point, tap lead, tool runout, and chip space. The final allowance should match the selected threading tool and hole geometry.
Slots, Grooves, and Undercuts
Match slot and groove widths to standard cutter sizes, and keep narrow features as shallow as the design allows. As a practical starting point, limit slot depth to about four times the slot width. Deeper slots may require longer, smaller-diameter tools, which increases deflection, vibration, and tool-breakage risk.
Grooves need enough space for the cutter to enter, complete the cut, and retract. Define the width, depth, bottom radius, and end relief clearly on the drawing. Standard dimensions also give us more options for internal, external, face, and O-ring groove tools.
Undercuts require dedicated cutters because standard end mills cannot reach behind an overhanging surface. Prefer standard T-slot and dovetail dimensions, including common dovetail angles such as 45° or 60°. Leave enough clearance for both the cutting head and tool shaft, not only the finished undercut profile.
Small Features
Small features include narrow ribs, tiny bosses, pins, recesses, and other fine machined details. For routine CNC machining, use a width or diameter of at least 2.5 mm. This size generally supports more stable cutting tools and reduces machining time and tool risk.
- Small-feature range: Features between 0.5 mm and 2.5 mm may be machinable, but they require closer review of the material, depth, tolerance, and tool access.
- Practical minimum: About 0.5 mm may be possible for shallow and accessible details, but it should not be treated as a universal machining limit.
- Feature depth: Keep narrow features within about four times their width as an initial design guideline. Deeper features require longer and less rigid tools.
Text and Lettering
Recessed engraving is usually more efficient than raised lettering because the tool only follows the character paths instead of removing the surrounding surface. Use a simple sans-serif font and place the text on a flat, accessible face.
For machined text, use a minimum stroke width of about 0.5 mm in plastics and soft metals and 0.8 mm in harder metals. An engraving depth of approximately 0.3 mm is sufficient for many part numbers, labels, and identification marks. Use laser marking instead when the text does not need physical depth.
| Feature | Practical Design Guideline |
| Cavities and pockets | Limit depth to about 4× the minimum pocket width. |
| Internal corners and radii | Provide a vertical corner radius of about one-third of the cavity depth; select R0.5 mm or R1.0 mm for common floor edges. |
| Thin walls and tall features | Maintain at least 0.8 mm for metal walls and 1.5 mm for plastic walls; limit unsupported height to about 4× the wall thickness. |
| Holes and bores | Keep routine drilled holes within about 4D; depths above 10D may require deep-hole drilling. |
| Threads | Allow about 1D–1.5D engagement in steel and 1.5D–2D in aluminum; avoid full thread depths above 3D. |
| Slots, grooves, and undercuts | Match widths and profiles to standard cutters; limit slot depth to about 4× its width. |
| Small features | Target 2.5 mm or larger for routine machining; review features between 0.5 mm and 2.5 mm individually. |
| Text and lettering | Specify a stroke width of about 0.5–0.8 mm and an engraving depth of about 0.3 mm. |
Part Orientation and Machine Setup Considerations

Part orientation affects tool access, workholding stability, setup count, and dimensional consistency. A feature may be easy to reach but still difficult to machine if critical surfaces require separate setups or the part lacks suitable clamping and locating areas.
- Setup count: Align related features along the same machining direction. Fewer setups reduce repositioning error, machining time, and fixture requirements.
- Critical feature relationships: Keep coaxial bores, bearing seats, sealing faces, and tightly positioned holes in the same setup to better control runout, position, perpendicularity, and parallelism.
- Datum and workholding: Select rigid, repeatable surfaces for locating and clamping. Avoid using thin walls, flexible edges, or surfaces removed during machining as primary datums.
- Machine and fixture selection: Three-axis machining suits features arranged along simple perpendicular directions, while five-axis machining improves access to angled and multi-sided geometry. Rotational parts may be more suitable for turning or combined turning and milling.
- Tool clearance: Check the complete machining assembly, including the cutter, holder, spindle, clamps, and fixture. Tool-tip access alone does not guarantee collision-free machining.
During DFM review, we evaluate setup directions, datum transfer, fixture requirements, tool clearance, and inspection access before selecting 3-axis machining, 5-axis milling, turning, or combined machining. This helps maintain critical feature relationships while reducing unnecessary repositioning.
How Should You Define Tolerances, GD&T, and Surface Finish for CNC Parts?
Tolerances, geometric controls, and surface finish should reflect the part’s functional requirements rather than applying the tightest values to every feature. Over-specification increases machining time, setup complexity, inspection work, and rejection risk without improving performance.

Set Functional and General Tolerances
Assign tight tolerances only to features that control fit, sealing, motion, or alignment. A general tolerance of about ±0.1 mm suits many noncritical machined dimensions, while ±0.05 mm or tighter may require additional finishing and inspection. Avoid applying tight tolerances between features machined in different setups, as re-clamping introduces additional variation.
Define Datums and GD&T Controls
GD&T, or Geometric Dimensioning and Tolerancing, controls feature form, orientation, location, profile, and runout beyond ordinary ± tolerances. Use it when assembly, sealing, rotation, or alignment depends on the relationship between critical features. Select stable functional surfaces or axes as datums A, B, and C, and avoid thin, unfinished, or inaccessible geometry.
- Hole patterns and locating pins: Use position tolerance relative to the assembly datums. Apply MMC only when the mating clearance allows bonus tolerance and functional gauging.
- Mounting and sealing faces: Use flatness when the surface itself must remain uniform. Add parallelism or perpendicularity only when its relationship to another datum affects assembly or sealing.
- Shafts and bearing seats: Establish the functional axis from a datum bore or diameter, then control related diameters and faces with runout, total runout, or perpendicularity.
- Complex machined surfaces: Use profile tolerance when several dimensions would otherwise be needed to control the same contour.
Keep functionally related features under the same datum system. Avoid applying position, concentricity, and runout to the same feature unless each control addresses a separate requirement. During DFM review, confirm that the fixture can reproduce the datum reference frame and that a CMM, probe, gauge, or indicator can verify every specified control.
Specify Surface Finish Requirements
Match the surface finish to the function of each face. For many noncritical surfaces, Ra 3.2 µm provides a practical standard machined finish. Closer fits, sliding contact, and sealing surfaces often benefit from Ra 1.6 µm, while Ra 0.8 µm or lower typically requires grinding, honing, polishing, or another dedicated finishing process.
Do not apply the same finish requirement to the entire part unless every surface needs it. Mark only the bearing seats, sealing faces, sliding surfaces, and cosmetic areas that require tighter control. Also state whether the specified finish applies before or after anodizing, plating, coating, heat treatment, or polishing.
How Do Materials and Secondary Processes Affect CNC Part Design?
Material machinability, residual stress, heat treatment, and surface finishing influence both part geometry and final dimensions. They affect wall thickness, feature depth, tolerance strategy, machining allowance, and mating fits, and may determine whether critical features remain within specification after machining and post-processing.

Material Machinability and Dimensional Stability
Material machinability directly affects feature geometry and machining stability. Aluminum and free-machining steels usually support smaller tools, deeper features, and faster cutting. Stainless steel, titanium, hardened alloys, and abrasive materials create higher cutting forces, heat, and tool wear. For these materials, favor rigid walls, larger internal radii, accessible features, and realistic tolerances. Avoid deep narrow pockets and fine details unless the part function requires them.
Dimensional stability becomes more important when machining removes large amounts of stock. Large plates, thin rings, long shafts, asymmetric parts, and heavily pocketed components can warp as residual stress redistributes. Reduce this risk with balanced material removal, uniform section thicknesses, and rough machining on both sides when the geometry allows. Engineering plastics add thermal expansion, moisture absorption, and lower stiffness to the design considerations. For precision parts, balance material removal, avoid abrupt section changes, and reserve critical bores, faces, and diameters for final machining after roughing.
Heat Treatment and Distortion
Heat treatment can change hardness, size, flatness, straightness, and roundness. Through hardening, carburizing, induction hardening, and precipitation hardening create different levels of dimensional change. Thin walls, long shafts, asymmetric sections, and large thickness changes are more likely to distort during heating and cooling.
Plan the part geometry and machining sequence around the required treatment. Keep section changes gradual, avoid unnecessary thin areas near hardened zones, and leave finishing allowance on bearing seats, precision bores, sealing faces, and other critical dimensions. The drawing should also state the required hardness or case depth and identify which dimensions must meet tolerance after heat treatment.
Coating, Plating, and Finishing Allowances
Coating thickness becomes part of the final dimensional stack for precision fits. Plating builds material on shafts and inside bores, anodizing affects aluminum dimensions, while polishing removes a small amount of surface material. Design bearing seats, press fits, precision bores, and threads around the required final dimensions. Add machining allowance or masking where the treatment would interfere with fit or function.
Define the treatment condition directly on the drawing. Identify sealing faces, grounding areas, threads, and precision mating surfaces that need masking or post-finish machining. Also state whether critical dimensions and tolerances apply before or after anodizing, plating, coating, or polishing. This prevents the finishing process from shifting a correctly machined feature outside its final tolerance.
CAD Model and Technical Drawing Checklist for CNC Machining Design
Before releasing a CNC part for quotation or production, review the CAD model and technical drawing together. A CNC-ready design package should clearly define the final geometry, functional tolerances, material condition, and surface requirements while giving the manufacturer enough flexibility to select an appropriate machining process.
- Product definition: Confirm the part number, units, revision, and nominal geometry. Make sure the CAD model and drawing do not contain conflicting dimensions or features.
- Dimensions and tolerances: Mark all required dimensions clearly and keep them consistent with the CAD model, with general tolerances for unspecified dimensions and specific tolerances for critical features.
- Holes, threads, and special features: Clearly specify hole depth, thread size, pitch, class, counterbores, countersinks, undercuts, chamfers, and other details that the 3D geometry alone may not fully communicate.
- Datums and GD&T: Follow the selected GD&T system, such as ASME Y14.5 or ISO 1101. Select functional datums and apply position, runout, profile, orientation, or other controls only where the part requires them.
- Material and final condition: State the exact material grade, heat treatment, hardness, coating, plating, and other secondary processes. Clarify when critical dimensions apply to the finished condition after these processes.
- Surface texture and edges: For ISO-based drawings, follow ISO 21920-1:2021 when specifying surface texture. Mark Ra requirements on surfaces that need controlled finish, and add edge-break or deburring requirements where necessary.
Conclusion
Good CNC part design balances functional requirements with practical machining limits. Use tool-friendly radii and feature proportions, maintain adequate wall thickness, avoid unnecessary deep or narrow geometry, and select standard holes and threads when the design allows. Plan part orientation, workholding, tolerances, GD&T, material behavior, heat treatment, and surface finishing around the features that control fit and performance. These decisions help reduce setup complexity, tool risk, dimensional variation, and unnecessary machining cost.
DZ Making supports CNC projects from DFM review through machining and finishing. Our capabilities include 3-axis and 5-axis CNC milling, CNC turning, precision machining of metals and engineering plastics, heat treatment, surface finishing, and dimensional inspection. Send us your CAD model and technical drawing, and our engineering team can review feature geometry, tolerances, machining strategy, and post-processing requirements before production.
FAQs
1. How to design a part for CNC machining?
Start with geometry that matches standard cutting tools and provides clear tool access. Use practical wall thicknesses, internal radii, pocket depths, hole sizes, and thread dimensions. Then define part orientation, workholding, functional tolerances, GD&T, material, and secondary processes before releasing the CAD model and drawing.
2. Can CNC machining create sharp internal corners?
Standard rotating end mills cannot produce perfectly sharp vertical internal corners. Add an internal radius that matches a practical cutter size; a radius around one-third of the cavity depth provides a useful starting point. If a square mating component must fit into the pocket, use dog-bone or T-bone reliefs instead.
3. What is a practical minimum wall thickness for CNC machining?
For routine CNC machining, start with about 0.8 mm for metal walls and 1.5 mm for engineering plastics. Thinner walls may be possible, but cutting forces, material stiffness, wall height, and tolerance requirements increase the risk of deflection and dimensional variation.
4. How deep should you design CNC pockets and holes?
Keep pocket depth within about 4× the minimum pocket width as a practical DFM target. For drilled holes, depths up to about 4D are generally straightforward; 4D–10D requires closer process control, while holes deeper than 10D may need dedicated deep-hole drilling methods.
5. Do CNC-machined parts need a 2D technical drawing?
Not every CNC part requires a separate 2D drawing if the 3D product definition contains all manufacturing requirements. A technical drawing becomes important when you need to communicate tolerances, GD&T, thread classes, surface finish, heat treatment, coating, or other requirements that the nominal CAD geometry does not fully define.
6. When should you design a part for 5-axis machining?
Consider 5-axis machining when a part contains angled surfaces, compound geometry, or critical features on several sides that would otherwise require multiple setups. It can improve tool access and maintain feature relationships in fewer setups, but simple prismatic geometry often remains more economical on 3-axis equipment.
