
Manufacturing industrial machinery components involves several decisions before production begins. Part loads, geometry, tolerances, material properties, production volume, and assembly requirements all affect the manufacturing route. If these factors are not considered together, they can increase machining time, complicate inspection, raise costs, or cause fit and performance problems.
This guide explains how industrial machinery components are planned, manufactured, and inspected. You will also learn how to choose suitable materials, processes, tolerances, and production strategies for different types of machinery parts.
What Are Industrial Machinery Components?
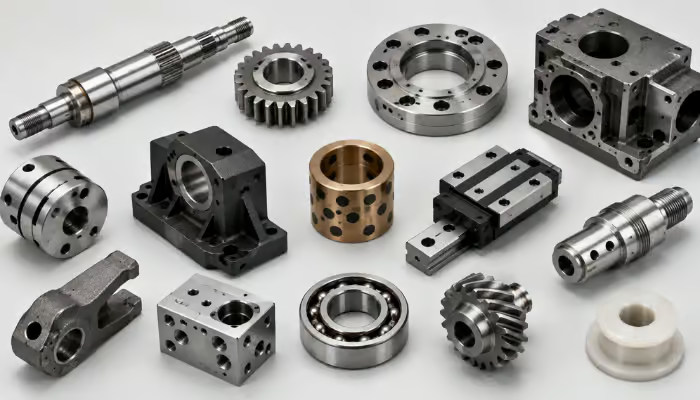
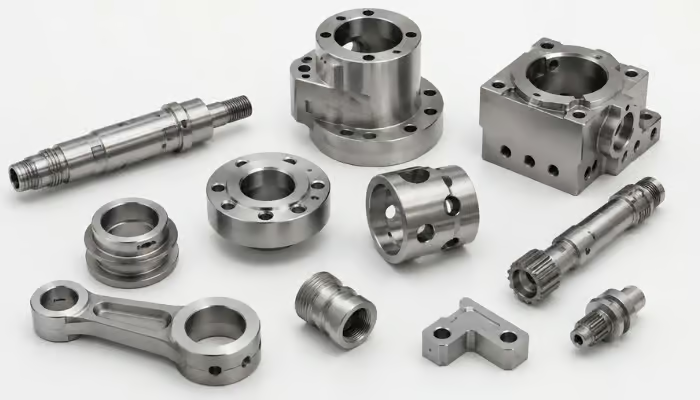
Industrial machinery components are individual parts and subassemblies that perform specific mechanical functions within industrial equipment. They support loads, transmit motion, guide movement, connect structures, or contain fluids in machine tools, conveyors, packaging equipment, automated production systems, and other industrial machinery.
Many industrial machine parts are designed for a specific assembly, operating load, motion requirement, or working environment rather than being used as general-purpose hardware. Their dimensions, material properties, fits, surface condition, and mechanical performance must match their intended function. The manufacturing method also needs to suit the part geometry, material, accuracy, and production volume.
Key Factors in Manufacturing Industrial Machinery Components
Several factors determine whether an industrial machinery component can be produced accurately, consistently, and cost-effectively. Load, geometry, tolerances, surface requirements, production volume, and service life all affect material choice, machining strategy, inspection, and the production route. Evaluating these factors early helps avoid unnecessary operations while ensuring reliable performance.
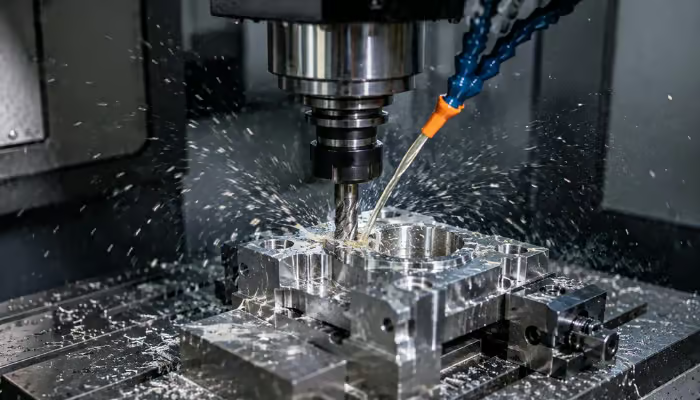
Load and Mechanical Performance
The component must first meet the machine’s mechanical demands. Industrial machinery parts may experience static loads, repeated cycling, impact, vibration, torsion, bending, or combinations of several loading conditions. These forces determine the strength, stiffness, fatigue resistance, and wear performance the component must provide.
For example, shafts and couplings that transmit torque require sufficient strength and fatigue resistance, while machine frames and mounting structures depend more on stiffness and dimensional stability. Bushings, guides, and bearing interfaces face repeated contact, so wear resistance and surface condition become more important. These loading conditions influence material selection, heat treatment, and surface requirements, not just the final dimensions of the part.
Geometry and Part Size
Machinery part geometry affects machine selection, tool access, workholding, setup count, and the sequence of manufacturing operations. Simple rotational components are often suited to CNC turning, while prismatic parts with pockets, mounting faces, and hole patterns generally require milling. Parts with features on several sides may benefit from 4-axis or 5-axis machining because fewer setups can improve access and maintain feature relationships.
Part size creates a different set of constraints. Large components require enough machine travel, rigid fixturing, and stable support, while thin walls, deep pockets, long bores, and narrow features can increase vibration, tool deflection, or distortion. Geometry should therefore be evaluated together with the available manufacturing process and equipment capacity.
Tolerances, Fits, and Surface Finish
Tolerances, fits, and surface finish directly affect the manufacturing difficulty, process sequence, inspection method, and assembly performance of industrial machinery components. A bearing bore with a tight fit may require precision boring, reaming, or grinding after rough machining, while a mounting face with strict flatness may need controlled fixturing and an additional finishing operation.
Shaft journals, locating bores, and other mating features may follow standardized tolerance and fit systems defined in ISO 286-1. For example, a 50 mm H7 hole has a tolerance of 0 to +0.025 mm, illustrating how functional fits can require much tighter dimensional control than general features. Sealing and sliding surfaces may also require controlled roughness. Industrial machinery part drawings should therefore distinguish critical functional features from non-critical dimensions to avoid unnecessary machining and inspection costs.
Production Volume and Lifecycle Requirements
Production quantity influences how industrial machinery components are manufactured, including the level of tooling, fixture design, process control, and material preparation required. Prototypes and low-volume parts often favor flexible CNC machining, while higher-volume production may justify dedicated fixtures, automated inspection, or cast and forged blanks to reduce cycle time and improve batch consistency.
Industrial machinery components may also remain in service for many years. Replacement availability, drawing control, material continuity, revision history, and repeatable inspection criteria can therefore matter beyond the initial production run. For machinery with a long operating life, manufacturing planning should consider not only the current order quantity but also future maintenance, replacement, and repeat production requirements.
Common Materials for Industrial Machine Parts
Material selection affects strength, stiffness, wear resistance, corrosion behavior, weight, machinability, and service life. Industrial machine parts commonly use metals, engineering plastics, and composites, but the final choice should match the operating load, environment, required precision, and expected maintenance cycle.
Metals
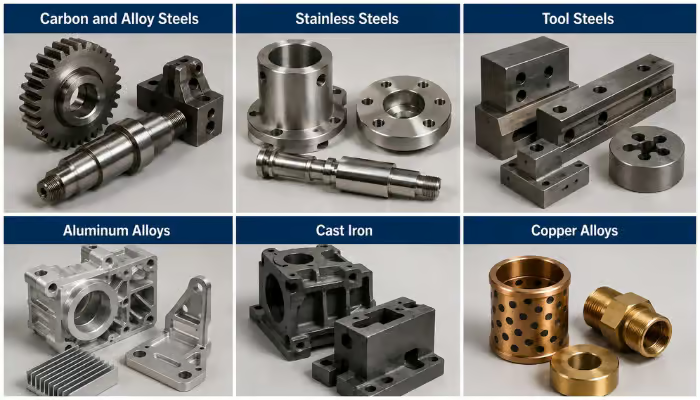
Metals are the most widely used materials for industrial machine parts because they offer a broad range of strength, stiffness, toughness, wear resistance, and finishing options. The suitable grade depends on load, corrosion exposure, weight limits, heat treatment needs, and machining requirements.
- Carbon and alloy steels: Strength, fatigue resistance, and heat-treatability make them a practical choice for shafts, gears, fixtures, and heavily loaded parts.
- Stainless steels: Corrosion resistance suits shafts, housings, fluid-handling parts, and equipment exposed to moisture, chemicals, or washdown.
- Tool steels: High hardness and abrasion resistance support wear guides, dies, tooling elements, and contact surfaces that see repeated loading.
- Aluminum alloys: Their lower density and good machinability make them useful for housings, brackets, covers, and moving automation parts.
- Cast iron: Its stiffness, damping capacity, and dimensional stability work well in machine bases, housings, and large support structures.
- Copper alloys: Bronze and brass perform well in bushings, fittings, and sliding interfaces where low friction or corrosion resistance matters.
Engineering Plastics
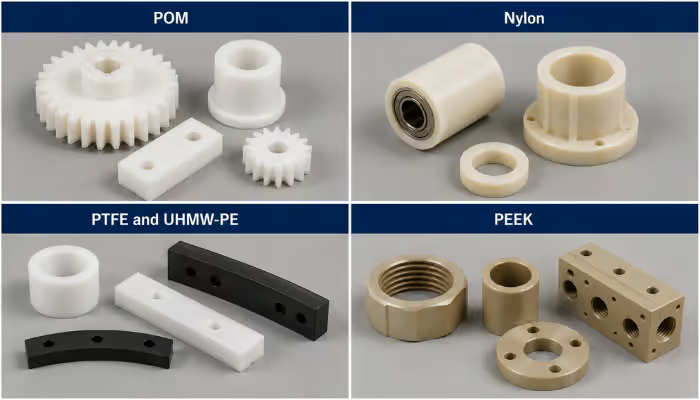
Engineering plastics are useful when low weight, corrosion resistance, electrical insulation, low friction, or chemical resistance matters more than high structural stiffness. Dimensional stability, thermal expansion, moisture absorption, and cutting heat can affect machining accuracy and final part performance.
- POM: Good dimensional stability and low friction make it useful for guides, gears, spacers, and moving components.
- Nylon: Toughness and wear resistance suit rollers and bushings, although moisture absorption can shift final dimensions.
- PTFE and UHMW-PE: Very low friction and chemical resistance support sliding surfaces, liners, wear pads, and guide components.
- PEEK: Higher temperature capability and chemical resistance make it suitable for seals, insulators, wear parts, and demanding machine environments.
Composites
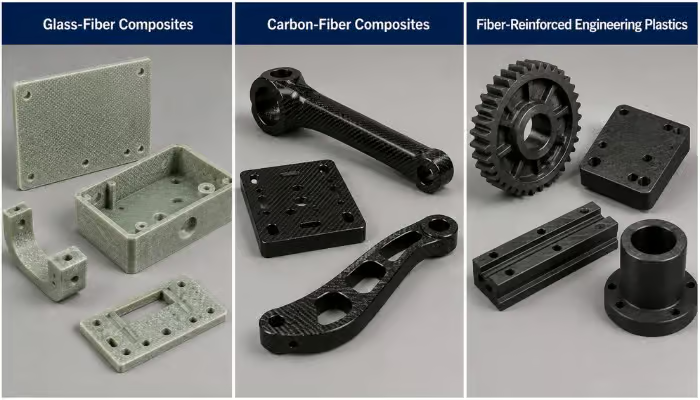
Composites are used in industrial machinery components when low weight, stiffness, corrosion resistance, or electrical insulation justifies more complex machining. Fiber reinforcement can improve mechanical performance, but it can also increase tool wear and create risks such as delamination, edge damage, and dust.
- Glass-fiber composites: Their stiffness and electrical insulation suit structural panels, covers, fixtures, and corrosion-resistant components.
- Carbon-fiber composites: High stiffness-to-weight performance is useful in robotic arms, automation structures, and moving assemblies where mass reduction matters.
- Fiber-reinforced engineering plastics: Added reinforcement can improve stiffness and dimensional stability in wear parts, tooling plates, and structural machine components.
Common Types of Industrial Machinery Components
Industrial machinery includes components with different mechanical roles, service requirements, and manufacturing characteristics. Grouping industrial machinery components by function helps connect each part type with its typical geometry, operating conditions, manufacturing methods, and critical production requirements. Common categories include rotating and motion parts, structural and mounting components, housings and functional blocks, and wear or interface components.
Rotating and Motion Components
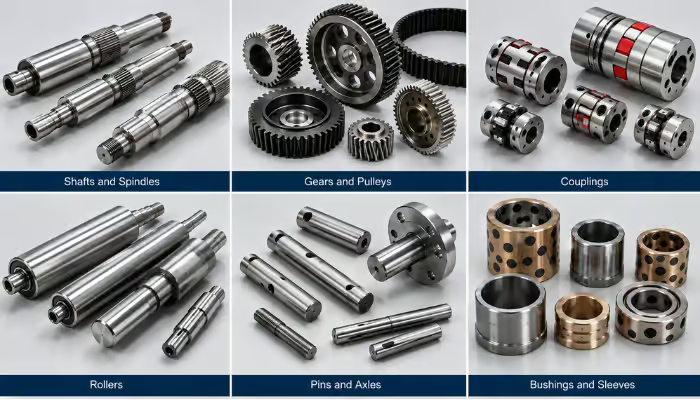
Rotating and motion components transmit torque, support rotation, or guide mechanical movement. Accurate alignment, controlled concentricity, suitable fits, and stable contact surfaces are common manufacturing requirements for these parts. Typical rotating and transmission parts:
Many rotating components start from bar, tube, or forged blanks, with CNC turning used to establish the main rotational geometry. Milling, gear cutting, heat treatment, or grinding may follow depending on the features and performance requirements. For precision bearing journals and similar rotating interfaces, runout may be controlled to around 0.01–0.03 mm depending on the application. Concentricity, fits, and surface finish also need close control where they affect rotation and bearing performance.
Structural and Mounting Components
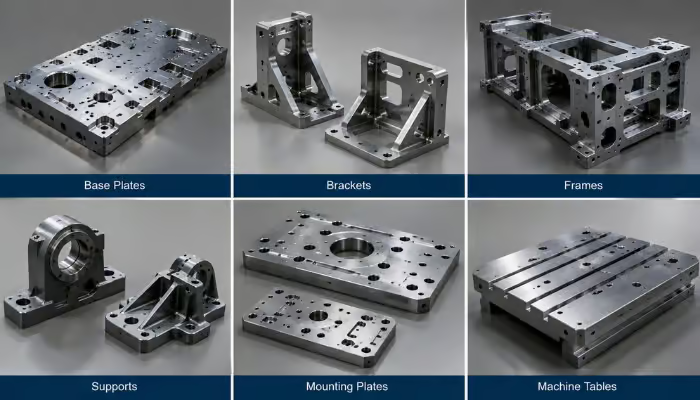
Structural and mounting components support machine assemblies, carry loads, and maintain the relative position of connected parts. Stiffness, flatness, mounting accuracy, and resistance to deformation are key requirements for these machinery components.
- Base plates
- Brackets
- Frames
- Supports
- Mounting plates
- Machine tables
These components may be produced from plate, billet, castings, or welded fabrications. Milling typically creates mounting faces, locating features, slots, and hole patterns, while larger fabricated structures may require stress relief before final machining. Flatness, datum relationships, fixturing stability, and distortion control are often more important than applying tight tolerances to every feature.
Housings and Functional Blocks
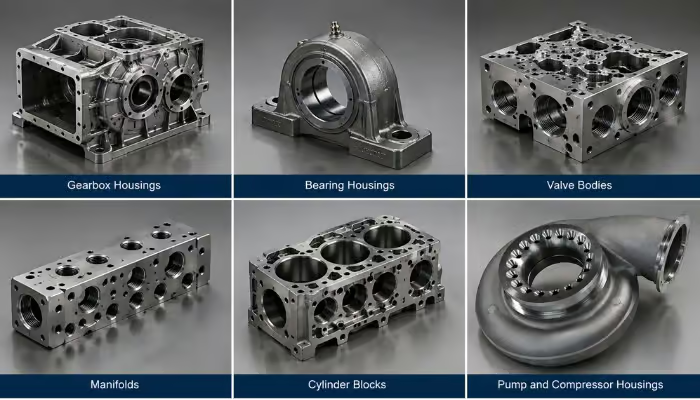
Housings and functional blocks contain, locate, support, or connect other mechanical elements within industrial equipment. They often combine bearing locations, fluid passages, mounting surfaces, sealing interfaces, and other functional features within one component.
- Gear housings
- Bearing housings
- Valve bodies
- Manifolds
- Cylinder blocks
- Pump and compressor housings
Housings and functional blocks commonly begin as billets, cast, or forged blanks before critical faces, bores, cavities, and ports are machined. Milling and boring establish mounting and bearing features, while 4- or 5-axis machining can reach features distributed across several sides. The machining sequence should preserve the required relationships between bearing locations, sealing surfaces, mounting datums, and intersecting passages.
Wear and Interface Components
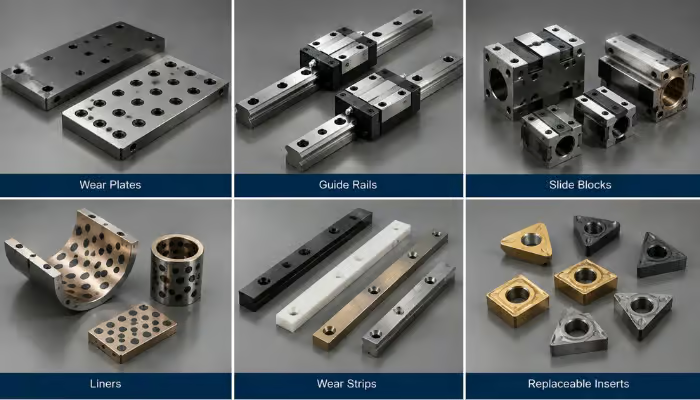
Wear and interface components operate directly against moving parts, seals, conveyed products, or other contact surfaces. Wear resistance, friction behavior, hardness, clearance, and surface condition often determine their service performance.
- Wear plates
- Guide rails
- Slide blocks
- Liners
- Wear strips
- Replaceable inserts
These components commonly use hardened steels, bronze, engineering plastics, or other materials selected for their friction and wear characteristics. Production may combine machining with heat treatment, grinding, polishing, or surface treatment depending on the application. Final hardness, surface condition, dimensional fit, and replaceability can be as important as the basic geometry of the component.
Choosing the Right Manufacturing Process for Machinery Parts
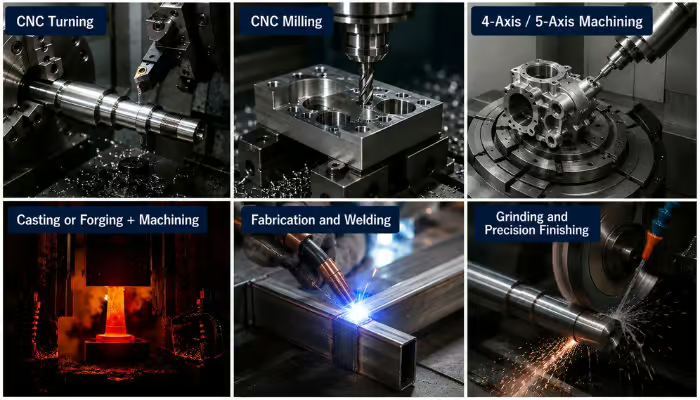
The manufacturing process should match the part’s geometry, material, tolerance requirements, production volume, and functional role. Many industrial machinery parts require more than one process, with machining, heat treatment, grinding, or finishing used at different stages of production. The process sequence should therefore be planned as a complete production route rather than as separate operations.
| Manufacturing process | Best suited for | Typical industrial machinery parts | Manufacturing advantage |
| CNC turning | Rotational geometry | Shafts, sleeves, rollers, bushings | Produces concentric diameters, grooves, and threads efficiently |
| CNC milling | Prismatic geometry | Brackets, plates, housings, blocks | Handles pockets, faces, slots, and hole patterns across varied part layouts |
| 4-axis / 5-axis machining | Multi-sided or angled features | Complex housings, rotary parts, multi-face components | Reduces repositioning and improves feature-to-feature consistency |
| Casting or forging + machining | Near-net-shape blanks or repeat production | Large housings, heavy-duty components | Reduces material removal before precision machining |
| Fabrication and welding | Large structural assemblies | Frames, bases, supports | Builds large structures without machining them from solid stock |
| Grinding and precision finishing | Tight-tolerance or hardened features | Journals, bearing surfaces, precision fits | Improves dimensional accuracy, runout, and surface finish |
Industrial Machinery Component Manufacturing Process
Industrial machinery components usually pass through several linked production stages before they are ready for assembly or service. A typical manufacturing process starts with design review, then moves through material and process planning, machining, secondary treatment, and final inspection. Each stage affects the next, so the sequence needs to be planned around the part’s functional requirements and final accuracy.
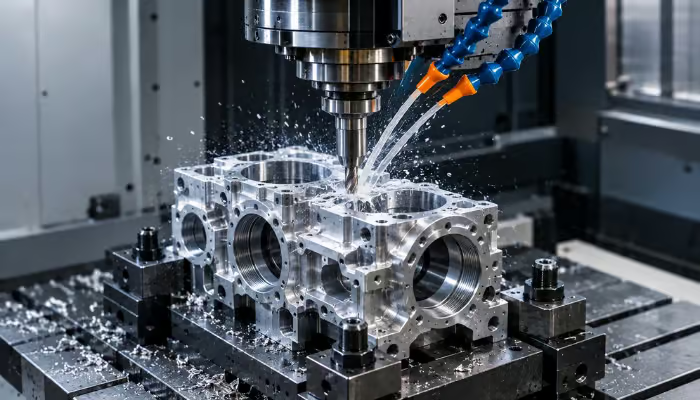
Step 1: Review the Design and Manufacturing Requirements
Production starts with a review of the 2D drawing, 3D model, material specification, tolerances, GD&T, surface finish, and order quantity. The first task is to identify the features that control function and assembly, such as bearing bores, shaft fits, mounting faces, sealing surfaces, and locating features.
The part then goes through design for manufacturability to identify potential production issues before the process plan is finalized. Tool access, wall thickness, feature depth, datum strategy, machining allowance, and inspection access should all be evaluated. This review helps distinguish critical dimensions from general-tolerance features and identifies design changes that may simplify manufacturing without affecting part function.
Step 2: Select the Material and Production Route
Once the design requirements are clear, the next step is to choose the material grade and starting stock that fit the part’s function, size, and geometry. Select bar, plate, tube, casting, or forging based on the amount of material removal and the required strength, wear resistance, corrosion resistance, or subsequent heat treatment.
The production route is then planned before machining begins. Define the datum strategy, setup sequence, and the stage at which each critical feature will reach its final size. Features affected by heat treatment, coating, or stress release should retain suitable allowance for later finishing. This planning sets the order of rough machining, finish machining, treatment, and inspection without finishing critical surfaces too early.
Step 3: Perform Primary and Precision Machining
Machining starts by establishing the main datum surfaces or axes and removing most of the excess material. Rough turning, milling, drilling, or boring creates the basic geometry while leaving machining allowance on features that still require precision finishing. Setup order and workholding should follow the datum strategy defined in the process plan.
Precision machining begins after the main geometry is established. Critical bores, bearing seats, mounting faces, threads, grooves, hole patterns, and other functional features are finished to their specified dimensions, tolerances, and geometric relationships. Features scheduled for later grinding, coating, or heat treatment retain the planned allowance until those operations are complete.
Step 4: Apply Heat Treatment and Secondary Finishing
After the main machining stages, carry out the specified heat treatment according to the material and drawing requirements. Depending on the component, this may include stress relieving, quenching and tempering, case hardening, induction hardening, nitriding, or other thermal processes. Any expected distortion or dimensional change should be allowed for before final finishing.
For example, a bearing housing that requires a heat-treated bore may be rough-machined slightly undersized before heat treatment, then finish bored or ground to final tolerance afterward. Critical surfaces may still require grinding, honing, polishing, or light machining after heat treatment. This is especially important for bearing seats, sealing faces, sliding surfaces, and tight fits.
Step 5: Inspect and Verify the Finished Component
The final step is to confirm that the finished component meets the drawing and project requirements before release. Verify the required dimensions, material condition, surface requirements, and functional interfaces after all machining, heat treatment, and finishing operations are complete. Any nonconforming result should be reviewed before the part moves to assembly, packing, or delivery.
Quality Control for Industrial Machinery Components
Quality control confirms that industrial machinery components meet drawing requirements and remain suitable for assembly and service. Inspection should focus on the characteristics that affect fit, alignment, motion, sealing, load transfer, and repeatability rather than treating every feature as equally critical.
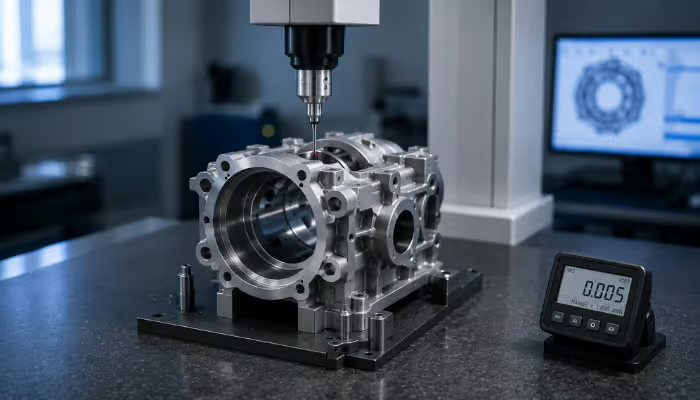
Dimensional and GD&T Inspection
Dimensional inspection checks whether industrial machinery parts meet the required sizes, positions, and geometric relationships. Critical diameters, bore locations, flatness, perpendicularity, parallelism, runout, and positional tolerances should be verified against the drawing datum system and applicable ASME Y14.5 requirements. For precision features with tolerances around 0.01–0.02 mm, the inspection equipment should provide enough resolution and accuracy to identify meaningful variation within the specified limit.
The inspection method should match the feature and tolerance. Micrometers and bore gauges can verify critical sizes, while indicators, height gauges, and coordinate measuring machines can check location and geometric relationships. Measurements should reference the specified datums, and acceptance should follow the tolerance limits on the drawing. For example, a 50.00 ±0.02 mm diameter is acceptable from 49.98 to 50.02 mm; values outside this range are nonconforming.
Material and Surface Verification
Material and surface verification confirms that machine components have the required material condition, hardness, roughness, and surface treatment. A dimensionally correct machinery part can still perform poorly if the material grade, hardness, or surface condition does not match the application.
Material certificates or supplier documentation can confirm the specified material grade and production batch. Hardness testing verifies heat-treated metal parts using methods such as Rockwell, Brinell, Vickers, or Knoop. Surface roughness should also be checked where sealing, sliding, bearing contact, or wear depends on the surface condition, with parameters such as Ra and Rz used where specified.
Functional and Assembly Verification
Functional and assembly verification checks whether precision machinery components can meet their intended assembly and interface requirements. This step focuses on actual fit, movement, alignment, and interaction between related features rather than dimensional results alone. Verification may include trial assembly, go/no-go gauges, thread gauges, mating-part checks, or controlled movement tests where tolerance stack-up could affect fit or motion.
Manufacturing Replacement and Legacy Machine Parts
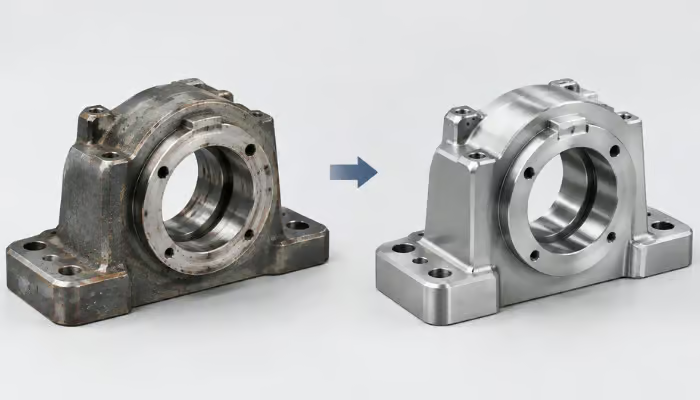
Industrial equipment may remain in service long after original parts or records become unavailable. Replacement industrial machinery components can be manufactured from reliable drawings, physical samples, or approved engineering updates while preserving the interfaces that control fit and function.
Drawing-Based Manufacturing
When reliable drawings or CAD data are available, replacement machinery components can be manufactured to the documented requirements after the applicable revision is confirmed. Critical dimensions, fits, and mating interfaces should remain consistent with the current machine configuration. Older drawings may contain superseded revisions, discontinued materials, or legacy tolerancing, so these requirements should be resolved before production.
Sample-Based Reproduction
Physical samples provide a practical starting point when drawings for replacement industrial machine parts are missing or incomplete. Measurements need to reconstruct the original design condition rather than reproduce wear, deformation, corrosion, or previous repairs. Mating components, standard bearing or seal sizes, and assembly clearances may also help reconstruct critical dimensions that cannot be confirmed from the worn sample alone.
Obsolete Part Upgrades
Legacy machinery parts may be updated when the original material, surface treatment, or manufacturing method is no longer practical. Any approved update should improve manufacturability or service performance while preserving compatibility with the interfaces that control assembly and function. Material substitutions, surface treatment changes, or limited design revisions should be documented so future replacement parts follow the same controlled specification.
Reducing Manufacturing Problems and Costs for Industrial Machinery Components
Manufacturing problems often become expensive when they appear late in production. For industrial machinery components, cost control depends on keeping tolerances realistic, improving manufacturability, limiting distortion, and matching the production route to the required volume. The goal is to remove unnecessary machining and process complexity without affecting fit, function, or service performance.
Set Tolerances Based on Functional Needs
Tight tolerances should be limited to features that directly affect assembly or machine performance. Reducing a dimensional tolerance from ±0.10 mm to ±0.02 mm narrows the allowable variation by five times and may require additional finishing, more controlled setups, and more capable inspection. Bearing seats, locating bores, sealing faces, shaft fits, and alignment features may justify tighter control, while non-critical surfaces can often use wider tolerances to reduce unnecessary machining and inspection costs.
Improve Tool Access and Reduce Setups
Poor tool access can require long-reach tooling, additional fixtures, or repeated repositioning when machining complex industrial machinery components. Deep pockets, narrow internal corners, inaccessible holes, and features spread across many orientations can all increase cycle time and alignment risk. Simplifying access to critical features and reducing unnecessary setups can shorten machining time while improving feature-to-feature consistency.
Control Distortion and Residual Stress
Large, thin-walled, or heavily machined industrial machine parts can distort as material is removed or after heat treatment. Residual stress, uneven stock removal, aggressive clamping, and thermal changes can all shift dimensions after machining. Balanced roughing, stable fixturing, stress-relief steps, and suitable finishing allowances help reduce distortion before critical features reach final size.
Match Raw Material and Process to Production Volume
The starting material form has a direct effect on material waste, machining time, and overall cost. A low-volume custom industrial machinery component may be practical to machine from bar or plate, while higher-volume or repeat production can justify castings, forgings, or dedicated fixtures that reduce stock removal and setup time. A cost-effective production route should balance the required quantity with material removal, tooling investment, and the machining needed to reach the final geometry.
Conclusion
Manufacturing industrial machinery components requires more than selecting a material and machining the final shape. Part function, geometry, tolerances, production volume, process sequence, finishing, and inspection all need to work together throughout production. A well-planned manufacturing route helps control fit, repeatability, service performance, and total production cost.
For custom industrial machine parts, clear technical information makes manufacturing review and quotation more accurate. Provide a 2D drawing or 3D CAD file together with the material, critical tolerances, surface finish, heat treatment, and expected quantity. DZ Making can then review the part for CNC milling, turning, multi-axis machining, and any required secondary finishing before production.
FAQs
1. What is industrial machinery manufacturing?
Industrial machinery manufacturing covers the production of machines, assemblies, and components used in factories, automation systems, processing equipment, material handling, and other industrial operations. It may involve machining, fabrication, casting, forging, finishing, assembly, and inspection.
2. What tolerances are commonly required for industrial machinery parts?
General machined features often use tolerances around ±0.05 to ±0.20 mm, while critical bearing seats, locating bores, and shaft fits may require ±0.01 to ±0.025 mm or tighter. The final tolerance should follow the part function, fit requirements, drawing, and inspection capability.
3. When should machine components use CNC machining instead of casting or forging?
CNC machining suits prototypes, custom machinery components, low-to-medium volumes, and parts with tight tolerances or frequent design changes. Casting or forging may be more economical when near-net-shape blanks reduce material removal or production volume justifies tooling. Many machinery parts combine both approaches.
4. How do heat treatment and surface finishing affect precision machinery components?
Heat treatment can change hardness, strength, wear resistance, residual stress, and final dimensions. Surface treatments can improve corrosion resistance, wear, or friction, while coatings may add thickness to critical fits. Suitable allowance should remain where later treatments may affect final size or surface condition.
5. How can replacement machine parts be manufactured without original drawings?
A physical sample can provide the starting geometry when drawings are unavailable. Dimensions, fits, threads, hole locations, and mating interfaces can be measured, while wear, corrosion, deformation, and previous repairs must be separated from the original design condition. Mating parts and standard bearing or seal sizes can also help recover missing dimensions.
6. What information is needed to quote custom industrial machine parts?
A quotation is more accurate when the supplier receives a 2D drawing or 3D CAD model, material grade, quantity, tolerances, GD&T, surface finish, heat treatment, coating, and inspection requirements. Clear technical requirements reduce assumptions and support a more accurate production plan.
