
Powder coating is widely used on machined metal parts because it adds color, corrosion resistance, and a durable protective layer. However, the coating also adds measurable thickness, requires heat curing, and can interfere with threads, fits, and other precision features if you do not plan for it.
This guide explains what powder coating is, how the process works, which types and metals are suitable, typical coating thickness, cosmetic options, common defects, and the design and drawing details you should specify before ordering powder-coated parts.
What Is Powder Coating?
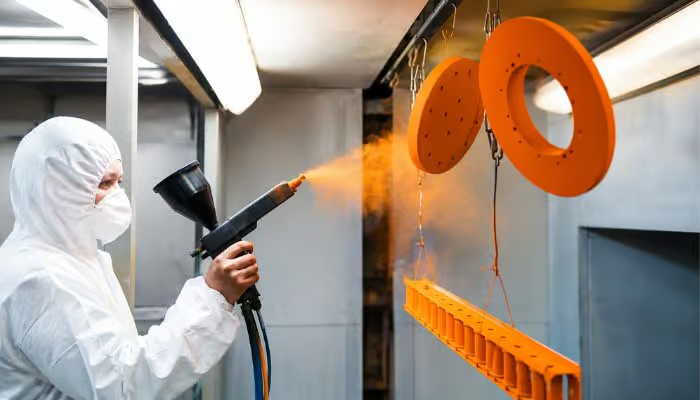
Powder coating is a protective and decorative finish for metal parts that forms a solid polymer layer on the surface. For machined parts, powder coating services can add both functional protection and a controlled cosmetic finish after machining. It can improve corrosion protection, resist scratches and impact, and provide a consistent color, gloss, or textured appearance.
Beyond surface performance, powder coating can also offer environmental benefits compared with many conventional solvent-based coatings. The U.S. EPA identifies powder coatings as an example of low- or no-VOC/HAP coatings and notes that replacing higher-emitting coatings with lower-emitting alternatives supports pollution-prevention goals. This makes lower solvent-related emissions another practical advantage of powder coating in industrial finishing.
Key advantages include:
- Durable surface protection: A properly prepared and cured coating can resist abrasion, impact, chemicals, and atmospheric corrosion in many industrial applications.
- Wide finish selection: Powder systems support matte, gloss, smooth, textured, wrinkle, and many color options without changing the base machining process.
- Consistent coverage in production: Controlled application and curing can provide repeatable appearance and film thickness across production batches.
- Low solvent use: Powder coating uses solid coating material rather than a solvent-based carrier, which can reduce VOC emissions during application.
Key limitations include:
- Dimensional buildup: Powder coating adds measurable film thickness, which can change hole sizes, thread fit, clearances, and other close-tolerance features.
- Heat sensitivity: The curing cycle can restrict its use on assemblies that contain plastics, seals, adhesives, or other temperature-sensitive components.
- Coverage limits: Deep pockets, internal corners, and narrow recesses can receive less uniform coating than open external surfaces.
- Repair difficulty: Local scratches or chips can be touched up, but matching the original color, gloss, texture, and film build can be difficult.
- Functional surface restrictions: Bearing seats, sealing faces, electrical contacts, and precision mating surfaces usually cannot accept normal coating buildup.
What Is Powder Coating Made Of?
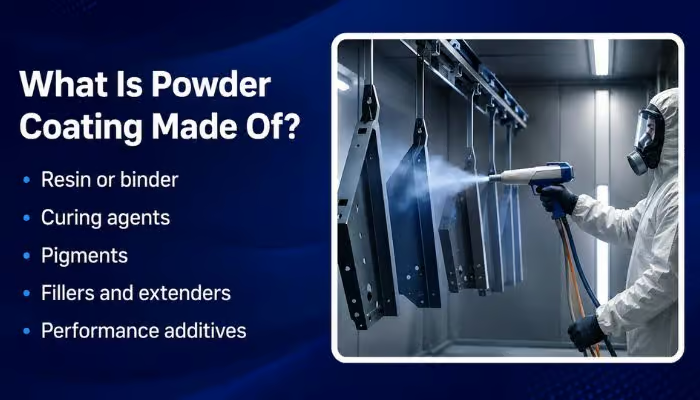
Powder coating is a formulated blend of polymer resin, curing agents, pigments, fillers, and performance additives. The resin forms the main coating film, while the other ingredients control color, hardness, flow, gloss, texture, curing behavior, and resistance to different service conditions. The formulation is typically melt-mixed, cooled, and ground into fine powder particles before application.
The main components include:
- Resin or binder: Forms the main structure of the coating. Common resin systems include epoxy, polyester, epoxy-polyester hybrid, polyurethane, and acrylic. The resin system strongly influences adhesion, flexibility, chemical resistance, UV stability, and suitable service conditions.
- Curing agents: React with compatible thermoset resins during heating to create a cross-linked film. The curing chemistry affects properties such as hardness, chemical resistance, cure conditions, and long-term coating performance.
- Pigments: Provide color, opacity, and visual consistency. Formulations may use organic or inorganic pigments, while metallic and effect pigments can create decorative finishes. Pigment selection can also influence UV and heat stability.
- Fillers and extenders: Mineral ingredients such as barium sulfate, calcium carbonate, and silica may be used to adjust hardness, density, texture, film build, and mechanical properties.
- Performance additives: Flow-control agents, leveling agents, degassing additives, gloss modifiers, and texturing agents help control application behavior and the appearance of the cured surface.
What Are the Main Types of Powder Coatings?
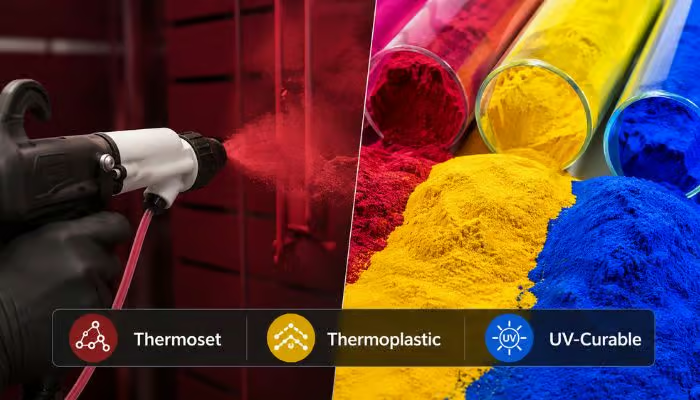
Powder coatings are broadly divided into thermoset and thermoplastic systems, while UV-curable powder coatings use a different curing approach for applications that require faster curing or lower thermal exposure. Thermoset powders form a permanent cross-linked film during curing, thermoplastic powders soften with heat and harden again as they cool, and UV-curable powders use heat for melting and leveling before ultraviolet energy completes the cure.
Thermoset Powder Coatings
Thermoset powder coatings cure through a chemical cross-linking reaction that creates a hard, stable film with good adhesion, chemical resistance, and long-term surface durability. Different resin systems offer different levels of UV resistance, corrosion protection, flexibility, and hardness. Because of this balance of performance and finish control, thermoset powders are commonly used on machined metal parts such as housings, brackets, covers, and equipment components.
Common thermoset systems include:
- Epoxy: Provides strong adhesion, chemical resistance, and corrosion protection. Its limited UV resistance makes it better suited to indoor equipment, machine components, and protected assemblies.
- Polyester: Offers good UV and weather resistance, making it suitable for outdoor housings, brackets, frames, and other exposed metal parts.
- Epoxy-polyester hybrid: Balances the properties of epoxy and polyester. It is commonly used for indoor enclosures, equipment panels, and decorative industrial components.
- Polyurethane: Provides good abrasion resistance, chemical resistance, and surface smoothness. It can suit parts where both appearance and exterior performance matter.
- Acrylic: Offers good color and gloss retention and is used where appearance and weatherability are important.
For CNC parts, polyester and epoxy-based thermoset powders are especially common. Polyester works well for outdoor parts that need UV and weather resistance, while epoxy-based systems suit indoor components that need strong adhesion, chemical resistance, or corrosion protection. Choose the coating system based on the service environment and performance requirements, not color alone.
Thermoplastic Powder Coatings
Thermoplastic powder melts and flows when heated, then hardens as it cools without forming a permanent cross-linked structure. Enough heat can soften the coating again. Common thermoplastic systems include nylon, PVC, polyethylene, and other polyolefins, which offer different combinations of toughness, flexibility, abrasion resistance, and moisture protection.
Thermoplastic coatings often form thicker films than standard thermoset powders. They work well when a part needs a tough protective layer against impact, repeated contact, abrasion, or moisture. However, they are less common for precision CNC housings and cosmetic machined parts where coating thickness and dimensional control are more critical.
UV-Curable Powder Coatings
UV-curable powder coating uses heat to melt and level the powder, then ultraviolet energy completes the curing reaction. This process reduces the thermal load on the part and can suit some heat-sensitive substrates, thin components, and assemblies. UV curing also works quickly, but the coated surface must remain accessible to the UV light for complete curing.
The Main Steps in the Powder Coating Process: 5 Steps
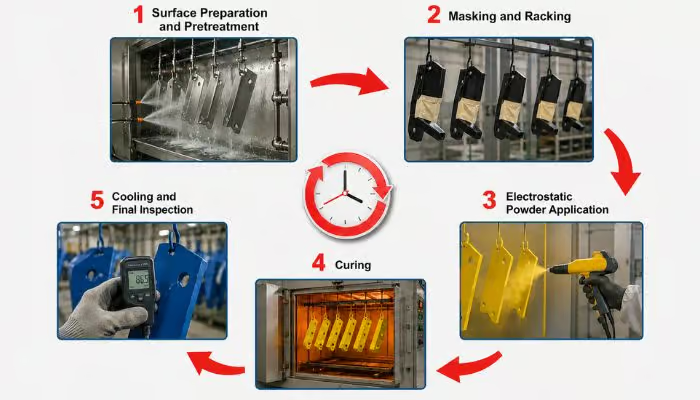
The powder coating process usually includes surface preparation, masking and racking, electrostatic application, curing, and final inspection. Together, these steps create a clean substrate, build a controlled coating layer, develop the required film properties, and confirm that the finished part meets both cosmetic and functional requirements.
Step 1. Surface Preparation and Pretreatment
Surface preparation starts by removing machining oil, coolant, grease, rust, oxide, and other contaminants that could weaken coating adhesion. Depending on the metal and surface condition, this stage may include degreasing, alkaline cleaning, abrasive blasting, rinsing, and thorough drying.
After cleaning, the part may receive a chemical pretreatment to improve adhesion and corrosion resistance. You can use iron phosphate for many steel parts, while zinc phosphate or zirconium-based systems can provide stronger corrosion protection or support a wider range of metals. The exact pretreatment should match the base material and the service environment of the finished part.
Step 2. Masking and Racking
Before spraying, high-temperature tape, silicone plugs, caps, or other masking materials protect areas that must remain coating-free, such as threads, precision bores, electrical contacts, and mating surfaces. The part then moves to racking, where the hook or fixture supports it during spraying and provides the electrical grounding required for electrostatic powder application. A good racking position also keeps the part stable and leaves the required coating surfaces accessible to the spray gun.
Step 3. Electrostatic Powder Application
Once the part is masked, racked, and properly grounded, an electrostatic spray gun applies powder to the exposed surfaces. The gun charges the powder particles so they move toward the grounded metal and build a dry coating layer before curing.
To create even coverage, the spray moves around the part while the process adjusts gun angle, powder flow, and charging level to match the geometry. Deep recesses, internal corners, and narrow pockets need more controlled spraying because the electrostatic field can limit powder penetration in these areas. The process aims for a consistent dry film without excessive buildup before the part enters the curing stage.
Step 4. Curing
The coated part then enters the curing oven, where heat melts and levels the powder and, for thermoset systems, completes the cross-linking reaction. Many conventional thermoset powders cure at about 160–200°C for roughly 10–20 minutes, although the exact schedule depends on the formulation.
The target temperature refers to the part itself, not just the oven air. Part thickness and mass affect how quickly it reaches that temperature, so follow the powder supplier’s technical data sheet for the final cure cycle. Undercuring can weaken adhesion, while excessive heat can affect color, gloss, and film performance.
Step 5. Cooling and Final Inspection
After curing, the parts leave the oven and cool naturally on the rack until the coating hardens enough for safe handling. Cooling time depends on the part material, thickness, and mass, so heavy steel parts generally cool more slowly than thin aluminum parts.
Once the parts reach a stable handling temperature, inspection checks color, gloss, texture, coating coverage, and film thickness. For machined parts, the final check also confirms masked areas, threads, mating surfaces, and any dimensions that apply after coating.
What Metals Can Be Powder Coated?
Aluminum, carbon steel, and stainless steel all work well with powder coating because they support electrostatic application and withstand standard curing cycles. The real difference appears after you consider what the coating needs to achieve. Aluminum often uses powder coating for cosmetic flexibility and added protection, carbon steel benefits strongly from the corrosion barrier, while stainless steel usually uses it to change surface appearance or add a specific functional layer.
Aluminum
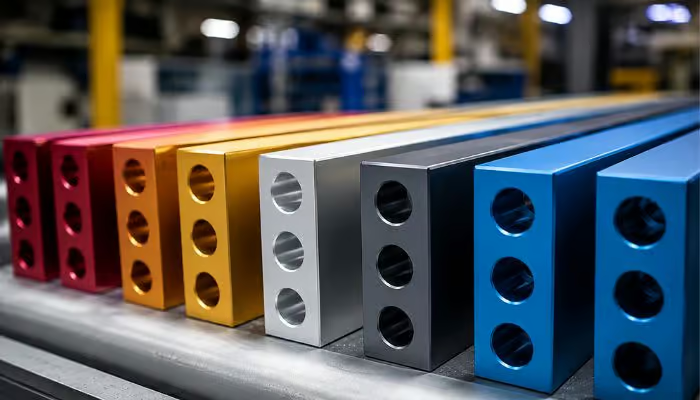
Aluminum pairs well with powder coating when a machined part needs a durable opaque color, controlled gloss, or textured surface. The powder film also adds protection against handling, moisture, and environmental exposure, so it works well for aluminum bearing housings, covers, brackets, frames, and similar components.
The aluminum form also influences the coating result. Wrought machining alloys such as 6061 and 7075 usually provide a dense and relatively uniform substrate, while cast aluminum may contain porosity that releases trapped gases during curing and creates pinholes or bubbles. Aluminum also forms a natural oxide layer, so proper surface preparation helps maintain reliable adhesion. For aluminum parts, the powder chemistry and pretreatment should match the expected exposure conditions and required finish performance.
Carbon Steel
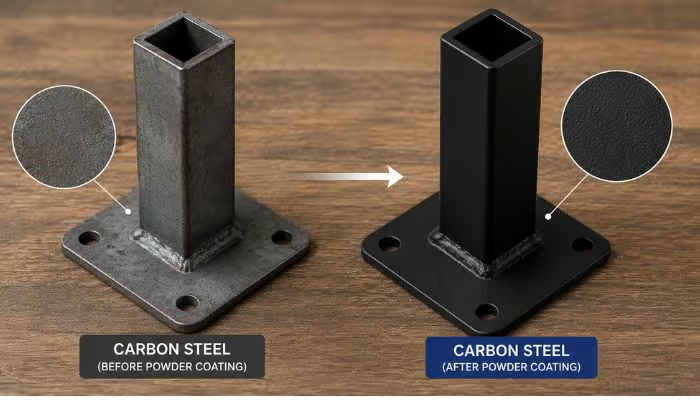
Powder coating adds particular value to carbon steel because the cured film separates the steel surface from moisture, oxygen, and other corrosive exposure. This combination of corrosion protection and a durable colored finish makes it useful for steel mounting plates, brackets, guards, frames, and other industrial components.
Carbon steel has less inherent corrosion resistance than aluminum or stainless steel, which makes the condition beneath the coating especially important. Rust, mill scale, or unstable oxidation can weaken adhesion and allow corrosion to develop under the film. Once scratches or edge damage expose bare steel, corrosion can also spread from the affected area. For carbon steel, long-term coating performance depends more on a stable substrate and continuous protective film than on coating thickness alone.
Stainless Steel
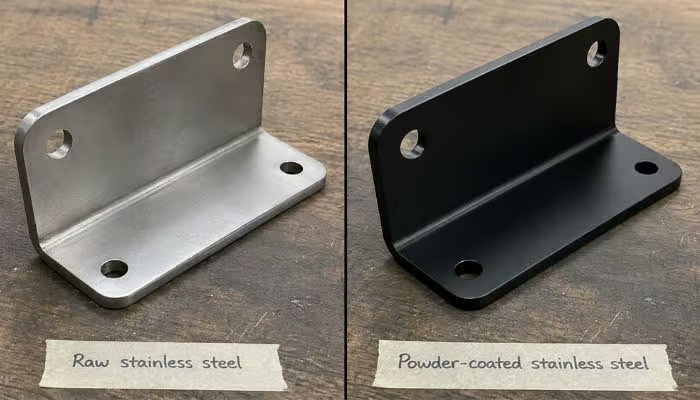
Stainless steel already resists corrosion through its passive surface, so powder coating usually serves a different purpose. You may choose it to create a specific color, matte or textured surface, reduce glare, maintain a consistent appearance across an assembly, or add another barrier for a particular service environment.
The passive stainless surface also makes adhesion an important consideration. Oils, polishing residues, and other contamination can weaken the bond between the coating and metal, so proper surface preparation still matters even when corrosion resistance is not the main goal. Powder coating suits stainless steel parts best when the design calls for a controlled coated appearance or additional surface performance beyond the natural metal finish.
Common Applications of Powder Coating
Powder coating is widely used across industries such as automotive, industrial equipment, electronics, architecture, and consumer products. It suits applications that need a durable finish, consistent appearance, and resistance to moisture, abrasion, handling, or outdoor exposure.
- Industrial equipment: Machine enclosures, control cabinets, safety guards, and equipment panels often use powder coating. The finish helps resist frequent handling, shop-floor dirt, and routine cleaning while keeping a consistent appearance.
- Automotive and transportation: Wheels, suspension parts, underbody components, and car parts often use powder coating. The coating helps protect these parts from road debris, moisture, salt, and changing weather conditions.
- Electronics and electrical equipment: Enclosures, chassis, panels, and equipment housings often require a consistent cosmetic surface while protecting the underlying metal from handling and environmental exposure.
- Architectural and outdoor products: Railings, aluminum frames, outdoor fixtures, fencing, and structural components benefit from powder systems designed for UV exposure and changing weather conditions.
- Medical and laboratory equipment: Metal frames, equipment housings, carts, and non-patient-contact components can use powder coating when the design requires a cleanable, chemically resistant, and consistent surface.
- Consumer and commercial products: Furniture frames, shelving, appliance components, exercise equipment, and display fixtures commonly use powder coating for color control, wear resistance, and repeatable appearance.
What Is the Typical Thickness of Powder Coating?
A typical thermoset powder coating usually has a dry film thickness of about 60–120 μm (2.4–4.7 mils), although the exact range depends on the powder system and finish requirement. Decorative smooth finishes often use about 50–80 μm, textured coatings about 70–120 μm, protective industrial coatings about 80–150 μm, and heavy-duty functional coatings can reach 200–300 μm or more.
The required thickness depends on what the coating needs to achieve. A thin film may not provide enough hiding, edge coverage, or barrier protection, while excessive film build can increase orange peel, reduce surface definition, and create curing or adhesion problems in some powder systems. The ideal film thickness should match the coating type, required appearance, and service environment, and confirm the final range in the powder specification.
What Cosmetic Options Are Available for Powder Coating?
Powder coating can produce a wide range of colors, gloss levels, and surface textures. You can combine these options to create anything from a smooth industrial finish to a low-glare textured surface. For parts with visible cosmetic requirements, these elements should be specified together because changing one can affect the overall appearance of the coating.
Color Options
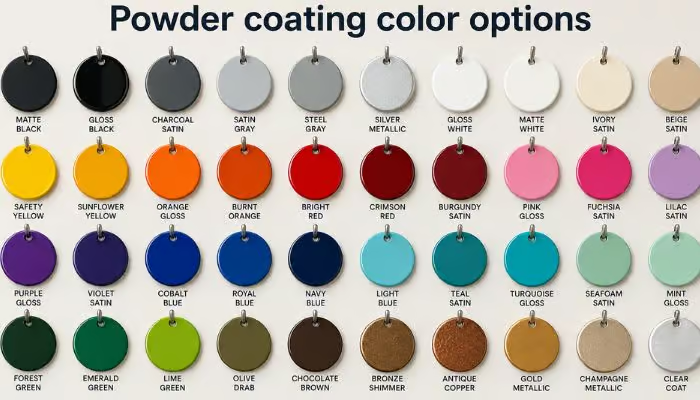
Powder coatings are available in a broad range of solid colors, including standard industrial shades, custom-matched colors, and reference systems such as RAL. You can also specify metallic, pearlescent, and other effect finishes when the design requires more visual depth.
For production parts, the color reference should remain consistent from sample approval through bulk coating. Gloss level, texture, and curing conditions can change how the same color appears, so a color code alone may not fully define the target. An approved coated sample or color panel provides a clearer reference when visual consistency matters.
Gloss Levels
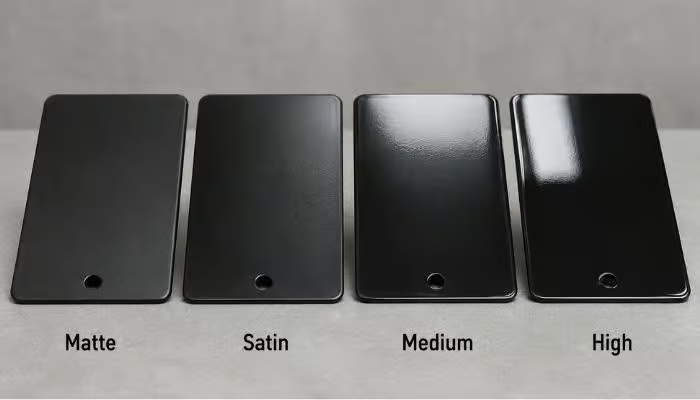
Powder coatings can range from matte and low-gloss finishes to semi-gloss and high-gloss surfaces. The selected gloss level changes both the visual character of the part and how strongly the surface reflects light.
Matte and low-gloss finishes reduce glare and make minor surface variation less noticeable, which can suit equipment housings and panels. High-gloss finishes create a brighter, smoother appearance, but they also reveal scratches, waviness, and small surface defects more easily. The gloss level should therefore match both the intended appearance and the way the part will be viewed and handled.
Surface Textures
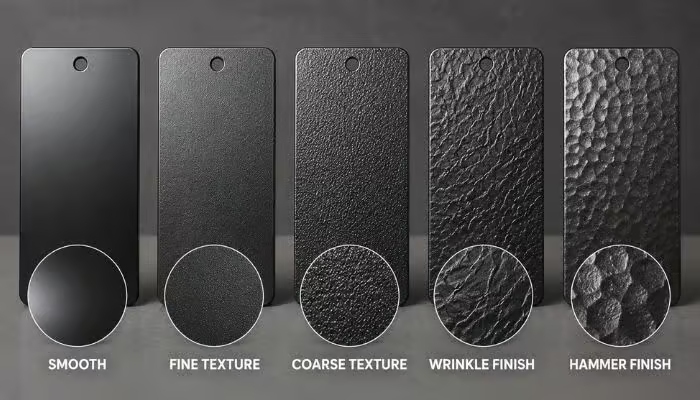
Common powder coating textures include smooth, fine texture, coarse texture, wrinkle, and hammer finishes. The coating formulation creates these surface effects during curing, so each option produces a different visual pattern and surface feel. Texture also affects practical factors such as glare, grip, cleanability, and how visible minor substrate imperfections remain on the finished part.
- Smooth finish: Creates a clean, even surface that keeps edges, graphics, and fine details visible. It works well when appearance and surface clarity matter.
- Fine texture: Adds a light surface pattern that reduces glare and helps make small substrate variations less noticeable without creating a heavily rough feel.
- Coarse texture: Produces a more pronounced surface profile and can improve grip or hide minor cosmetic imperfections, but it also reduces fine visual detail.
- Wrinkle finish: Forms a distinctive raised pattern that gives the surface a stronger industrial appearance and can disguise small variations in the underlying metal.
- Hammer finish: Creates an irregular hammered effect with greater visual depth, making it useful where a decorative industrial look is more important than a perfectly smooth surface.
How Should You Design CNC Parts for Powder Coating?
Design powder-coated CNC parts around the final coated condition, not only the machined dimensions. The coating adds material to exposed surfaces, while masking, spray access, racking, and curing introduce additional design constraints. Planning these details early reduces rework after finishing.
Allow for Coating Thickness
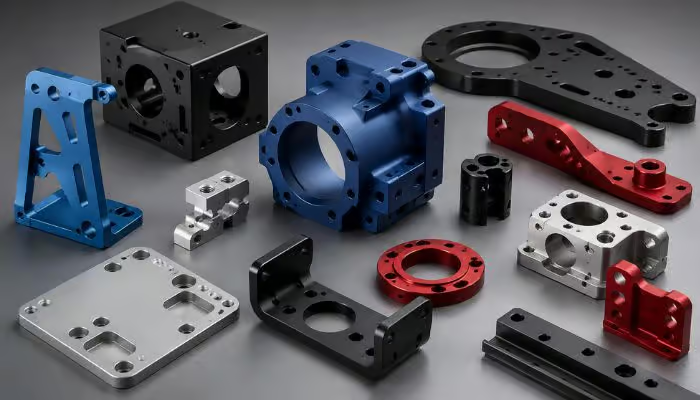
Powder coating adds material to every coated surface, so external dimensions increase while coated holes, slots, and gaps become smaller. This matters most on mating parts, locating features, and close-clearance assemblies where even a small buildup can affect fit.
For example, an 80 μm coating on each side of a 10.00 mm bore can reduce the finished opening to about 9.84 mm. You should therefore define whether critical dimensions apply before or after coating and include the expected film build in the tolerance stack. For bearing seats, precision bores, and other tightly controlled features, masking or post-coating machining usually gives more reliable dimensional control.
Protect Critical Features
Powder coating should not cover every surface by default. Threads, bearing seats, press-fit holes, sealing faces, electrical contacts, and precision locating surfaces depend on controlled dimensions or direct surface contact. Coating buildup on these features can change fit, increase assembly force, reduce sealing contact, or interrupt electrical continuity.
Coating inside a threaded hole can reduce thread clearance, while coating on a bearing seat can interfere with the intended fit. Define these coating-free areas on the drawing and show where the coating boundary should stop. For critical interfaces, masking or a planned post-coating finishing step gives more reliable control than relying on the coating film itself.
Consider Part Geometry and Coverage
Part geometry directly affects powder access and film uniformity. Deep blind pockets, narrow slots, closely spaced walls, and sharp internal corners can develop thin or uneven coverage because the electrostatic field tends to concentrate around the opening instead of carrying powder deep into the recess. This is the Faraday cage effect, and it becomes more noticeable as the feature gets deeper or more enclosed.
Where recessed surfaces require full cosmetic or protective coverage, use wider openings, larger internal radii, and less enclosed geometry where function allows. Small edge breaks or radii can also improve coating continuity on sharp external edges.
Plan Racking and Curing
Part design should leave a practical location for hanging and grounding during powder coating. A non-critical hole, hidden edge, or dedicated tab can support the part and maintain electrical contact without leaving rack marks on important cosmetic surfaces. Keep rack contact points away from sealing faces, precision datums, and other functional areas.
The curing cycle also affects the assembly design. If the CNC part includes plastic inserts, seals, adhesives, magnets, or other heat-sensitive components, install them after powder coating where possible. For multi-piece assemblies, coating the metal components before final assembly can reduce masking and avoid exposing sensitive components to curing heat.
Common Powder Coating Defects and Quality Checks
Powder coating inspection should evaluate both surface appearance and coating performance. For CNC parts, inspection should confirm coating coverage, film thickness, adhesion, color and gloss consistency, while also checking that masked features and critical dimensions remain within specification. Some defects appear visually, while others require thickness or adhesion testing to identify.
| Common Defect | Typical Causes | Quality Check |
| Orange peel | Excessive film build, poor powder flow, or unsuitable curing conditions | Visual inspection and film thickness measurement |
| Pinholes or bubbles | Trapped gas, surface contamination, or porosity in the substrate | Visual inspection, with extra attention to cast parts |
| Thin or uneven coverage | Limited spray access, complex geometry, or Faraday cage areas | Measure film thickness at multiple representative locations |
| Poor adhesion | Surface contamination, inadequate pretreatment, or incomplete curing | Perform the specified adhesion test |
| Color or gloss variation | Variation in film thickness, curing conditions, or powder batch | Compare against the approved sample or specified color/gloss standard |
| Coating on no-coat areas | Incomplete masking or poorly defined coating boundaries | Inspect threads, bores, mating faces, contacts, and other protected features against the drawing |
For tighter quality control, use ASTM D7091 to verify dry film thickness and ASTM D3359 to evaluate adhesion when the drawing or quality specification requires these checks. Add corrosion testing only when the application defines a specific corrosion-resistance requirement.
Powder Coating vs. Other Surface Finishes: Which Should You Choose?
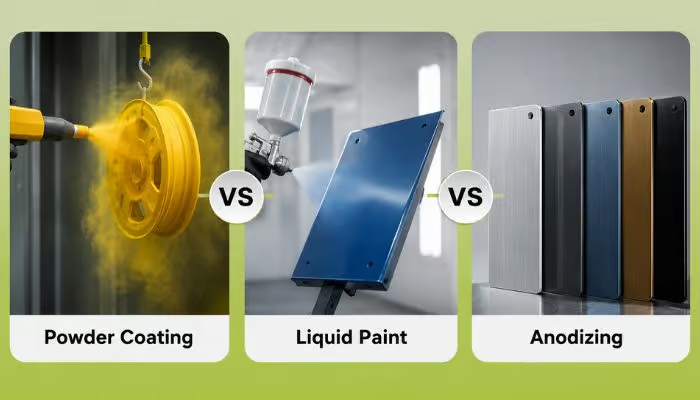
Powder coating, liquid paint, and anodizing are common surface finishing options for CNC parts, but they differ in material compatibility, film thickness, surface hardness, dimensional impact, curing requirements, and appearance.
The right finish depends on the part’s functional and cosmetic requirements. Powder coating is a strong choice for aluminum or steel parts that need durable color, texture, and general surface protection. Liquid paint works better when a thinner film, lower curing temperature, or specialized cosmetic effect is required. For aluminium parts where surface hardness, wear resistance, dimensional control, or a metallic appearance matters more, anodizing service is often the better option.
| Comparison | Powder Coating | Liquid Paint | Anodizing |
| Suitable materials | Aluminum, carbon steel, stainless steel | Broad range of metals and other substrates | Mainly aluminum |
| Finish structure | Relatively thick polymer film | Generally thinner organic film | Oxide layer formed from the aluminum surface |
| Appearance | Wide color, gloss, and texture options; usually opaque | Broad color and cosmetic options | Clear or dyed finish with metallic appearance |
| Dimensional impact | Film buildup can affect holes, fits, and mating surfaces | Usually lower buildup | Lower dimensional buildup, but anodic growth still matters |
| Wear resistance | Good abrasion and impact resistance | Depends strongly on the paint system | High surface hardness and wear resistance |
| Corrosion protection | Good with proper pretreatment and coating system | Depends on primer and paint system | Good corrosion resistance on aluminum |
| Heat requirement | Usually requires oven curing | Many systems cure at lower temperatures | Electrochemical process rather than oven curing |
| Best suited for | Durable colored CNC parts | Thin-film or heat-sensitive applications | Precision aluminum parts with metallic appearance |
How to Specify Powder Coating on a CNC Part Drawing or RFQ?
When requesting powder-coated CNC parts, send your drawing or CAD file together with the material, color, finish, coating areas, critical dimensions, and masking requirements. These details allows us to review the machining tolerances and finishing requirements together before production and identify features that may need coating allowance, masking, or post-coating control.
Include the following details where applicable:
- Base material: Aluminum alloy, carbon steel, stainless steel, or other substrate.
- Color: RAL code, customer color standard, or approved sample.
- Gloss and texture: Matte, semi-gloss, high-gloss, smooth, fine texture, or other specified finish.
- Powder coating type: Polyester, epoxy, hybrid, or another system when performance requirements make the chemistry important.
- Film thickness: Specify a target or acceptable range when thickness affects appearance, protection, or dimensional fit.
- No-coat areas: Clearly identify threads, bores, sealing faces, electrical contacts, mating surfaces, and other masked features.
- Critical dimensions: State whether tolerances apply before or after coating.
- Cosmetic surfaces: Identify appearance-critical faces and any restrictions on rack marks or surface defects.
- Performance requirements: Add adhesion, corrosion, UV, chemical, or other testing requirements when needed.
- Order details: Include part quantity and any approved finish samples or reference standards.
Conclusion
Powder coating is a practical finish for metal parts that need durable color, corrosion protection, and a consistent cosmetic surface, especially on aluminum and steel components. Its main limitation is that the coating becomes part of the finished geometry, so film thickness, masked features, mating surfaces, and curing requirements cannot be treated as an afterthought.
When the part design accounts for these factors from the beginning, powder coating can provide both reliable surface protection and a controlled appearance without compromising assembly or critical dimensions. The key is to specify the finish together with the machining requirements rather than treating coating as a separate final step.
FAQs
1. How long does powder coating last on metal parts?
Powder coating on metal parts can typically last about 10–20 years under normal outdoor conditions when proper pretreatment and an exterior-grade powder are used. Premium architectural polyester systems can offer warranties of up to 25 years, while heavy UV exposure, salt, chemicals, or abrasion can shorten service life.
2. How much does powder coating cost?
Powder coating typically costs about $5–$20 for small metal parts, while larger parts may be priced at roughly $2–$5 per sq. ft. The final cost depends on part size, order quantity, surface preparation, masking, coating type, color, and geometry complexity.
3. Does powder coating prevent rust?
Powder coating helps prevent rust by creating a protective barrier over carbon steel, but it does not make steel completely rust-proof. Corrosion can begin if scratches, chips, or poor edge coverage expose the base metal.
4. Can a powder-coated surface be repaired?
Yes. Powder-coated surfaces can be repaired, but the repair method depends on the size of the damage. Small scratches or chips can be cleaned, lightly prepared, and touched up with a compatible coating, while larger damaged areas usually require stripping and recoating to restore a uniform color, gloss, and texture.
5. Can you powder coat parts with threaded holes?
Yes, but precision threaded holes are normally masked before powder coating. Coating buildup on the thread flanks reduces clearance and can interfere with fastener fit.
6. What are alternatives to powder coating?
Common alternatives include liquid paint, anodizing, electroplating, electroless nickel, black oxide, and passivation. The best option depends on the base material, required thickness, corrosion resistance, wear resistance, conductivity, and appearance.
