
Choosing the right anodizing finish for CNC aluminum parts can directly affect durability, appearance, and long-term performance. Many projects face a common challenge: Type II and Type III anodizing offer different levels of protection, but selecting the wrong option may lead to unnecessary costs or performance issues.
This article explains the key differences between type II and type III anodizing, including coating thickness, wear resistance, dimensional impact, and application requirements. You will learn how each finish fits different CNC machining needs and make a more informed surface treatment decision.
What Is Anodizing and How Does It Work?

Anodizing is an electrochemical surface treatment that creates a protective aluminum oxide layer on aluminum parts. This process improves corrosion resistance, surface hardness, and appearance while maintaining aluminum’s lightweight properties. For CNC machined aluminum parts, anodizing provides a durable surface finish without adding a separate coating layer.
During anodizing, aluminum components are placed into an electrolyte solution and exposed to an electrical current. The process converts the aluminum surface into a controlled oxide layer instead of adding an external coating. This structure improves coating adhesion and helps protect parts from environmental exposure, wear, and surface damage.
What Is Type II Anodizing?
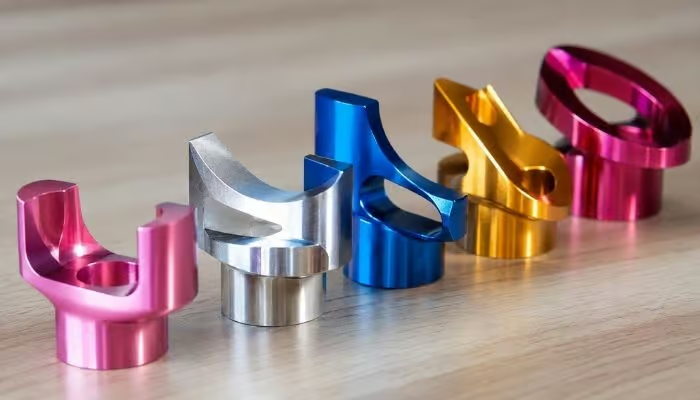
Type II anodizing is a sulfuric acid anodizing process that creates a protective aluminum oxide layer on the surface of aluminum parts. It is one of the most widely used anodizing methods for CNC machined aluminum components because it improves corrosion protection, surface appearance, and overall durability.
During the Type II anodizing process, the aluminum part acts as the anode and is placed into an electrolyte bath containing sulfuric acid. An electrical current passes through the solution, which triggers an electrochemical reaction that converts the aluminum surface into a controlled oxide layer. Unlike paint or external coatings, this oxide layer becomes part of the aluminum substrate and provides better adhesion during use.
The process usually includes several stages:
- Surface preparation: The aluminum part is cleaned and treated to remove oil, contaminants, and machining residues. Proper preparation helps achieve a consistent anodized finish.
- Anodizing treatment: The cleaned part is placed into the sulfuric acid electrolyte, where controlled electrical conditions create the oxide layer.
- Dyeing (optional): The porous oxide structure can absorb dyes, allowing different colors for appearance, identification, or product requirements.
- Sealing: The anodized surface is sealed to improve corrosion resistance and stabilize the finish.
Benefits and Limitations of Type II Anodizing
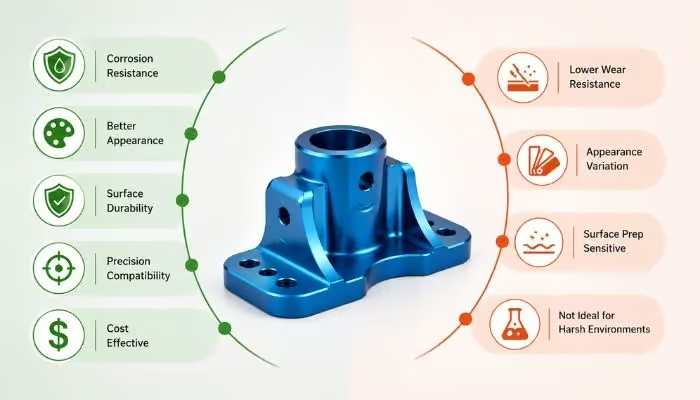
Type II anodizing offers a practical surface finishing solution for CNC machined aluminum parts by improving surface performance and appearance. However, this process also has certain limitations that should be evaluated based on the part’s function, operating environment, and expected performance requirements.
Benefits of Type II Anodizing:
Type II anodizing provides several practical advantages for CNC machined aluminum parts that require a stable and consistent surface finish. Its balanced performance makes it suitable for components where protection, appearance, and manufacturing requirements all need to be considered.
- Improved corrosion resistance: The anodized oxide layer protects aluminum surfaces from oxidation and environmental exposure. This makes the finish suitable for components used in indoor and outdoor applications where moisture and contaminants may affect bare aluminum.
- Enhanced surface appearance: The anodized surface provides a clean and consistent finish. The porous oxide structure allows dye absorption, which supports different color options and helps maintain visual consistency across multiple parts.
- Better surface durability: The anodized layer improves resistance to minor scratches, handling marks, and everyday surface wear during normal use.
- Suitable for precision aluminum parts: Type II anodizing works well with CNC machined components because the controlled finishing process can maintain the dimensional requirements needed for many assemblies.
- Practical finishing cost: The process provides functional surface protection and appearance improvement while maintaining a reasonable production approach for many aluminum components.
Limitations of Type II Anodizing:
Although Type II anodizing is suitable for many CNC machined aluminum parts, it also has certain limitations that should be considered during the finishing selection process. Understanding these limitations helps prevent performance issues when the component operates under specific mechanical or environmental conditions.
- Limited protection for extreme wear conditions: Components exposed to frequent mechanical contact, continuous friction, or abrasive materials may require a different finishing approach.
- Appearance can vary between aluminum alloys: Alloy composition, surface preparation, and machining conditions can influence the final color and surface consistency.
- Requires proper surface preparation: Machining marks, scratches, or inconsistent surface finishes may remain visible after anodizing because the process does not hide existing surface conditions.
- Not suitable for every operating environment: Parts exposed to aggressive chemicals, heavy mechanical stress, or demanding service conditions may require additional evaluation before selecting Type II anodizing.
Typical Applications of Type II Anodized Parts
Type II anodizing is widely used across industries that require aluminum parts with corrosion protection, consistent appearance, and reliable surface performance. These applications usually involve components that operate under normal conditions and require a balance between functional protection and surface aesthetics.
- Consumer electronics: Aluminum housings, electronic enclosures, device frames, and protective covers often use Type II anodizing to achieve a clean appearance and protect aluminum surfaces from oxidation and daily handling.
- Automotive applications: Aluminum interior trim parts, dashboard components, decorative panels, and non-critical auto parts may use Type II anodizing when appearance, corrosion resistance, and surface consistency are key requirements.
- Industrial equipment: Machine covers, equipment panels, aluminum brackets, mounting components, and protective enclosures commonly use Type II anodizing to improve surface protection during regular industrial operation.
- Medical equipment components: Medical device housings, instrument covers, aluminum frames, and equipment components often use Type II anodizing to maintain a clean finish and provide corrosion protection in controlled environments.
- Consumer products: Aluminum accessories, product frames, handheld device parts, and decorative aluminum components may choose Type II anodizing for color customization and consistent surface quality.
What Is Type III Anodizing?
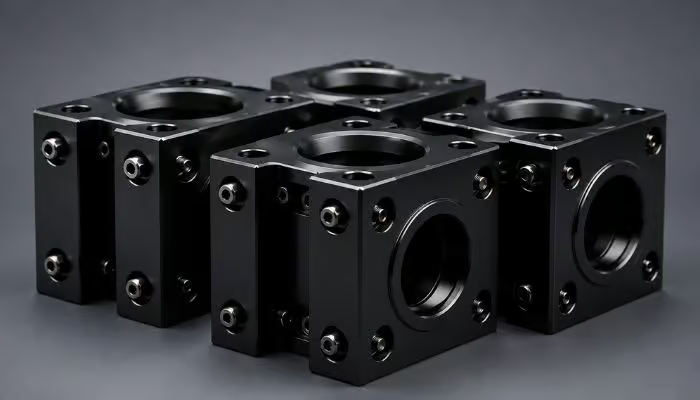
Type III anodizing, also known as hard anodizing, is an electrochemical surface treatment that creates a durable oxide layer on aluminum parts. It is commonly used for CNC machined aluminum components that require enhanced surface performance in more demanding operating conditions.
The process uses an electrolyte bath and controlled electrical current to convert the aluminum surface into a protective oxide layer. Before anodizing, the aluminum parts usually go through cleaning and surface preparation steps to remove contaminants and ensure a consistent finish. The final surface properties depend on factors such as aluminum alloy selection, machining quality, and process parameters.
Type III anodizing is often chosen for CNC components that need a more durable surface for long-term service. It is commonly applied to parts where wear resistance, surface protection, and functional performance are important considerations.
Benefits and Limitations of Type III Anodizing
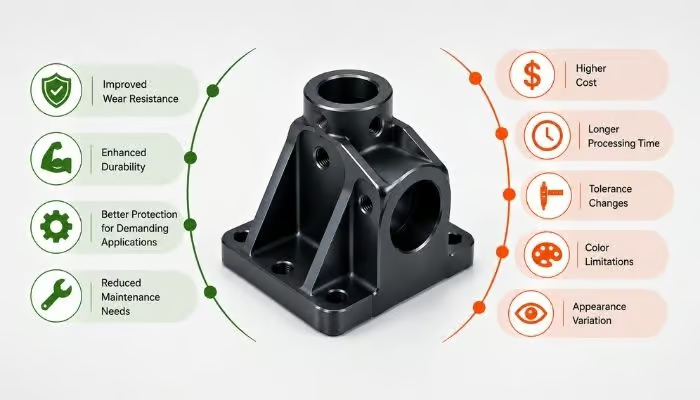
When CNC machined aluminum parts face higher mechanical demands, Type III anodizing can provide additional surface protection for long-term use. However, this process also comes with certain limitations that need to be evaluated based on part requirements, design conditions, and manufacturing considerations.
Benefits of Type III Anodizing:
Type III anodizing is commonly selected for aluminum components that require stronger surface protection during long-term operation. Its characteristics make it suitable for CNC machined parts that experience higher mechanical stress, repeated contact, or demanding working conditions.
- Improved wear resistance: The anodized surface helps reduce damage caused by friction, abrasion, and repeated contact, making it suitable for functional components with long service requirements.
- Enhanced surface durability: Type III anodizing helps aluminum parts maintain their surface condition when exposed to mechanical impact, handling, or continuous operation.
- Better protection for demanding applications: Components used in industrial equipment, mechanical systems, and precision assemblies can benefit from a more durable surface finish.
- Reduced maintenance needs: A more durable anodized surface can help minimize wear-related replacement and maintenance requirements during the service life of aluminum components.
Limitations of Type III Anodizing:
Selecting Type III anodizing requires more than considering its performance advantages. Engineers also need to evaluate factors such as production requirements, dimensional control, and application conditions before choosing this finish for CNC machined parts.
- Higher cost: Type III anodizing usually involves stricter process control and additional finishing requirements, which can increase overall processing costs for CNC machined components.
- Longer processing time: The additional treatment requirements may extend finishing lead times, especially for projects that require tight quality control or large production volumes.
- Tolerance changes: The anodized layer adds material to the aluminum surface, which may affect critical dimensions such as holes, threads, and mating surfaces if finishing allowances are not considered during machining.
- Color limitations: Type III anodizing typically focuses on functional performance, and achieving bright or decorative colors can be more challenging for certain applications.
- Surface appearance variation: Final appearance can be affected by aluminum alloy composition, machining marks, and surface preparation quality, making strict visual consistency more difficult in some projects.
Typical Applications of Type III Anodized Parts
Type III anodizing is commonly used for CNC machined aluminum parts that require higher surface durability, wear resistance, and long-term performance. These applications usually involve components exposed to friction, repeated contact, mechanical stress, or demanding operating environments.
- Wear-resistant mechanical parts: Machine components, tooling parts, fixtures, and aluminum mechanical assemblies often use Type III anodizing when repeated contact and surface wear may affect part performance.
- Precision aerospace components: Aircraft brackets, structural aluminum parts, and precision components can benefit from Type III anodizing when lightweight construction and durable surface protection are both required.
- Functional automotive parts: Engine components, transmission parts, and other aluminum auto parts may use Type III anodizing when they operate under repeated mechanical loads or harsh conditions.
- Medical and laboratory components: Surgical instrument parts, precision medical components, and equipment parts may require Type III anodizing when surface durability and long-term reliability are important.
- Hydraulic and industrial components: Hydraulic parts, mechanical housings, and industrial aluminum components exposed to friction or continuous operation can benefit from a harder anodized surface.
Type II vs Type III Anodizing: Key Differences Explained
Type II and Type III anodizing both provide protective oxide layers on aluminum surfaces, but they serve different performance requirements. The main differences involve coating thickness, surface properties, durability, appearance, and processing costs. Understanding these factors helps you select a more suitable finish for CNC machined aluminum parts.
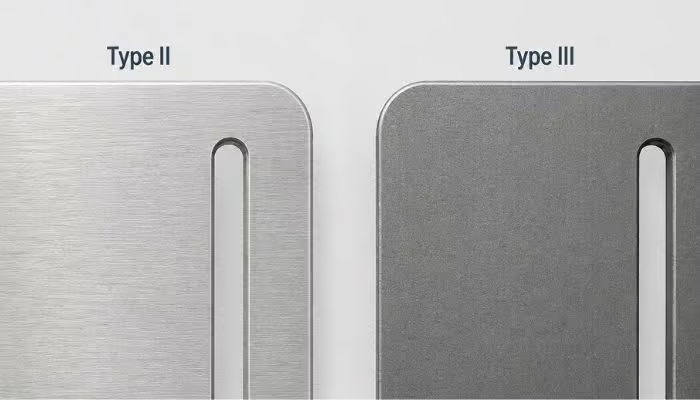
Coating Thickness
Coating thickness is one of the main differences between Type II and Type III anodizing. Industry references such as the Anodizing Reference Guide provide general coating thickness information for different anodizing classifications and their intended applications.
Type II anodizing typically creates a thinner oxide layer of around 1.8–25.4 μm (0.00007–0.001 inches). This thickness provides sufficient surface protection for aluminum parts that require corrosion resistance, appearance consistency, and general environmental protection.
Type III anodizing produces a much thicker oxide layer, commonly ranging from 12.7–115 μm (0.0005–0.0045 inches). The increased thickness improves the surface’s ability to withstand wear and mechanical exposure, making it suitable for more demanding CNC machined components.
Surface Hardness and Wear Resistance
Surface hardness and wear resistance directly affect how CNC machined aluminum parts perform under friction, repeated contact, and mechanical stress. Type II and Type III anodizing both improve aluminum surface properties, but their performance levels are different.
Type II anodizing generally provides a surface hardness of around 200–400 HV (Vickers hardness). This level of protection works well for CNC machined parts that require corrosion resistance, appearance consistency, and basic resistance against scratches or handling damage.
Type III hard anodizing typically reaches around 400–600 HV, creating a harder oxide layer with better resistance against abrasion and repeated mechanical contact. This makes it suitable for functional CNC parts such as tooling components, sliding assemblies, and industrial parts exposed to higher wear conditions.
Corrosion Resistance
Type II anodizing provides effective corrosion protection for CNC machined aluminum parts used in standard environments. Its thinner oxide layer helps prevent oxidation and surface degradation, making it suitable for components such as aluminum bearing housings, covers, and external parts that require general protection against moisture and daily exposure.
Type III anodizing offers stronger corrosion resistance due to its thicker and harder oxide layer. It is better suited for aluminum components exposed to harsh conditions, outdoor environments, chemical exposure, or long-term operation where additional surface protection is required. Compared with Type II, Type III provides a higher level of corrosion protection, but Type II remains a practical choice when standard environmental resistance is sufficient.
Color Options and Appearance
Type II anodizing usually provides more flexibility in color selection and surface appearance. Its thinner oxide layer allows dyes to create brighter and more varied finishes, including black, red, blue, green, gold, bronze, and clear anodized surfaces. It is commonly chosen for CNC machined aluminum parts where appearance, branding, and visual consistency are important.
Type III hard anodizing focuses more on functional performance than decorative effects. The thicker oxide layer typically creates a darker, more matte or satin-like appearance, with black, dark gray, and bronze being common choices. The denser coating structure also makes bright colors and complex decorative finishes more difficult to achieve.
Cost Differences
The cost difference between Type II and Type III anodizing mainly comes from process requirements, coating thickness, and production conditions. Type II anodizing generally requires less processing time and fewer treatment steps, making it a more economical option for CNC machined aluminum parts that need standard surface protection and appearance improvement.
Type III hard anodizing usually has higher processing costs because it requires tighter process control, longer treatment cycles, and additional steps to achieve a thicker, harder oxide layer. The final price can also vary depending on part size, quantity, aluminum alloy, surface preparation, and dimensional control requirements. For projects where wear resistance and extended service life are necessary, the additional finishing cost may be justified by the improved part performance.
Type II vs Type III Anodizing Comparison Summary
The following comparison highlights the key differences between Type II and Type III anodizing based on coating thickness, surface performance, appearance, cost, and common applications. This overview helps you quickly evaluate which finish better matches your CNC machined aluminum part requirements.
| Factor | Type II Anodizing | Type III Anodizing |
| Coating thickness | 1.8–25.4 μm | 12.7–115 μm |
| Surface hardness | Standard hardness | Higher hardness |
| Wear resistance | General protection | Enhanced durability |
| Corrosion resistance | Standard protection | Improved protection |
| Color options | More color choices | Limited colors |
| Appearance | Smooth, decorative | Darker, matte finish |
| Cost | Lower cost | Higher cost |
| Applications | Housings, covers, panels | Tooling, mechanical parts |
How Do Type II and Type III Anodizing Affect CNC Machined Parts?
The choice between Type II and Type III anodizing can influence more than surface performance. The anodizing process may also affect part dimensions, surface quality, and finishing requirements during CNC manufacturing. Understanding these factors helps prevent issues during assembly and final inspection.
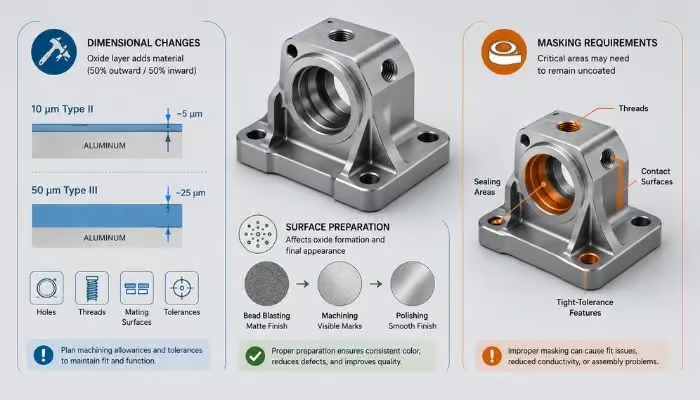
Dimensional Changes After Anodizing
Anodizing can slightly affect the dimensions of CNC machined aluminum parts because the oxide layer adds material to the surface. In general, around 50% of the coating thickness grows outward and 50% penetrates into the aluminum substrate.
For example, a 10 μm anodizing layer may increase the external dimension by approximately 5 μm, while a 50 μm Type III hard anodizing layer may add around 25 μm to the surface size. Precision features such as holes, threads, and mating surfaces should consider these changes during CNC machining and tolerance planning.
Surface Preparation Before Anodizing
Surface preparation directly affects the final appearance and consistency of anodized CNC machined parts. Machining marks, surface roughness, polishing methods, and cleaning processes can influence how the oxide layer forms and how the final finish looks.
Different surface preparation methods create different surface effects. For example, bead blasting can produce a uniform matte texture, while machining or polishing can create smoother finishes. Proper preparation helps achieve consistent color, reduce surface defects, and improve the overall quality of anodized aluminum parts.
Masking Requirements for Precision Components
Masking directly affects the function and assembly performance of CNC machined aluminum parts. Areas such as threads, contact surfaces, sealing areas, and tight-tolerance features may need to remain uncoated to maintain their original dimensions and surface properties.
Without proper masking, the anodized layer can change critical features, causing issues such as tighter thread fit, reduced electrical conductivity, or improper assembly between mating components. This consideration is especially important for precision parts with strict tolerance requirements, where even small dimensional changes can affect final performance.
How to Choose Between Type II and Type III Anodizing for CNC Machined Parts?
Choosing between Type II and Type III anodizing depends on the actual requirements of the CNC machined part, including its function, dimensional requirements, and material characteristics. The right choice should balance surface performance, production needs, and final application conditions rather than focusing on a single factor.
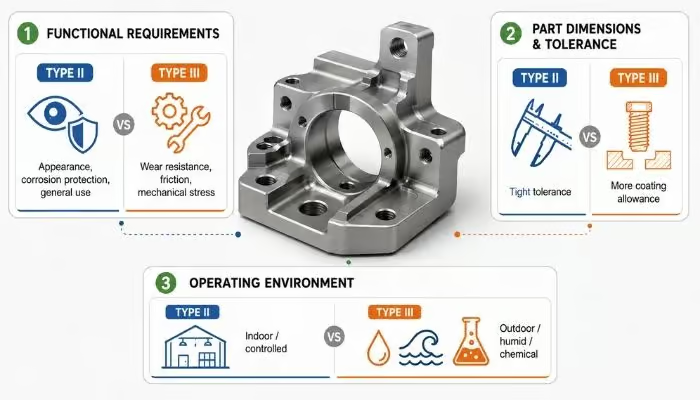
Functional Requirements
The function of the aluminum part is one of the most important factors when selecting an anodizing type. Components that mainly require corrosion protection, appearance improvement, or general surface protection are often suitable for Type II anodizing.
Parts exposed to friction, repeated contact, abrasion, or mechanical stress usually require the additional durability provided by Type III hard anodizing. Applications such as tooling components, industrial assemblies, and functional mechanical parts often benefit from the thicker and harder oxide layer.
Part Dimensions and Tolerance
Part tolerance requirements can help determine the suitable anodizing type for CNC machined parts. Type II anodizing is generally a better choice for precision components with tight dimensional tolerances because its thinner coating is easier to control during finishing.
Type III hard anodizing is more suitable for parts with less restrictive tolerance requirements or designs that allow coating allowance, especially when higher wear resistance is needed. Components used in demanding mechanical environments can benefit from a thicker coating when dimensional control has been considered during the design stage.
Operating Environment
The surrounding environment of a CNC machined part can influence the choice of anodizing type. For parts used in controlled indoor environments with limited exposure to moisture, temperature changes, or corrosive elements, Type II anodizing is often sufficient for daily protection requirements.
For components operating outdoors, in coastal areas, humid conditions, or environments with chemical exposure, Type III hard anodizing may provide a more suitable surface solution due to its thicker oxide layer. Environmental conditions should be evaluated alongside the part’s expected service life and maintenance requirements.
Conclusion
Choosing between Type II and Type III anodizing depends on the requirements of the CNC machined part, including surface appearance, wear resistance, dimensional control, and operating conditions. Type II anodizing works well for parts requiring decorative finishes and general protection, while Type III hard anodizing is better suited for components that need enhanced surface durability.
At DZ Making, we support customers with CNC machining and surface finishing solutions for custom aluminum parts. From material selection and machining processes to anodizing considerations, our team helps ensure each component meets the required functional and quality standards for its intended application.
FAQs
1. Is Type III anodizing more durable than Type II?
Yes. Type III anodizing forms a thicker and harder oxide layer, giving CNC machined aluminum parts better resistance to abrasion, friction, and repeated mechanical contact. Type II provides adequate durability when general surface protection, corrosion resistance, and appearance are the main requirements.
2. Can Type III hard anodizing be colored?
Yes. Type III hard anodizing can be dyed, but its thicker oxide layer generally limits color flexibility. Black, dark gray, and bronze are common choices. Type II anodizing is usually more suitable when a project requires brighter colors or a wider range of decorative finishes.
3. Does anodizing affect CNC machined part dimensions?
Yes. Anodizing changes final dimensions because part of the oxide layer grows outward from the original aluminum surface. This change becomes especially important for tight-tolerance features such as bores, threads, slots, and mating surfaces. Machining allowances or masking may be required before anodizing.
4. Which aluminum alloys are suitable for Type II and Type III anodizing?
Common CNC aluminum alloys such as 6061, 7075, 5052, and 2024 can generally receive Type II or Type III anodizing. However, alloy composition influences coating appearance, color consistency, and performance. The anodizing process should therefore be specified according to both the alloy and application requirements.
5. Which anodizing type is better for precision CNC machined components?
Neither type is universally better for precision components. Type II is easier to accommodate when tight dimensional control and a thinner coating are priorities. Type III is more appropriate when the component requires higher wear resistance, provided the machining allowance, masking, and final tolerances account for the thicker coating.
