
Waterjet Cutting Services
Custom waterjet cutting services support non-standard parts made from sheet and plate materials, including complex profiles, thicker sections, and drawing-specific dimensional requirements. DZ Making can continue with secondary CNC machining when the part includes precision holes, threads, or other features that require tighter control, helping complete the part to the required specifications.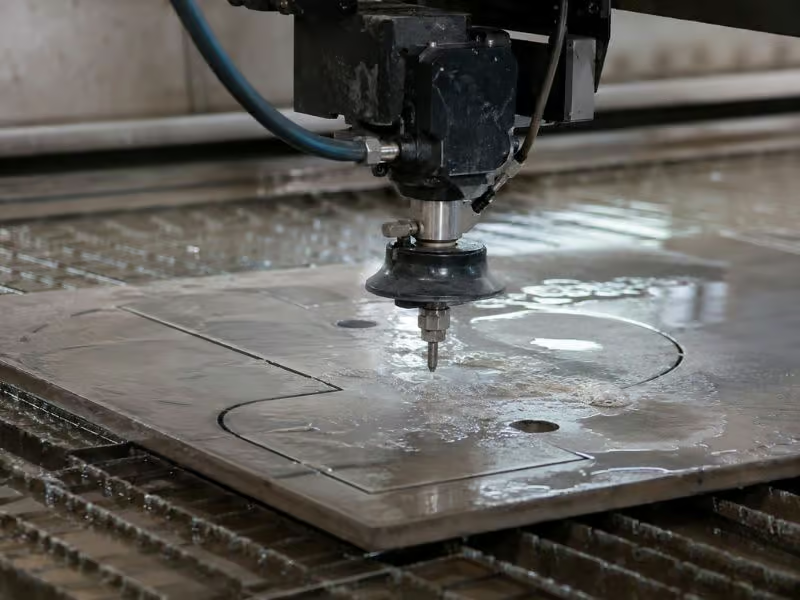
Waterjet Cutting Technical Specifications
| Specification | Reference Value |
|---|---|
| Cutting Method | CNC abrasive waterjet cutting |
| Cutting Pressure | Up to 60,000 psi / 4,140 bar |
| Profile Tolerance | ±0.25 mm / ±0.010 in |
| Kerf Width | Typically 1.0–1.6 mm / 0.040–0.062 in |
| Material Thickness | 1–150 mm / 0.04–6 in |
| Preferred Cutting Range | 1–75 mm / 0.04–3 in for routine production |
| Minimum Slot Width | Typically ≥1.0 mm / 0.040 in |
| Edge Condition | Fine to visible vertical striation; slight taper may occur on thicker sections |
| Drawing Formats | DXF, DWG, STEP, STP, PDF |
| Secondary Processing | CNC milling, drilling, tapping, grinding, deburring, and finishing |
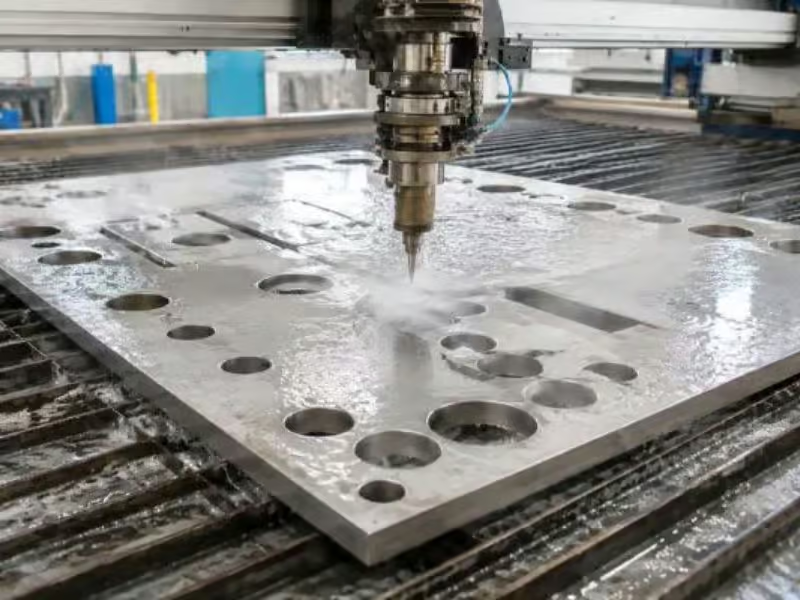
Custom Parts Suited to Waterjet Cutting
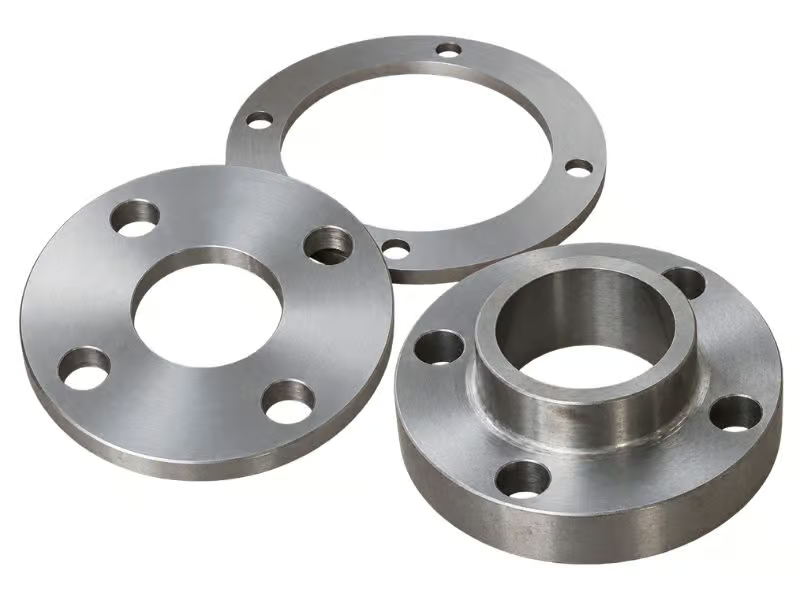
Flanges and Rings
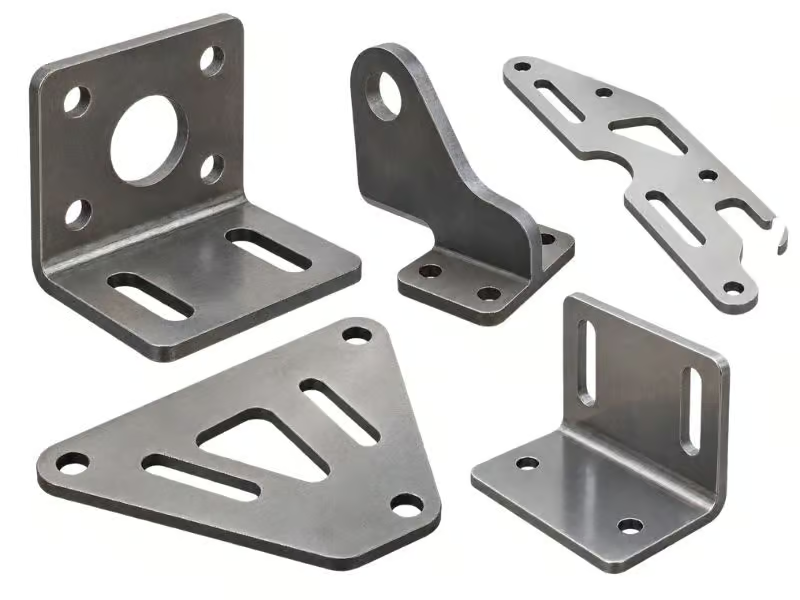
Mounting Brackets
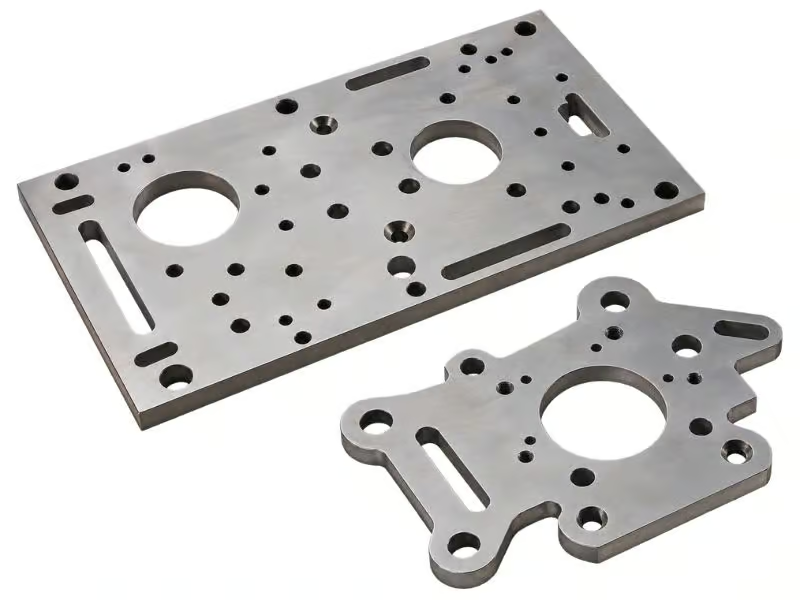
Base and Fixture Plates
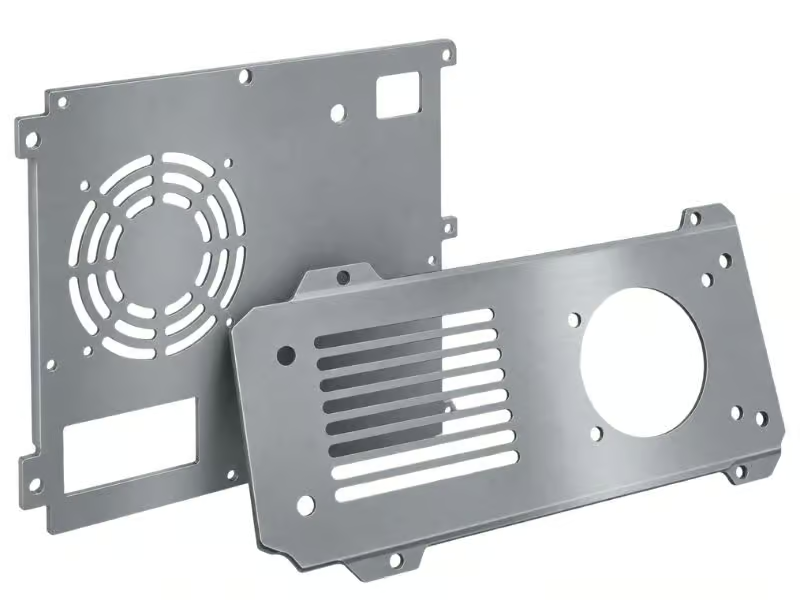
Covers and Panels
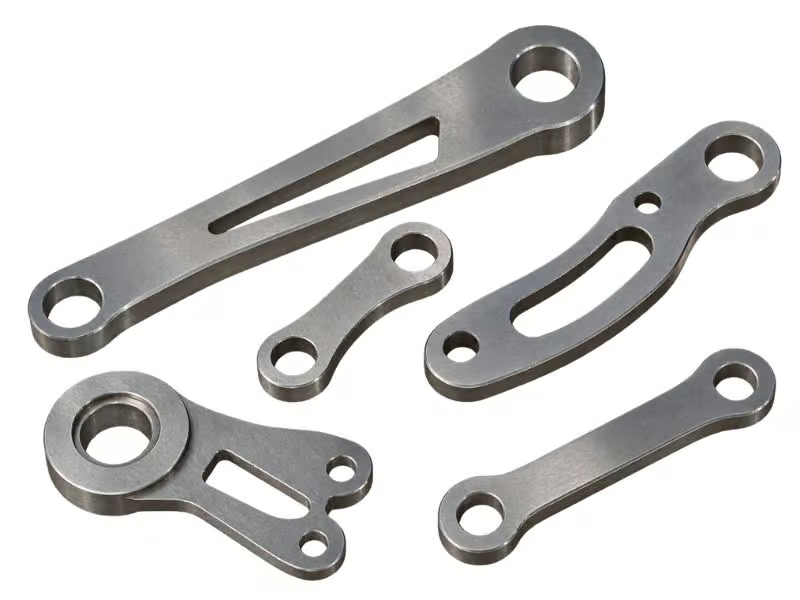
Links and Levers
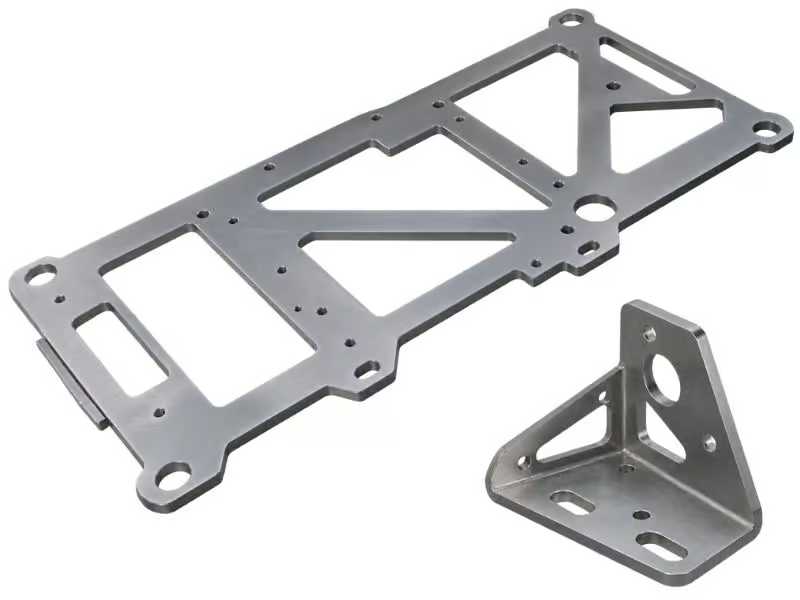
Frames and Supports
Need a Quote for Your Waterjet Cut Parts?
Why Choose Waterjet Cutting for Custom Parts?
Waterjet cutting is a practical choice for custom parts that involve thick plates, complex profiles, or materials that should not be exposed to cutting heat. It offers a flexible way to shape different materials while keeping the original material condition around the cut area.
No Heat-Affected Zone
Waterjet cutting uses high-pressure water and abrasive instead of heat, so the cut edge does not melt or form a thermal heat-affected zone. This helps protect the original material condition and reduces the risk of heat-related distortion.
Suitable for Thick Materials
Thicker plate often requires more flexibility than many thermal cutting methods can provide. Waterjet cutting can process substantial material thickness while maintaining the required profile, making it practical for heavy plates and structural parts.
Efficient Complex Profiles
Complex outlines, internal openings, slots, and irregular shapes can follow the programmed cutting path directly from CAD data. Waterjet cutting handles these geometries without dedicated dies, giving custom part designs greater freedom while reducing extra tooling.
Our Waterjet Cutting Equipment and Capabilities
Our waterjet systems use high-pressure abrasive cutting and CNC motion control to produce custom sheet and plate parts from digital drawings. The equipment supports complex profiles, different material thicknesses, efficient part nesting, and repeat production. For designs that include bevels or angled edges, 5-axis waterjet cutting adds the head movement needed to create features beyond a standard vertical cut.


Materials Suitable for Waterjet Cutting
Our waterjet cutting services handle a wide range of sheet and plate materials, each with different cutting behavior. Material grade, thickness, part geometry, and edge requirements are considered together to select a suitable cutting setup for the part.
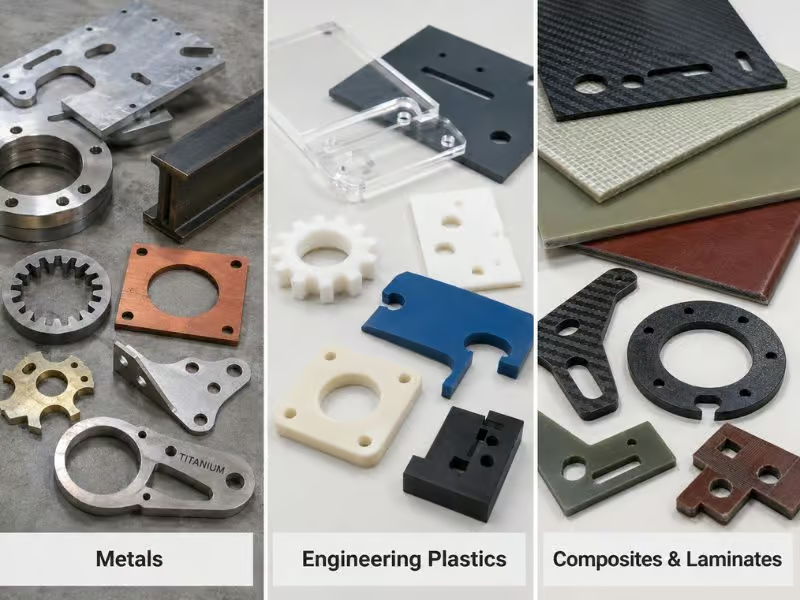
- Metals: Waterjet metal cutting handles aluminum, stainless steel, carbon steel, tool steel, titanium, copper, brass, and nickel alloys for custom plates, brackets, flanges, and profile-cut parts.
- Engineering Plastics: Acrylic, polycarbonate, PVC, UHMW, nylon, and POM respond well to waterjet cutting for custom sheet profiles without exposing the material to thermal cutting heat.
- Composites and Laminates: Carbon fiber, fiberglass, G10, phenolic laminates, and other reinforced sheets allow waterjet cutting to follow complex profiles.
Waterjet Cutting Accuracy and Process Control
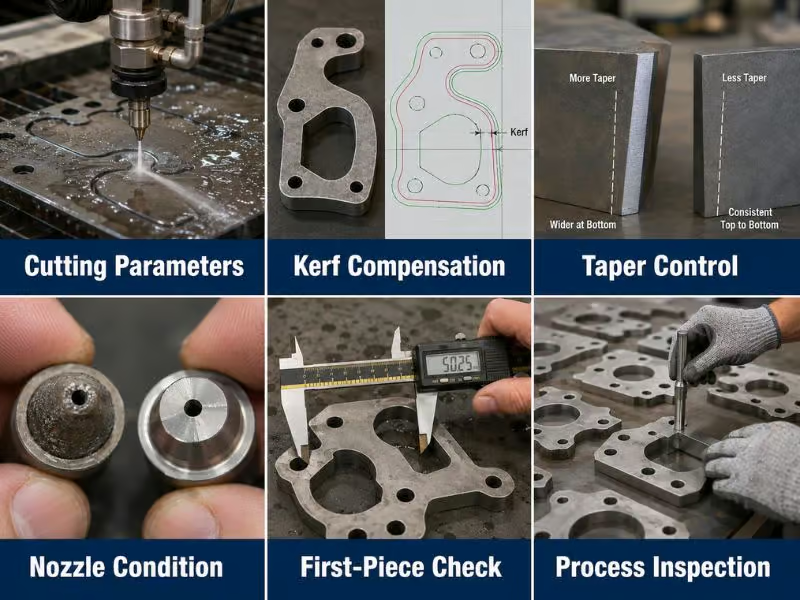
Waterjet cutting can maintain general profile tolerances around ±0.25 mm when cutting parameters match the material, thickness, geometry, and required cut quality. DZ Making controls cutting speed, kerf, taper, and toolpath settings around the drawing requirements, with critical dimensions checked during production for consistency.
- Cutting Parameters: Match speed, pressure, and abrasive feed to the material, thickness, and required cut quality.
- Kerf Compensation: Offset the programmed path to account for the cutting width and maintain profile dimensions.
- Taper Control: Adjust the cutting strategy to reduce top-to-bottom variation, especially on thicker plate.
- Nozzle Condition: Monitor nozzle wear and cutting condition to reduce changes in kerf width and edge quality.
- First-Piece Check: Verify critical dimensions and cut condition before continuing the production run.
- Process Inspection: Check specified features at planned stages to identify dimensional drift during batch production.
Secondary Processing for Waterjet-Cut Parts
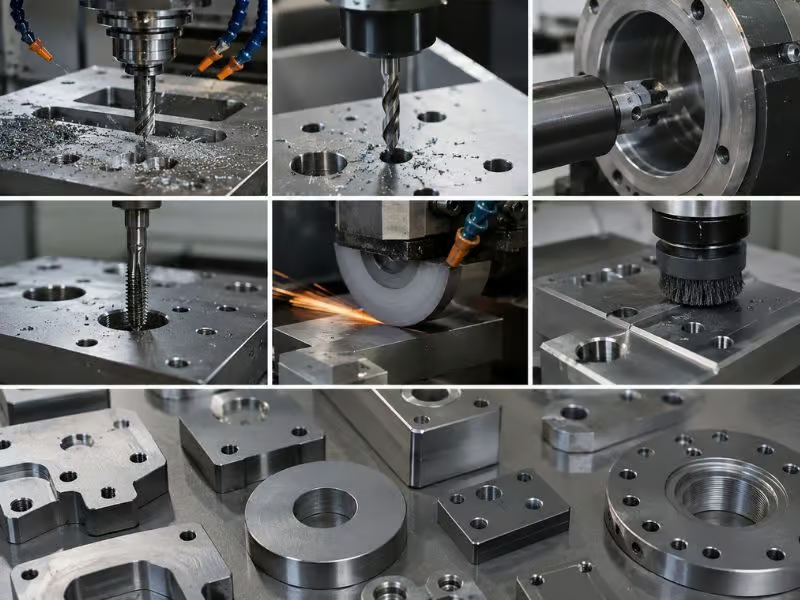
Waterjet cutting can establish the main profile before precision features are added in later operations. When a drawing includes features that the waterjet stage should not finish directly, machining allowance can be retained for the next process.
DZ Making can continue with CNC milling, drilling, boring, tapping, grinding, deburring, and other required operations after waterjet cutting. For parts that include threads, pockets, precision holes, datum faces, or sealing areas, these features can be completed after the main profile is cut, allowing the project to move from plate stock to a finished custom part within one coordinated manufacturing route.
What Do Global Customers Say about Our Waterjet Cutting Services?
From initial drawings to repeat orders, waterjet projects require steady coordination at every stage. These customer experiences highlight the areas that matter most during actual production.
DZ Making reviewed our drawings carefully and handled the waterjet cutting services around the required material and profile details. Communication stayed clear through sampling and production, and the finished parts matched the specifications we had confirmed.

We needed precision waterjet cutting for several plate components with different profiles and thicknesses. DZ Making kept the project organized from quotation through production, and the repeat parts remained consistent with our approved requirements.

Our project involved waterjet-cut parts that also required additional machining before assembly. DZ Making coordinated the cutting and follow-up operations well, which made the transition from prototype parts to the production order much easier to manage.

Design Considerations for Waterjet-Cut Parts
Waterjet-cut part design should leave enough room for the jet to enter, turn, and separate nearby features without weakening the surrounding geometry. Feature proportions and edge requirements are especially important on small or closely spaced details.
01
02
03
FAQs
Do waterjet-cut parts require deburring after cutting?
Not always, but deburring or edge finishing may still make sense depending on the material, cut quality, handling requirements, and final application. We can review the required edge condition and arrange additional finishing when the waterjet-cut parts need smoother or safer edges before assembly.
Yes, prototype quantities can help verify profile geometry, assembly fit, material choice, and any downstream machining requirements before larger production. For custom waterjet-cut parts, this stage also gives engineering teams a practical reference before approving the final production drawing.
A drawing, material grade, thickness, quantity, and key dimensional requirements are the main details needed for an RFQ. Adding surface requirements, secondary machining, inspection needs, and delivery expectations helps us evaluate the waterjet cutting route more accurately before quotation.
Yes, part identification can be considered when the drawing or purchase requirements specify how components should be marked or separated. Part numbers, batch identification, labels, or packaging references can make mixed-part and repeat waterjet cutting orders easier to receive and manage.
Packaging should match the part size, weight, material, surface condition, and risk of movement during transport. Waterjet-cut parts with finished surfaces, sharp profiles, or secondary machining may require separators, protective wrapping, reinforced cartons, or stronger export packaging to reduce contact damage in transit.
What Is Waterjet Cutting?
Waterjet cutting is a CNC-controlled process that uses a concentrated stream of high-pressure water to cut a programmed profile. Industrial systems generally use either pure water or an abrasive mixture, with abrasive waterjet cutting providing the additional cutting power needed for harder workpieces and many custom part applications.
A typical waterjet cutting workflow includes the following steps:
- Prepare the Part File: Convert the CAD drawing into a cutting program that defines the part geometry and required toolpath.
- Set the Cutting Parameters: Adjust pressure, cutting speed, abrasive flow, and related settings according to the material, thickness, and required cut quality.
- Generate High-Pressure Water: The pump raises the water pressure and sends the flow to the cutting head.
- Add Abrasive When Required: For harder materials, the cutting head introduces abrasive particles into the water stream to increase cutting power.
- Pierce the Workpiece: The jet penetrates the material at the selected start point before moving into the main profile.
- Cut the Programmed Profile: The cutting head follows the defined path to create the outer contour, openings, slots, and other required features.
- Inspect the Cut Part: Check specified dimensions and edge condition before the part moves to secondary processing, packaging, or shipment.
Waterjet Cutting vs Laser Cutting: Which Process Fits Your Part?
The main difference appears in the type of part each process handles most efficiently. Laser cutting suits many thinner metal sheets where fast cycle times, narrow kerfs, and fine profile detail matter. Waterjet cutting becomes more practical for thicker plates, heat-sensitive materials, reflective metals, and non-metallic workpieces because the cutting jet removes material without melting the edge or creating a heat-affected zone.
Process selection should then follow the drawing requirements. Consider material type, thickness, profile complexity, edge condition, tolerance, quantity, and any machining that follows the cutting stage. A thin sheet-metal panel produced in volume may favor laser cutting, while a thick stainless steel plate, titanium profile, or part that must retain its original material condition often fits waterjet cutting better.
Waterjet Cutting Aluminum vs Stainless Steel: What Changes in Production?
Waterjet cutting works well for both aluminum and stainless steel, but the two materials do not cut at the same rate. Aluminum is generally easier for the abrasive jet to remove, so similar profiles can often run at a higher cutting speed. Stainless steel usually requires a slower pass, particularly as the plate becomes thicker or the required edge quality becomes more demanding.
The difference becomes more noticeable on thick or complex waterjet-cut parts. Aluminum can usually maintain efficient profile cutting across larger sections, while stainless steel needs more careful control of cutting speed and abrasive flow to manage taper and edge striation. Exact alloy grade also matters, so 6061 aluminum, 304 stainless steel, and 316 stainless steel should not automatically receive the same process settings even when the part geometry and thickness are similar.
