
A part can look perfect in CAD and still become expensive, slow, or difficult to manufacture. Tight tolerances, awkward geometry, unsuitable materials, and unnecessary features can increase machining time, scrap risk, tooling needs, and inspection effort. Design for manufacturability helps prevent these problems before production begins.
This guide explains what DFM means, why it matters, its core principles, and the review process. You will also see its role in CNC machining, industry applications, sustainable manufacturing, and prototype-to-production planning.
What Is Design for Manufacturability (DFM)?
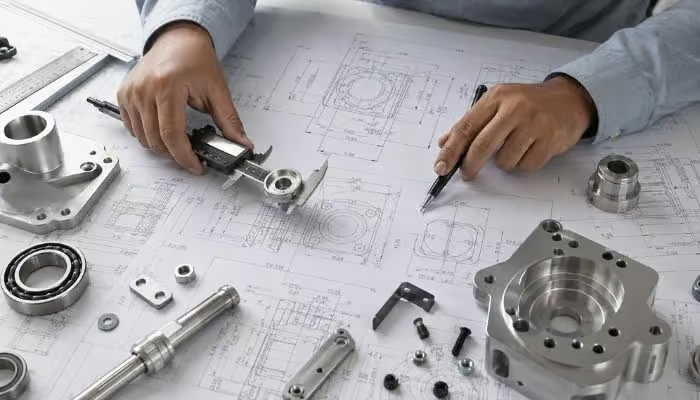
Design for manufacturability (DFM) is the practice of designing a part so it can be produced more easily, consistently, and economically. It considers manufacturing processes, materials, geometry, tolerances, tooling, and inspection before production begins.
A design may work perfectly in CAD but still create machining problems. Deep pockets, sharp internal corners, thin walls, or unnecessarily tight tolerances can increase cycle time, tooling requirements, and inspection effort. DFM identifies these issues early and adjusts the design without changing its intended function.
For CNC machining, this may mean increasing an internal radius, relaxing a non-critical tolerance, or simplifying a feature that requires extra setups. The goal is to balance part performance with practical manufacturing requirements.
DFM vs. DFA vs. DFMA
DFM focuses on making individual parts easier and more economical to manufacture. It considers factors such as geometry, material choice, tolerances, tooling access, and process capability. For CNC machining, DFM often addresses features that increase setup time, machining difficulty, or inspection effort.
DFA (design for assembly) focuses on making a product easier to assemble. It aims to reduce unnecessary components, simplify fastening methods, improve part orientation, and shorten assembly steps. The main goal is to make assembly faster, simpler, and less prone to errors.
DFMA combines DFM and DFA into one broader design approach. It evaluates both how each part will be produced and how the complete product will be assembled. This makes DFMA especially useful for products with multiple components, while DFM remains more directly relevant to individual custom CNC parts.
Why Is Design for Manufacturability Important?
Design for manufacturability helps you identify production problems before they become expensive changes on the shop floor. By reviewing geometry, tolerances, materials, tooling, inspection, and process limits early, you can reduce unnecessary manufacturing effort while protecting the function and performance of the finished part.

Reduce Manufacturing Costs
DFM lowers cost by removing features that add machining time without adding functional value. Deep pockets, excessive surface finish requirements, multiple setups, and unnecessarily tight tolerances can all increase cutting time, tooling needs, and inspection work.
For CNC parts, even a small design change can affect cost. A larger internal radius may allow a shorter, more rigid end mill. A relaxed, non-critical tolerance may eliminate extra finishing passes or additional inspection. DFM focuses on removing avoidable costs rather than simply making the cheapest possible part.
Prevent Production Issues
A manufacturability review can reveal problems that are easy to miss in CAD. Thin walls may deflect during cutting, deep features may restrict tool access, and complex geometry may require unstable workholding or extra setups.
Finding these risks before machining allows you to modify the design before material, tooling, and production time are committed. Early DFM reduces the chance of scrap, rework, dimensional instability, and repeated process adjustments.
Improve Quality and Consistency
DFM improves consistency by matching the design to the capability of the selected manufacturing process. Practical tolerances, stable geometry, clear datums, and accessible inspection features make it easier to reproduce critical dimensions from part to part.
This becomes more important as production quantity increases. A prototype may be adjusted manually to meet a difficult specification, but repeated production needs a stable process. A manufacturable design makes quality easier to control rather than relying on repeated correction after machining.
Shorten Lead Times
DFM can shorten lead time by reducing unnecessary machining operations, special tooling, complex fixturing, and repeated design revisions. A part that fits standard tools and practical setups can usually move through programming, machining, and inspection with fewer interruptions.
Early review also reduces back-and-forth after a quotation or first article inspection. When the drawing, CAD model, tolerances, and manufacturing method are aligned from the beginning, the project can move from design to prototype and production with fewer avoidable delays.
The Core Principles of Design for Manufacturability
The core principles of DFM focus on simplifying production without compromising part function. A manufacturable design should match the selected process, use suitable materials, avoid unnecessary complexity, apply realistic tolerances, and support stable quality control. These principles help reduce machining effort, production risk, and avoidable cost.

Simplification
Simplification removes design features that increase manufacturing difficulty without improving part performance. Complex contours, deep narrow cavities, unnecessary undercuts, and excessive transitions can require additional tools, setups, or slower machining strategies.
For CNC parts, simpler geometry often means better tool access and more stable cutting. This does not mean removing necessary functional features. Instead, you should question whether each feature needs its current shape, depth, location, or level of complexity.
Standardization
Standardization in DFM reduces unnecessary variation in dimensions, tooling, materials, and purchased components. Standard hole sizes, thread forms, corner radii, and material stock dimensions usually fit established manufacturing processes more easily than highly customized specifications.
For CNC machining, standard features can reduce special tooling and frequent tool changes. Common thread specifications and readily available stock sizes may also simplify material sourcing and production planning. Standardization becomes especially valuable when the same precision CNC part moves from prototype machining into repeat production.
Material Selection
Material selection is a core part of design for manufacturability because material properties directly affect machining difficulty, tool wear, cycle time, and manufacturing cost. A material should meet functional requirements while remaining suitable for the selected manufacturing process.
For example, aluminum 6061 generally offers better machinability than hardened steel or nickel-based alloys. Harder materials may require lower cutting speeds, more rigid tooling, and longer machining time. DFM therefore considers strength, corrosion resistance, temperature requirements, availability, and machinability together rather than selecting material based on mechanical properties alone.
Process Optimization
Process optimization in design for manufacturability (DFM) means aligning the part design with the capabilities and limits of the selected manufacturing process. The goal is to make production practical, repeatable, and cost-effective without changing the required function of the part.
In CNC machining, this principle considers tool access, workholding, setup count, machining sequence, and equipment capability. A design that fits the process can avoid unnecessary special tooling, repeated repositioning, and excessive machining time. Process optimization therefore helps improve manufacturability while reducing production complexity and risk.
Tolerance Control
In DFM, the tolerance control principle is to specify the widest tolerance that still satisfies the part’s functional requirements. DFM avoids applying unnecessarily tight tolerances across the entire drawing because tighter limits can increase machining difficulty, inspection time, scrap risk, and production cost.
The design should distinguish critical features from non-critical ones. Fits, sealing surfaces, bearing locations, and alignment features may justify tighter control, while less critical dimensions can use broader limits. Good DFM tolerance control balances functional accuracy with actual manufacturing capability, helping the part remain both precise where necessary and practical to produce.
Quality Control Integration
Quality control integration is a DFM principle that brings inspection and error prevention into the design stage instead of treating them as separate tasks after production. The design should make critical features easy to measure, reduce ambiguity in inspection, and support consistent results across repeated production runs.
Good DFM also considers how datums, tolerances, and inspection access affect verification. Features that are easier to inspect and less prone to assembly or measurement errors can improve process consistency and reduce rework. This makes quality control part of manufacturability rather than a final check after machining is complete.
How Does the DFM Process Work?
The DFM process reviews a design step by step to confirm that it can be produced with the selected manufacturing method at an acceptable cost, quality level, and production risk. It starts with design requirements, then evaluates process suitability, geometry, materials, tolerances, and cost drivers before the design is optimized and validated for production.

Step 1: Review Design Requirements
A DFM review starts by defining what the part must achieve in actual use. The review covers functional dimensions, material requirements, loads, mating features, surface finish, expected quantity, and inspection needs. This step separates essential specifications from flexible ones, which helps protect part performance while creating opportunities to improve manufacturability and control unnecessary production cost.
Step 2: Select the Manufacturing Process
The next step evaluates which manufacturing process best matches the part geometry, material, tolerance, and production quantity. CNC milling, turning, 5-axis machining, casting, and combined processes each have different capabilities and limitations. DFM aims to align the design with the strengths of the selected process, reducing the need for unnecessary operations, special tooling, or complicated setups later in production.
Step 3: Evaluate Geometry and Materials
Geometry and material are reviewed together because both strongly influence manufacturability. Features such as thin walls, deep pockets, small internal radii, inaccessible surfaces, or difficult hole locations can complicate machining. Material hardness, toughness, and thermal behavior may add further challenges. This DFM step identifies design and material combinations that could increase tool wear, deformation, machining time, or dimensional instability.
Step 4: Check Tolerances and Finishes
The review then checks whether tolerances and surface finish requirements are necessary for the part’s intended function. Very tight tolerances or fine finishes can require slower machining, additional finishing passes, and more detailed inspection. DFM places precision where it affects fit, sealing, alignment, motion, or performance, while allowing broader limits on non-critical features to avoid unnecessary manufacturing complexity and cost.
Step 5: Identify Cost and Production Risks
The next stage identifies features that increase manufacturing cost or reduce process stability. Common risks include multiple setups, special cutters, difficult workholding, hard-to-inspect features, and secondary operations. DFM evaluates these issues before production starts, because a minor difficulty during prototyping can become a significant cost, quality, or consistency problem when the same machining operation is repeated across a larger production run.
Step 6: Optimize and Validate the Design
The final step turns DFM findings into practical design changes and confirms that the revised part still meets its functional requirements. Geometry, tolerances, materials, feature orientation, or machining strategy may be adjusted before prototyping or first-article validation. The design is ready for production when it remains functional, manufacturable, measurable, and suitable for the intended production volume.
How Does DFM Apply to CNC Machining?
DFM applies to CNC machining by adapting the part design to real machining limits, tooling access, workholding, tolerances, and setup requirements. A design may be technically machinable but still create unnecessary cost, long cycle times, or dimensional risk. CNC-focused DFM aims to remove those issues before programming and production begin.

Tool Access and Part Geometry
DFM first checks whether cutting tools can physically reach every machined feature with enough clearance and rigidity. Hidden surfaces, narrow channels, deep cavities, or obstructed features may require long-reach tools, smaller cutters, or additional machining orientations.
When access is poor, DFM may change feature orientation, increase clearance, open restricted areas, or simplify surrounding geometry. These adjustments allow more direct tool paths and reduce dependence on special tooling, long tool overhang, or extra setups.
Internal Corners and Deep Features
Internal geometry is reviewed against the physical shape and reach of CNC cutting tools. Sharp internal corners may require very small end mills, while deep narrow pockets can force long tools that are more vulnerable to deflection, chatter, and poor chip evacuation.
DFM can increase internal corner radii, widen narrow pockets, or reduce unnecessary pocket depth while preserving functional surfaces. These changes allow larger and shorter cutters, improve machining stability, and often reduce the number of passes needed to complete the feature.
Wall Thickness and Part Stability
DFM also evaluates whether the part will remain stable while material is being removed. A thin wall may meet the final CAD dimensions but still deflect during machining, especially when surrounding material no longer provides support.
The review may increase wall thickness, change the sequence of material removal, add temporary support geometry, or redesign nearby features to improve stiffness. DFM therefore considers the condition of the part during machining, not only its final shape, which helps control distortion and dimensional variation.
| Material | General Minimum Wall Thickness |
| Aluminum | ~1.0–1.5 mm |
| Stainless steel / mild steel | ~1.5–2.5 mm |
| Engineering plastics | ~2.0–3.0 mm |
Tolerances and Surface Finishes
Tolerance and finish requirements are reviewed according to actual functional needs. DFM identifies dimensions that affect fit, sealing, alignment, bearing location, or motion, then separates them from features that do not need the same level of precision. General tolerance frameworks such as ISO 2768-1 and surface texture standards such as ASME B46.1 provide the reference basis for these decisions.
Non-critical tolerances may be widened, and fine surface finishes may be limited to functional areas. This prevents the entire part from requiring additional finishing passes, slower machining, or detailed inspection simply because a few features need tighter control.
Setups and Fixturing
DFM examines how the part can be located, clamped, and accessed throughout the machining process. Features spread across many directions may require repeated repositioning, while weak or irregular surfaces can make stable workholding difficult.
The design may be adjusted by changing feature orientation, creating practical clamping surfaces, improving datum locations, or arranging features so more operations can be completed in one setup. This application of DFM reduces setup complexity and helps maintain positional relationships between machined features.
DFM Examples Across Different Industries
DFM changes with industry requirements because manufacturability depends on how a part will function, what risks matter most, and how consistently it must be produced. Aerospace parts may prioritize weight and dimensional stability, while medical or electronics components may place greater emphasis on small features, surface quality, or inspection. The same DFM principle therefore leads to different design decisions across applications.
Aerospace

Lightweight structures, thin walls, complex geometry, tight tolerances, and difficult-to-machine materials define many DFM challenges in aerospace parts. Weight reduction may require deep pockets, thin ribs, or extensive material removal, which can increase deformation and make dimensional control more difficult. A DFM review balances structural performance with tool access, machining stability, datum planning, and practical feature geometry.
- Structural brackets
- Avionics housings
- Aircraft fittings
- Actuator components
- Sensor mounts
- Lightweight frames
Automotive

Production consistency and machining efficiency become especially important when automotive components move from prototypes into repeated production. Long cycle times, multiple setups, and unnecessarily tight tolerances can add high cost across larger quantities. DFM examines whether features can be standardized, operations simplified, and precision concentrated on interfaces that affect fit, motion, sealing, or assembly.
- Drive shafts
- Transmission housings
- Gearbox parts
- Suspension brackets
- Engine mounts
- Brake components
Medical

Close dimensional control, small complex features, surface requirements, and inspection accessibility shape many DFM decisions for medical parts. Compact geometry can restrict both cutting-tool access and measurement access, while thin features may become unstable during machining. The review checks whether critical dimensions can be produced and verified consistently, then looks for non-functional geometry that can be simplified without affecting the required performance.
- Surgical instrument parts
- Medical device housings
- Instrument handles
- Diagnostic equipment parts
- Precision interfaces
- Implant-related components
Robotics

Complex motion systems create a different set of manufacturability challenges for robotics components. Bearing seats, motor interfaces, joints, sensor mounts, and lightweight structures may span several faces, increasing repositioning and fixturing complexity. DFM evaluates feature orientation, datum relationships, and non-critical geometry to reduce setup effort while preserving positional accuracy. It can also help determine whether 3-axis or multi-axis machining provides the more practical production route.
- Robot arm joints
- End-effector parts
- Motor mounts
- Bearing housings
- Gearbox housings
- Sensor brackets
Electronics

Thin-wall enclosures, heat-dissipation structures, precision openings, cosmetic surfaces, and secondary finishes are common DFM considerations for electronics parts. Deep cavities may limit tool access, while extensive material removal can cause thin walls to distort. A manufacturability review examines wall thickness, internal radii, connector openings, heat-sink geometry, and feature spacing. It should also account for later processes such as anodizing, coating, or bead blasting when dimensions or visible surfaces may be affected.
- Electronic enclosures
- Heat sinks
- Connector housings
- Camera housings
- Control panels
- Precision mounting plates
How Does DFM Support Sustainable Manufacturing?
DFM supports sustainable manufacturing by reducing unnecessary material use, scrap, rework, machining effort, and avoidable process complexity during the design stage. Instead of treating sustainability as a separate activity, design for manufacturability improves how efficiently a part moves from raw material to finished component while still meeting its functional and quality requirements.
Reduce Material Waste
Material efficiency starts with part geometry and stock selection. Oversized blanks, excessive material removal, and unnecessarily bulky features can increase both raw material consumption and machining time. DFM reviews whether the part can achieve the required strength and function with more efficient geometry, suitable stock dimensions, and less unnecessary material removal.
This matters especially for large aluminum, stainless steel, or titanium parts where a significant portion of the starting stock may otherwise become chips. Better design decisions can improve material utilization without reducing the mechanical performance required from the finished component.
Minimize Scrap and Rework
Scrap does not only waste material; it also repeats the machining, inspection, tooling, and handling already invested in the part. Thin sections, unstable features, unclear tolerances, or difficult inspection requirements can increase the chance that a finished component falls outside specification.
DFM reduces this risk by identifying manufacturability problems before production begins. A more stable geometry, realistic tolerance scheme, accessible measurement features, and clearer datum structure can reduce rework and make dimensional results easier to reproduce across multiple parts.
Improve Machining Efficiency
Machining efficiency improves when the design avoids operations that add little functional value. Extra setups, deep narrow pockets, specialized cutters, excessive finishing passes, and difficult tool access can all extend cycle time and increase the resources required to produce each part.
A DFM review looks for opportunities to simplify toolpaths, reduce repositioning, improve cutter access, and avoid unnecessary machining operations. The goal is not simply faster cutting, but a manufacturing route that achieves the required result with fewer avoidable steps.
Choose Materials More Responsibly
Material selection in sustainable DFM should balance mechanical performance, machinability, availability, service life, and processing requirements. Using a material with performance far beyond the real application can increase machining effort, tool wear, cost, and material waste without providing practical value.
For example, 6061 aluminum may be a more practical choice than 7075 when very high strength is not required, because 6061 is widely available and generally easier to machine. Similarly, 304 stainless steel may be sufficient instead of 316 when the part does not need the higher corrosion resistance associated with chloride-rich environments. In engineering plastics, POM can be more practical than PEEK when extreme temperature or chemical resistance is unnecessary.
Prototype DFM vs. Production DFM: What Changes?
Prototype DFM focuses on proving function and manufacturability with maximum design flexibility, while production DFM focuses more heavily on repeatability, cycle time, tooling, inspection, and total unit cost. The same CNC part may therefore require different design priorities as it moves from a few prototypes into recurring production.
During prototyping, the design may still change after testing. A complex feature or extra setup can be acceptable when only a small number of parts are required. Prototype DFM mainly checks whether the design can be machined reliably and whether critical dimensions, materials, and functional features perform as intended. Flexible workholding and general-purpose tooling may also be practical at this stage.
Production changes the priorities. Repeated setups, long toolpaths, difficult inspection, or unnecessary tight tolerances become more important when the same operations are performed across many parts. Production DFM looks for ways to stabilize the machining process, reduce cycle time, simplify fixturing, standardize tools, and make inspection more repeatable.
| DFM Factor | Prototype DFM | Production DFM |
| Main goal | Validate design and function | Achieve repeatable production |
| Design changes | Frequent changes are acceptable | Design should be largely stable |
| Tooling | Flexible or standard tooling | Tool life and consistency matter more |
| Fixturing | General-purpose setups may work | Dedicated fixtures may become practical |
| Cycle time | Lower priority | Major cost consideration |
| Tolerances | Confirm functional requirements | Optimize critical vs. non-critical limits |
| Inspection | Validate key dimensions | Build a repeatable inspection plan |
| Cost focus | Total prototype cost | Cost per part and process stability |
Conclusion
Design for manufacturability (DFM) helps turn a functional design into a part that can also be produced consistently, economically, and with fewer avoidable risks. By reviewing process choice, geometry, materials, tolerances, inspection, tooling access, and production volume early, DFM reduces the chance that a good CAD model becomes a difficult or expensive manufacturing problem.
For CNC machining projects, the value of DFM becomes clearer as parts move from prototype to repeat production. If your design involves tight tolerances, complex geometry, multiple setups, or challenging materials, an early manufacturability review can help identify practical improvements before machining begins. DZ Making can review your drawings and CAD files, provide DFM feedback, and support CNC milling, turning, 5-axis machining, and related production requirements.
