
Part marking gives CNC-machined parts a clear identity throughout production, inspection, assembly, and service. Without a defined marking method, part numbers, serial data, revision details, or traceability codes can become difficult to verify once components move between machining, finishing, inventory, and final assembly.
This guide explains part marking for CNC machining, including common methods, material and finishing considerations, applicable standards, drawing requirements, and selection criteria. It will help you specify marks that remain readable and durable while matching the part geometry, surface condition, and production requirements.
What Is Part Marking for CNC Machining?
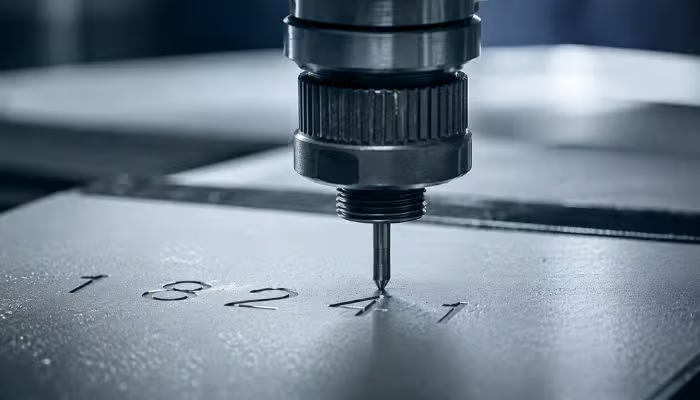
Part marking for CNC machining refers to adding identification information to a machined component so the part can be recognized throughout its use. When the information is applied directly to the part surface, the process is commonly known as direct part marking (DPM). The mark can contain letters, numbers, part numbers, serial numbers, batch codes, revision information, logos, symbols, or machine-readable codes such as Data Matrix.
Unlike a separate label or tag, direct part marking makes the identification part of the component itself. The information can be created by changing the surface, removing a controlled amount of material, creating small impressions, or transferring printed information onto the finished part. In CNC manufacturing, marking is typically specified as an additional operation based on the drawing or product identification requirements.
Why Is Part Marking Important for CNC Machined Parts?
Part marking keeps essential identification attached to a CNC-machined component as it moves through production, inspection, assembly, storage, and service. It gives operators, inspectors, engineers, and maintenance teams a consistent reference for confirming which part they are handling.
- Improve Part Identification: Similar CNC parts can look almost identical even when they differ in dimensions, material grade, revision, or function. A visible part number or identifier makes those differences easier to recognize without relying only on packaging or visual inspection.
- Enable Production Traceability: Serial numbers, lot codes, and other identifiers can connect a finished component with its production history. This allows teams to trace the part back to a specific batch, manufacturing record, or inspection stage when verification is required.
- Reduce Assembly Errors: Clear markings help operators distinguish parts with similar geometry, left- and right-hand versions, or components intended for different assembly positions. Orientation marks and reference symbols can also reduce confusion during installation.
- Maintain Product Information: Important identification remains available after the component leaves the machine shop. Part numbers, revision references, model information, and other defined markings preserve the data needed for maintenance, replacement, inventory control, and repeat production.
8 Common Part Marking Methods for CNC Machined Parts
CNC part marking methods create identification through different surface processes, from laser treatment and mechanical cutting to chemical etching and ink transfer. The selected process determines whether the finished mark appears as surface contrast, a recessed feature, an indentation, or a printed graphic, allowing CNC-machined parts to carry serial numbers, part numbers, logos, inspection information, and traceability codes.
Laser Marking
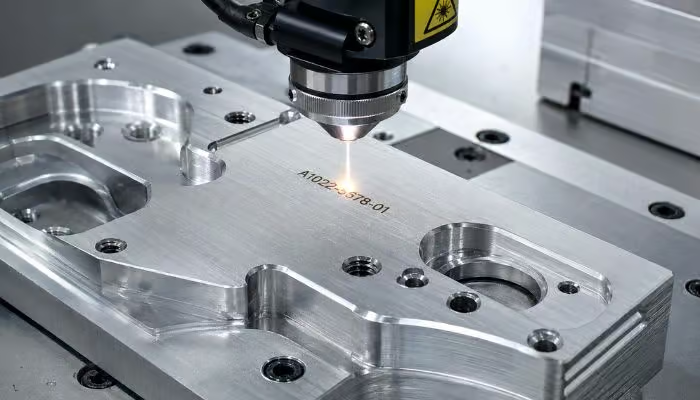
Laser marking uses controlled laser energy to create a visible change on the part surface while keeping the original surface profile largely intact. Depending on the material and laser settings, the beam can produce oxidation, annealing, discoloration, or a localized change in texture that creates contrast without intentionally cutting a deep recess.
For serial numbers, part numbers, logos, QR codes, and Data Matrix codes, this process can reproduce small characters and dense information with clearly defined edges. Programmed laser paths also allow the part marking data to change from one CNC-machined part to the next without replacing physical tooling, which is useful for serialized or variable identification.
Laser Engraving
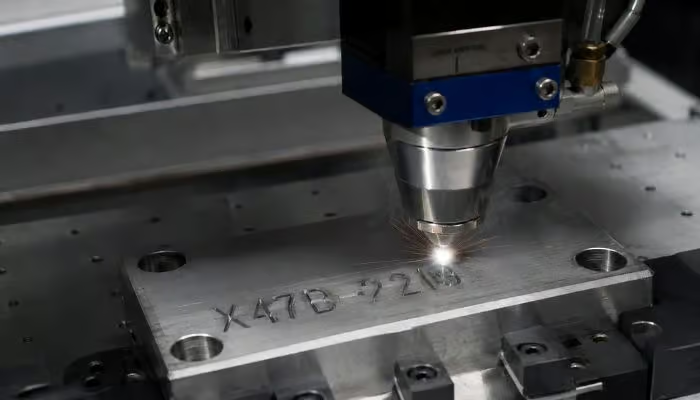
Laser engraving removes a controlled layer of material to form text, symbols, or graphics below the original part surface. The laser repeatedly scans the programmed area and ablates material until the engraving reaches the required depth, so power, scanning speed, focal position, and pass count all influence the resulting groove.
Because the information extends below the surrounding surface, engraved serial numbers and part IDs remain physically present even after some handling or moderate surface wear. This physical depth also distinguishes laser engraving from surface-focused laser marking and makes it suitable when a drawing calls for a permanent recessed identifier, detailed lettering, or an engraved logo.
CNC Engraving
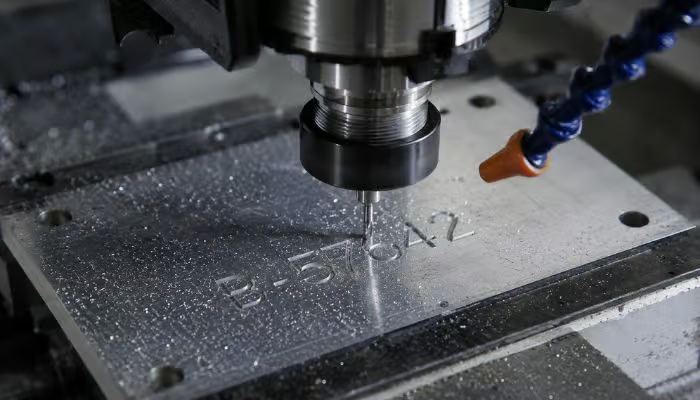
CNC engraving creates identification with a cutting tool following a programmed toolpath across the machined surface. Small engraving cutters, V-bits, or end mills remove material to produce letters, numbers, scales, reference lines, or symbols at a defined position and depth.
When engraving is included in the original CNC machining setup, the machine can use the same part datums and coordinates to position the mark relative to holes, edges, pockets, or other features. Cutter diameter, tip geometry, toolpath strategy, and engraving depth then determine how narrow, sharp, or pronounced the finished characters appear.
Dot Peen Marking
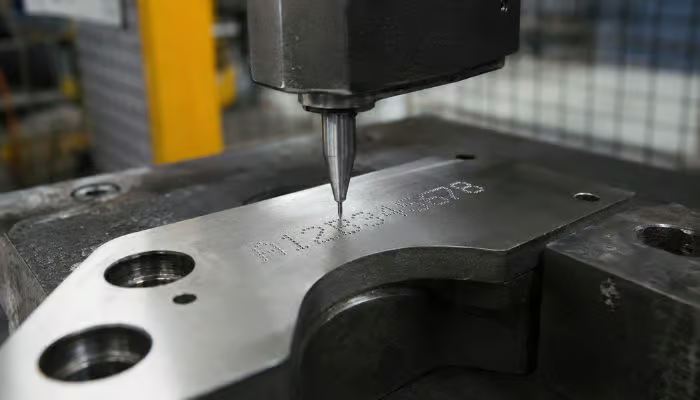
Dot peen marking builds characters from closely spaced indentations created by a rapidly actuated stylus. Each impact plastically displaces a small amount of surface material, and controlled movement of the part marking head arranges those impressions into letters, numbers, symbols, or machine-readable identification.
Serial numbers, lot codes, equipment IDs, and other traceability information are common uses for dot peen marking on industrial CNC parts. Its closely spaced impacts leave a recognizable dotted pattern and a shallow physical texture, while programmable marking equipment can update identification data automatically between individual components.
Chemical Etching
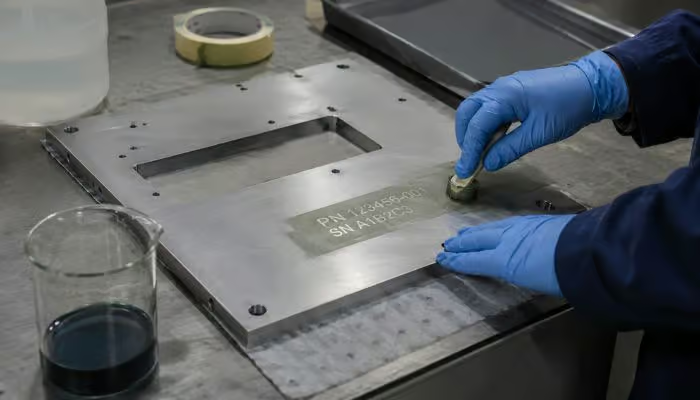
Chemical etching forms identification through a controlled reaction between the exposed workpiece surface and an etching agent. A stencil, mask, or resist protects the surrounding area and leaves the required characters or graphics exposed. The chemical process then alters those selected regions to create the mark.
Fine lettering, identification symbols, scales, and relatively detailed graphics can be produced without applying significant cutting force to the component. Etching depth and visual definition depend on the chemistry, exposure conditions, and treated surface, so chemical etching generally creates a shallow mark rather than the more pronounced recess associated with mechanical engraving.
Screen Printing
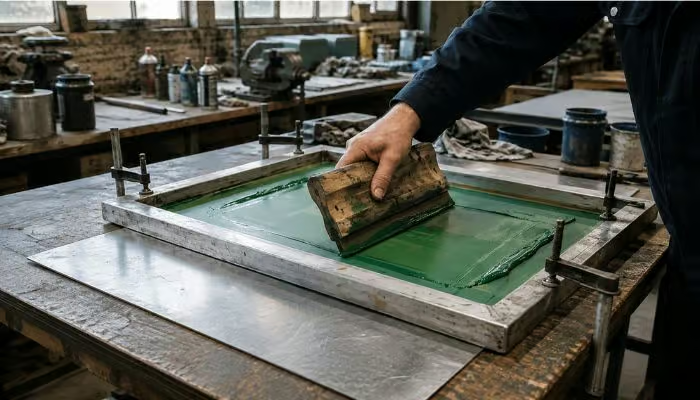
Screen printing deposits ink onto a CNC part through selected openings in a patterned mesh screen. A squeegee moves the ink across the screen and forces it through the open image area, transferring the required text or graphic onto the surface underneath.
Larger logos, warning information, operating symbols, labels, and color-coded graphics are well suited to this type of surface marking, particularly when the available area is relatively broad and accessible. Screen printing can also cover solid areas of color efficiently, while ink formulation, surface preparation, and curing conditions influence adhesion and the consistency of the finished print.
Pad Printing
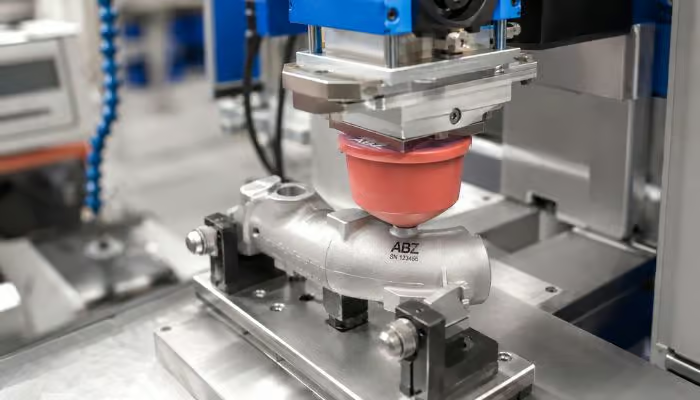
Pad printing uses a flexible silicone pad to pick up an ink image from an engraved plate and transfer it onto the component. The pad deforms as it contacts the workpiece, allowing the printed image to reach curved, slightly recessed, or geometrically irregular areas that are difficult to contact evenly with a flat printing screen.
Curved housings, rounded features, and small localized marking areas can therefore carry logos, symbols, labels, or fine text without requiring the printing surface to lie on a single flat plane. This ability to conform to three-dimensional geometry gives pad printing a wider geometric reach than screen printing for certain CNC-machined parts.
Ink Stamping
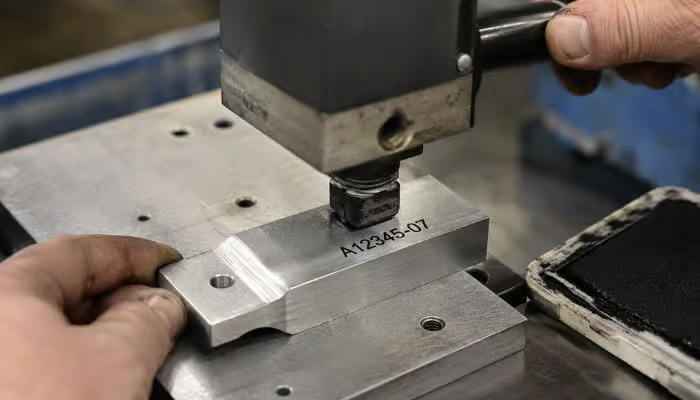
Ink stamping transfers text or symbols directly from an inked stamp onto the surface of the machined component. The stamp carries a fixed character set, logo, number pattern, or simple graphic and creates the mark through a single contact with the designated area.
Inspection marks, date codes, batch references, operator identifiers, and other basic production information fit this straightforward part marking method well. Consistent results depend on the stamp design, ink coverage, contact pressure, and placement, while the fixed transfer format makes ink stamping better suited to simple repeated information than to complex or individually programmed graphics.
CNC Part Marking Method Comparison Table
Part marking methods differ not only in how they create identification, but also in the depth they produce, the type of data they handle, the surfaces they can reach, and the limitations they introduce. Comparing these factors side by side makes it easier to see where each method fits within CNC machining applications.
| Method | Mark Form | Physical Depth | Variable Data | Geometry Fit | Typical Identification | Main Constraint |
| Laser Marking | Surface contrast/change | None to minimal | High | Flat and accessible curved surfaces | Serial numbers, Data Matrix, fine text | Contrast depends on material response |
| Laser Engraving | Laser-removed recess | Controlled recess | High | Accessible flat, angled, or curved areas | Permanent IDs, logos, serial numbers | Removes material and adds local heat |
| CNC Engraving | Machined groove | Controlled recess | Moderate to high | Areas with cutter access | Part numbers, scales, arrows | Tool size limits very fine detail |
| Dot Peen Marking | Impact indentations | Shallow indentations | High | Rigid, stylus-accessible surfaces | Serial and lot identification | Dotted texture and local deformation |
| Chemical Etching | Chemically altered recess | Very shallow | Low | Surfaces suitable for masking | Fine text, symbols, scales | Requires masking and chemical control |
| Screen Printing | Applied ink | None | Low | Broad, relatively flat areas | Logos, warning text, legends | Fixed artwork and exposed ink |
| Pad Printing | Applied ink | None | Low | Curved and irregular surfaces | Small logos and symbols | Limited image area and registration |
| Ink Stamping | Applied ink | None | Moderate | Simple accessible surfaces | Dates, inspection marks, short codes | Limited detail and wear resistance |
Part Marking Considerations for Common CNC Materials
Part marking needs to match the behavior of the base material, not just the information that needs to appear on the part. Hardness, ductility, heat response, reflectivity, and resin composition can all change mark depth, contrast, edge quality, and the risk of damaging the surrounding surface, so each material brings a different set of marking considerations.
Aluminum
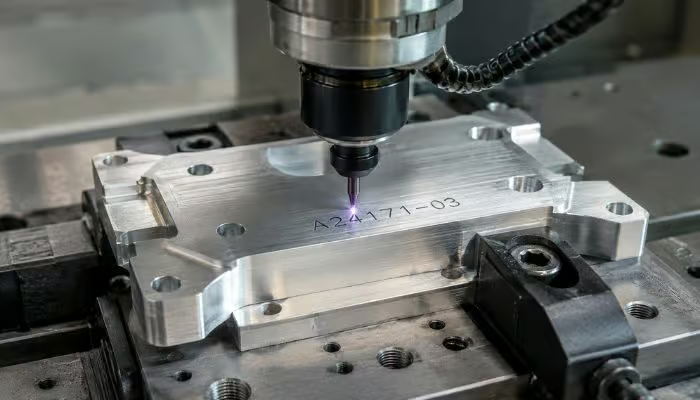
For aluminum part marking, the material’s low hardness makes engraving relatively easy, but deep cuts can raise material along the character edges. Thin walls, narrow ribs, shallow pockets, and small bosses are particularly sensitive features in aluminum parts, because local material displacement can distort the section or interfere with nearby geometry.
Keep engraved or indented marks shallow around thin aluminum features, and check that no raised lip forms around the characters. Small laser marks also need alloy-specific settings because 6061, 7075, and other grades can show different contrast under the same exposure. The goal is a clean mark without relying on excessive penetration to make it visible.
Stainless Steel
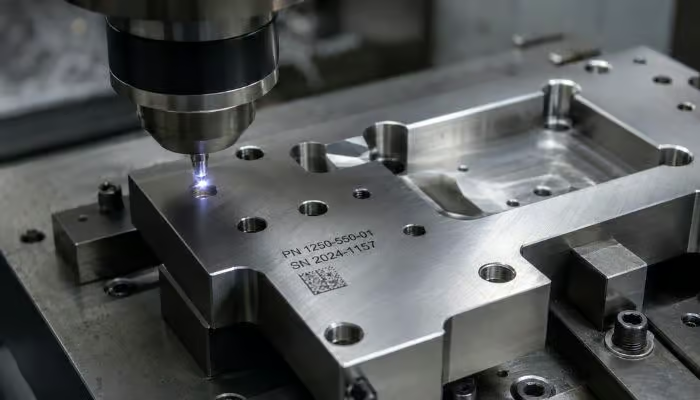
In stainless steel part marking, the surrounding surface condition often matters more than mark depth alone. Aggressive engraving can leave torn edges, and excessive laser energy can create a wider discolored zone than the actual characters. This becomes especially noticeable on stainless steel parts with visible or corrosion-sensitive surfaces.
Limit the marking action to the intended character area and avoid roughness or heat tint spreading beyond it. Fine engraved text also needs a sharp cutter because worn tooling can round corners and widen narrow strokes on the harder surface. Here, surface cleanliness and character definition matter more than simply cutting deeper.
Steel and Tool Steel
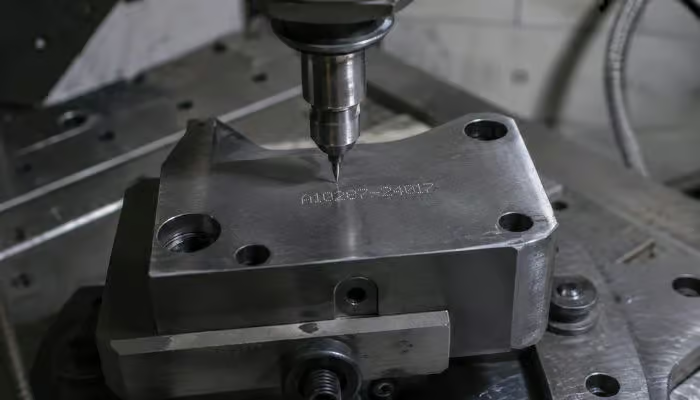
Steel brings a different issue because hardness can change dramatically after heat treatment. A dot peen setting that produces a clear indentation on annealed steel may barely penetrate hardened tool steel, while an engraving cutter can wear much faster after the steel part reaches its final hardness.
Set the marking depth and character geometry according to the final hardness condition, not the material designation alone. On hardened tool steel, wider strokes and less delicate lettering usually retain definition better than very fine characters. The actual heat-treated condition therefore affects whether the mark stays complete and consistent.
Titanium
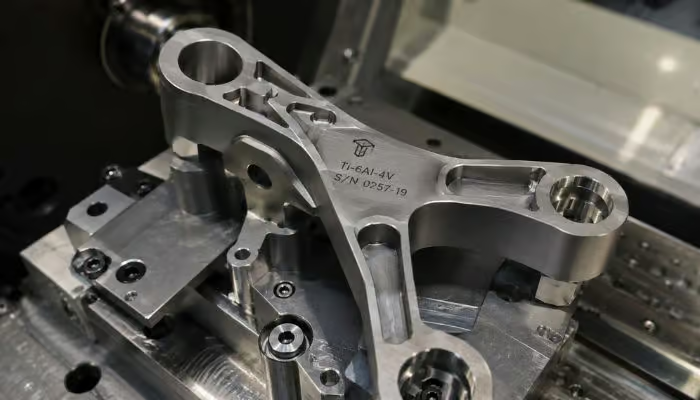
Titanium needs tighter control of concentrated heat than aluminum or ordinary carbon steel. Repeated laser passes can enlarge the thermally affected area, while deep mechanical engraving can add unnecessary material removal close to the precision geometry.
Deep marks on the titanium part should stay away from thin edges, sealing lands, highly stressed sections, and other function-critical areas. When identification sits close to these features, the marking process should use only the heat or depth needed to maintain readability. Keeping the mark localized avoids unnecessary surface alteration simply to achieve a darker or deeper appearance.
Brass and Copper
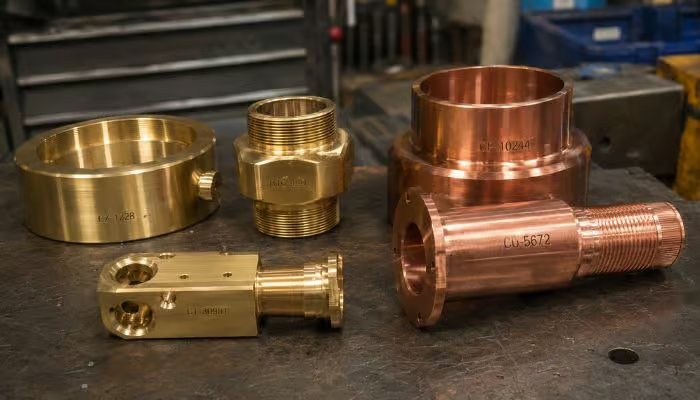
Copper-rich materials create two very specific marking problems: high thermal conductivity during laser processing and material smearing during mechanical cutting. Copper can carry heat away from the part marking zone quickly, which can weaken contrast, while its ductility can cause fine engraved strokes to drag or develop small rolled edges.
Watch the character edges closely on copper and soft brass, especially on narrow lettering and small symbols. A sharp cutter and moderate cut depth reduce smearing and burr formation, while laser settings need to account for the material’s reflectivity and rapid heat dissipation. The critical issue here is preserving crisp line definition.
Engineering Plastics
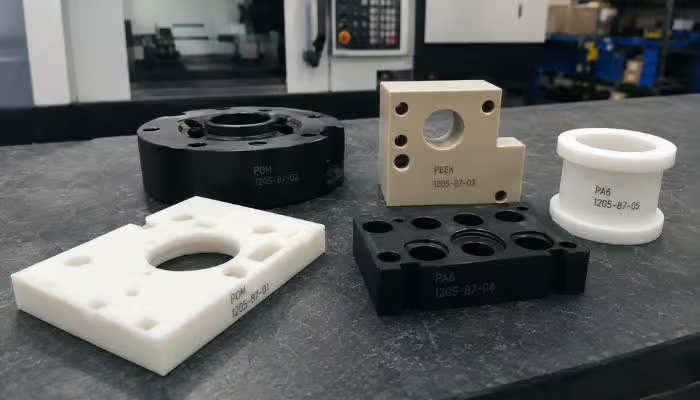
Engineering plastics need grade-specific part marking parameters because pigments, fillers, reinforcement, and additives can all change the result. PEEK, POM, nylon, and polycarbonate can darken, lighten, foam, melt, or char differently even under similar laser conditions.
Verify the mark on the exact production grade, including its color and reinforcement, before fixing the final process settings. Softer polymers such as some nylons can smear during engraving, while brittle or heavily filled grades can chip around small characters. For fine text and machine-readable codes, the material must preserve narrow gaps and small features without melting them together or breaking their edges.
How Can Finishing Affect Mark Visibility and Durability?
Surface finishing can change a CNC part mark even when the marking process itself has been completed correctly. The final visibility and durability depend on whether the finish changes contrast, adds material over the mark, covers it with a film, or removes part of the marked surface. These different surface changes influence identification in different ways.
Contrast Changes With Anodizing
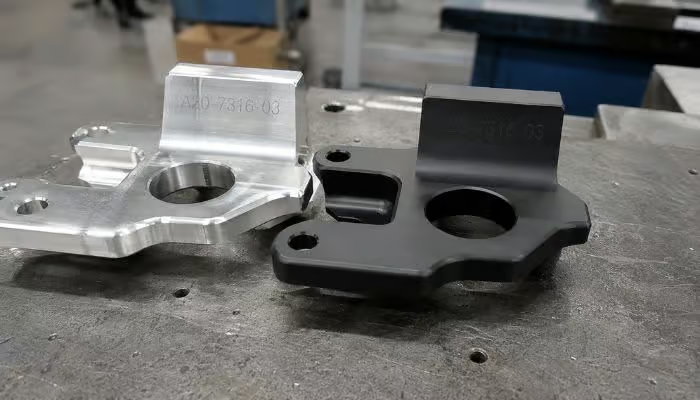
Anodizing mainly affects a mark by changing the visual background around it. The oxide layer alters color, reflectivity, and texture, so part marking visibility can increase or decrease after anodizing. The key visibility issue is whether the finished mark remains sufficiently distinct from the anodized surface around it.
The part marking sequence becomes important because it determines which layer carries the identification. A mark produced before anodizing is treated together with the surrounding aluminum, whereas laser marking or engraving performed afterward modifies the finished anodized surface. Post-anodizing marking can create strong contrast, but any process that cuts through the oxide layer also changes the surface protection at the marked location.
Shallow Mark Coverage From Plating
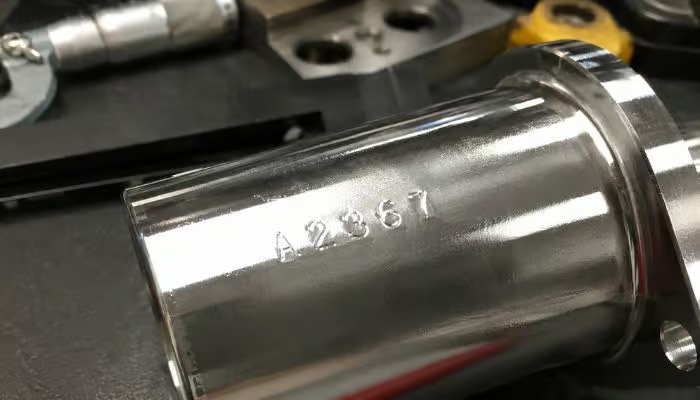
As plating builds on the sidewalls and bottom of an engraved or etched mark, the open width and effective depth gradually decrease. When the deposited layer becomes significant relative to the original mark depth, shallow characters can lose sharp edges and readable relief.
This makes original engraving depth especially important for plated parts. A deeper recess leaves enough geometry after deposition to preserve the characters, while very fine or shallow features have much less tolerance for buildup. Durability decreases when plating leaves too little physical depth for the identification to remain clearly defined after subsequent handling or wear.
Visibility Under Paint and Powder Coating
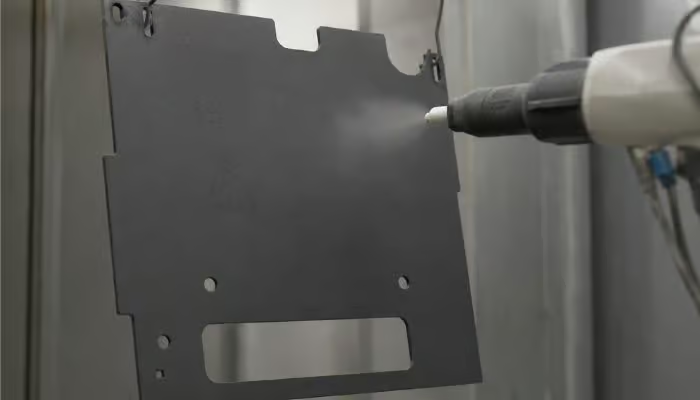
Once paint or powder coating is applied, an opaque finish can hide the original surface and alter the contrast around a CNC part mark. Surface-level laser marks, printed graphics, and other low-relief details can disappear beneath the finish, while similar coating and mark colors can make text, symbols, or codes difficult to distinguish.
The durability issue is different for marks created in the coating itself. Printed text, surface graphics, or other identification that exists only on the finished layer depends on that coating staying attached and intact. If the paint or powder layer chips, scratches, or peels away, any mark carried only by that layer can be lost with the finish. Deeper identification in the base material does not depend entirely on coating retention.
Mark Detail Loss Through Blasting and Polishing
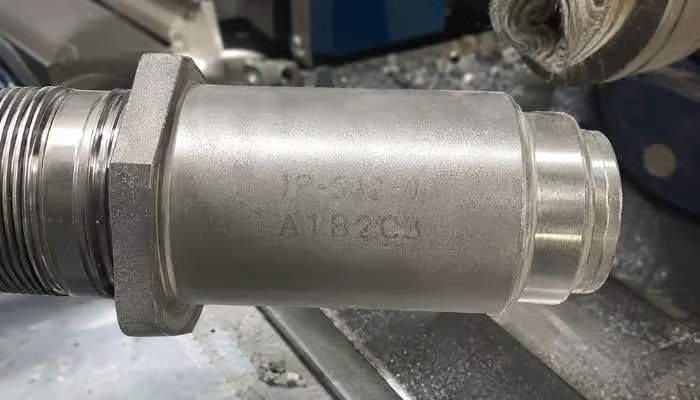
Blasting can reduce part marking detail by changing the texture around and inside the marked area. The process can soften sharp engraving edges, widen very fine recesses, and reduce the difference in texture between the mark and the surrounding surface. As the engraved edges become less distinct, the mark may remain physically present but lose visual definition and become harder to read.
Polishing removes material more directly. As the surface is leveled, shallow engraving and etched features lose depth, narrow strokes become less defined, and small characters can gradually disappear. This can reduce mark durability once enough material is removed to weaken the physical geometry that keeps the identification readable.
How to Choose a Part Marking Method for CNC Parts?
Choosing a part marking method for CNC parts means matching the marking process to the actual identification requirements and production conditions. Rather than starting with laser marking, engraving, or dot peen marking, first define what the mark must achieve, where it can fit on the part, how many parts require marking, and whether the information changes during production.
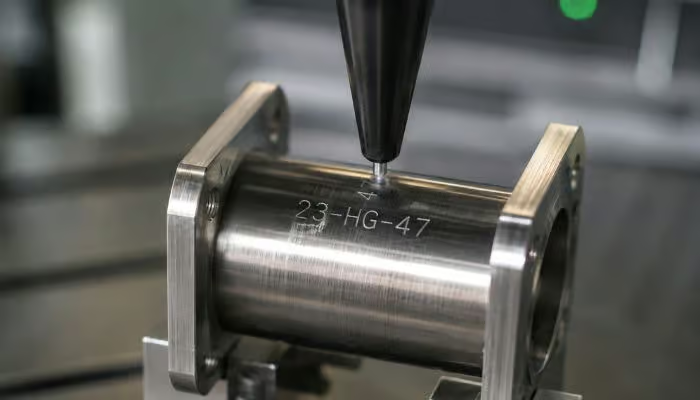
Step 1: Define Mark Performance Requirements
Begin by defining what the finished mark must accomplish. Determine whether operators only need to read it during production or whether the identification must remain legible throughout assembly, service, maintenance, and repeated handling. Then consider the expected exposure to abrasion, cleaning, heat, chemicals, or other conditions that could weaken the mark.
The reading requirement narrows the options further. Human-readable text mainly needs clear characters and sufficient contrast, while a Data Matrix code requires consistent cell definition for machine scanning. Set the required readability, service life, wear resistance, and level of permanence first, then select a part marking method capable of maintaining those characteristics.
Step 2: Consider Part Geometry and Marking Area
Next, identify the actual surface available for CNC part marking. Check whether the location is flat, curved, recessed, angled, or close to an edge, and confirm that the mark has enough usable area for the required text or code. Deep pockets, narrow shoulders, small diameters, and restricted surfaces can limit both equipment access and achievable mark size.
Then compare those geometric conditions with the physical requirements of each process. CNC engraving needs cutter and spindle clearance, dot peen marking needs direct stylus access, and laser marking needs an unobstructed optical path. Use the available surface shape, access, and marking space to eliminate methods that cannot reach the location or reproduce the required detail clearly.
Step 3: Evaluate Production Volume and Cost
Production volume should be evaluated by separating the one-time setup cost from the cost of marking each part. For prototypes and small batches, dedicated fixtures, screens, tooling preparation, or automated equipment can make setup costs disproportionately high. A simpler setup may therefore make more economic sense even if each individual mark takes slightly longer.
For larger runs, cycle time, operator handling, fixture loading, tooling or consumables, and automation have a greater effect on total marking cost. Automation becomes more valuable as repeat volume increases and the same marking cycle runs across more parts. Compare the total setup and processing cost across the expected order quantity rather than choosing a CNC part marking method based on its per-part marking speed alone.
Step 4: Consider Variable Data Requirements
First, separate the part marking content into fixed and changing information. Logos and warning symbols may stay fixed, while serial numbers, batch codes, dates, revision IDs, and Data Matrix codes can change by batch or by individual part.
Next, determine how often the information changes and where that data comes from. Fixed artwork suits processes such as screen printing, while frequently changing serial numbers or codes favor digitally controlled laser marking or dot peen marking. When the data changes regularly, choose a process that can update the marking content without creating a new physical setup for each change.
What Standards and Requirements Apply to CNC Part Marking?
CNC part marking standards can control the identification itself, the quality of a Data Matrix mark, or the way a finished direct part mark is verified. The applicable requirement normally comes from the drawing, contract, customer specification, or industry program, so the standard should be identified before the marking process is finalized.
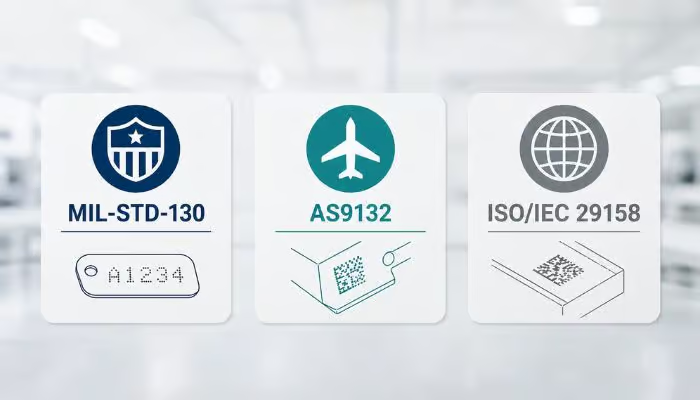
MIL-STD-130
MIL-STD-130 applies to the identification marking of U.S. military property. For CNC parts covered by the requirement, the drawing or contract can specify human-readable identification, machine-readable information, or both, including part identification and other required data.
The key requirement is that the selected part marking process produces the required identification without damaging the component or interfering with its function. This means the marking method, location, and permanence must suit the actual part rather than simply following a fixed marking process for every military component.
AS9132
AS9132 focuses specifically on Data Matrix marks applied directly to metallic aviation, space, and defense parts. It does not decide what information belongs inside the code; instead, it controls the quality of the physical Data Matrix produced by processes such as laser marking, dot peening, and electrochemical etching.
A CNC part subject to AS9132 needs a Data Matrix with sufficient symbol quality and a location that allows reliable electronic reading. A code that contains the correct data can still fail the requirement if poor dot formation, contrast, or placement prevents dependable scanning.
ISO/IEC 29158
ISO/IEC 29158 addresses the verification of machine-readable direct part marking (DPM). Direct marks on metal or other component surfaces can create glare, low contrast, or irregular cells, so normal printed-barcode inspection conditions do not always represent how the symbol actually behaves.
ISO/IEC 29158 defines how the finished DPM symbol is illuminated, captured, measured, and graded for readability. In practice, it provides a consistent way to determine whether a Data Matrix or other applicable direct mark meets the specified machine-readable quality level.
What Part Marking Details Should Be Specified on a CNC Drawing?
A CNC drawing should define the part marking details clearly enough that the supplier can reproduce the mark without interpreting missing information. The drawing should identify the exact content, marking zone, reading direction, character or code dimensions, required process, and any rules for changing serial or batch data.
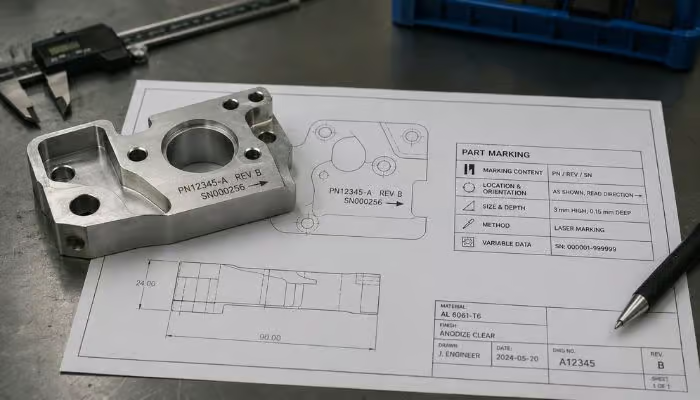
Marking Content
The drawing should show the exact information that must appear on the part. This can include a part number, serial number, revision, lot code, date code, logo, inspection symbol, warning text, or Data Matrix content. When punctuation, prefixes, suffixes, capitalization, or spacing matters, include the complete character string rather than a general note such as “mark P/N.”
For machine-readable identification, separate the encoded data from any human-readable text shown beside it. If the code contains a part number, serial number, and lot number, define the order and format of those fields so the part marking file does not rely on shop interpretation.
Location and Orientation
Marking location should tie to recognizable part geometry instead of a vague note such as “mark on side.” A drawing can dimension the mark from datums, edges, holes, or centerlines, or define a bounded marking zone on a specific face.
Orientation also needs to remove ambiguity. Show which edge or datum the text reads from and whether a Data Matrix or logo must face a particular assembly or viewing direction. Keep the part marking area away from threads, sealing faces, precision fits, bearing surfaces, and other functional features unless the design intentionally allows marking there.
Size and Depth
The drawing should control the dimensions that determine whether the mark remains readable. For text, this can include character height, stroke width, spacing, and overall marking envelope. For a Data Matrix, define the symbol size or cell size when the code must fit within a restricted area.
Depth only needs specification when the part marking process physically removes or displaces material. For CNC engraving, laser engraving, or dot peen marking, state the required depth, acceptable range, or maximum penetration when it affects readability or nearby geometry. Surface-level laser marks or printed marks usually need a visibility or contrast requirement instead of a depth value.
Marking Method
If the design depends on a particular surface condition, the drawing should name the required part marking method directly. A note such as “LASER MARK,” “CNC ENGRAVE,” or “DOT PEEN” prevents substitution with a process that creates the same characters but a different depth, texture, or permanence.
Not every project needs to lock the process. When the result matters more than the technology, specify the required readability, depth, permanence, or code quality and allow the supplier to use a suitable method. This avoids unnecessarily restricting production when several processes can meet the same marking requirement.
Variable Data Rules
Variable marking needs its own rules because the content changes during production. The drawing or linked specification should identify which fields vary by part or batch, such as serial numbers, lot numbers, dates, work-order references, or unique Data Matrix data.
For serial sequences, define the starting value, number of digits, prefix or suffix, increment rule, and whether the sequence resets between orders. For example, a requirement such as “SN0001–SN0500, increment by 1, no duplicates” gives the shop a usable part marking rule instead of simply stating “add serial number.”
Best Practices for CNC Part Marking
Good CNC part marking depends on more than choosing the right method. The shop also needs to confirm the marking setup before production, verify the finished mark against the requirement, and keep the process stable across repeat orders. These controls reduce wrong data, misplaced marks, unreadable codes, and visible variation between batches.
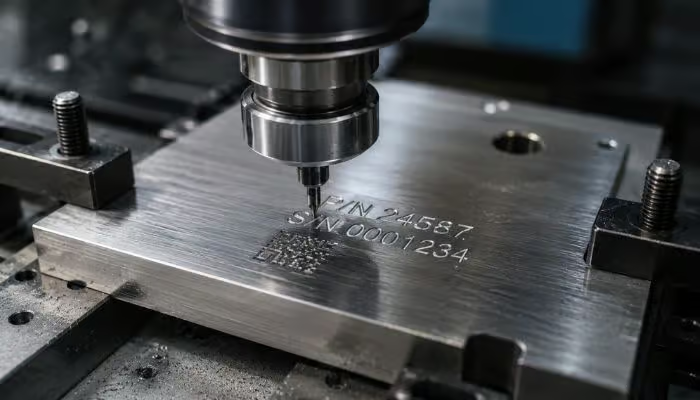
Verify Marking Setup Before Production
Before the production run starts, confirm that the marking program uses the approved text, code file, serial format, and part orientation. The fixture should place the part marking area in the correct position, while laser focus, engraving depth, stylus force, and print alignment should match the planned setup.
A first-piece mark provides a practical check before the remaining parts enter production. Compare the first mark with the drawing or approved reference for content, position, orientation, character formation, and required depth or contrast. Any mismatch should be corrected at the setup stage rather than carried through the entire batch.
Inspect Final Mark Quality and Accuracy
Final inspection should focus on the mark that actually reaches the customer, not only on whether the part marking equipment completed its cycle. Human-readable text needs complete characters and correct content, while machine-readable marks should remain clear enough for the intended scanner or verification method.
Inspect for missing strokes, incorrect characters, poor contrast, excessive depth, blurred edges, misplaced marks, and unreadable codes. When the drawing controls a measurable feature such as engraving depth, character height, or mark position, verify that requirement in the same way as other specified CNC part dimensions.
Maintain Consistency Across Production Batches
Repeat orders can drift when marking parameters, tooling, fixtures, or consumables change over time. A worn engraving cutter can widen strokes, a dot peen stylus can change indentation quality, and changes in laser focus or print setup can alter contrast and character definition.
Keep approved part marking parameters, fixture references, program versions, and representative samples with the production record so future batches can reproduce the same result. Periodic checks during longer runs also help identify gradual changes before they create noticeable variation across the finished CNC parts.
Conclusion
Part marking gives CNC-machined parts a practical way to carry identification throughout production, assembly, inspection, and service. The right result comes from matching the marking method to the part material, surface condition, geometry, required durability, and identification format, while also following any drawing or industry requirements that apply.
For custom CNC parts, define the marking content and requirements early so the process can be planned together with machining and finishing. DZ Making can produce CNC parts with drawing-specified part marking for prototypes and production orders. Send us your drawing, material, quantity, and marking requirements to request a quotation.
FAQs
1. Can part marking affect the strength of a CNC-machined part?
Yes, part marking can affect a CNC-machined part if the mark removes too much material, creates a deep notch, or sits too close to a thin wall, fillet, sealing surface, or highly loaded feature. Shallow laser marking or properly controlled engraving usually has little structural effect, but deeper CNC engraving or dot peen marking should stay within the limits defined by the part geometry and application.
2. Can part marking be removed or reworked?
Some CNC part marking can be reworked, but the options depend on how the mark was created. Printed ink may be removable, while shallow laser marks can sometimes be polished away; deeper laser engraving, CNC engraving, and dot peen marks usually require material removal to eliminate them. Rework should not reduce the part below dimensional or surface requirements.
3. How long does part marking last on CNC-machined parts?
The durability of part marking depends on the method, mark depth, surface finish, and service environment. Recessed engraving and dot peen marks usually resist handling and abrasion better than surface-applied ink, while contrast-based laser marking can remain readable for long periods if the surface is not heavily worn or refinished.
4. Can very small CNC parts still be marked clearly?
Yes, small CNC-machined parts can still receive clear part marking if the available area, character size, and marking method match the geometry. Laser marking is often useful for compact text or Data Matrix codes, while mechanical engraving may become limited when tool diameter, edge distance, or surface access leaves too little room for clean features.
5. What is the difference between human-readable and machine-readable part marking?
Human-readable part marking uses letters, numbers, or symbols that a person can interpret directly, while machine-readable marking uses codes such as Data Matrix symbols that a scanner or vision system reads electronically. CNC parts can carry either format or both when the drawing, traceability system, or applicable standard requires them.
6. Does part marking affect corrosion resistance?
It can. CNC part marking that removes or disrupts a protective surface can locally change corrosion behavior, especially on plated, anodized, or corrosion-resistant components. The effect depends on the marking depth, material, finish, and exposure conditions, so corrosion-sensitive parts should avoid unnecessary surface removal in critical areas.
